English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Italian
 Portuguese
Quick answer:
Precision casting parts are metal components produced through controlled molding where molten alloy fills a prepared cavity to achieve tight dimensional accuracy. The key to getting the right part is matching your tolerance specifications, material grade, and surface finish to a process that can reliably hold them. A mismatch here typically triggers expensive rework, failed inspections, or early fatigue failure in service. Before placing an order, confirm the foundry’s process capability data, alloy mill certificates, and the inspection method applied per batch.
Many buyers in CNC machining and assembly operations run into a familiar problem: a casting looks correct on the drawing but fails under load, or tolerances drift outside spec after heat treatment. YPMFG supports projects where dimensional and material requirements are strict, and the sections below walk through what to verify before you commit tooling or place a production order.
Contents
Key specifications that define the part
Matching alloy and process to your application
Tolerances, inspection, and post-casting machining
Common questions before ordering
Making a better long-term decision
Key Specifications That Define the Part
Four parameters govern whether a casting will perform in service:
Alloy grade and heat-treatment condition – sets strength, corrosion resistance, and fatigue life
Nominal dimensions and tolerance class – defines acceptable deviation per feature
Surface finish requirements (Ra value) – critical for mating surfaces, seals, and cosmetic faces
Critical-to-quality (CTQ) features – the handful of dimensions that must hold tighter than the general tolerance
If your drawing calls for ±0.1 mm on a 120 mm bore but ±0.5 mm on non-critical walls, state that explicitly. Ambiguity is the most common cause of disputes between buyer and foundry.
Matching Alloy and Process to Your Application
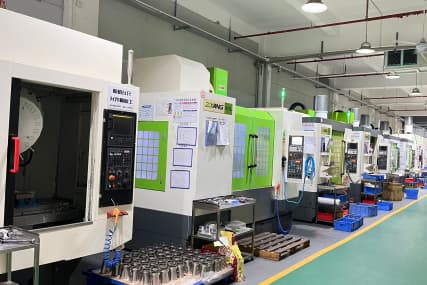
Not every geometry suits every casting method. The table below summarizes typical ranges so you can narrow the field quickly.
Choose investment casting when your part needs fine detail and tight tolerances without heavy secondary machining. Shell-mold sand casting works better for larger, lower-cost components where a few tenths of a millimeter of clearance are acceptable. YPMFG can help you compare process options against your drawing and budget before tooling is committed.
Tolerances, Inspection, and Post-Casting Machining
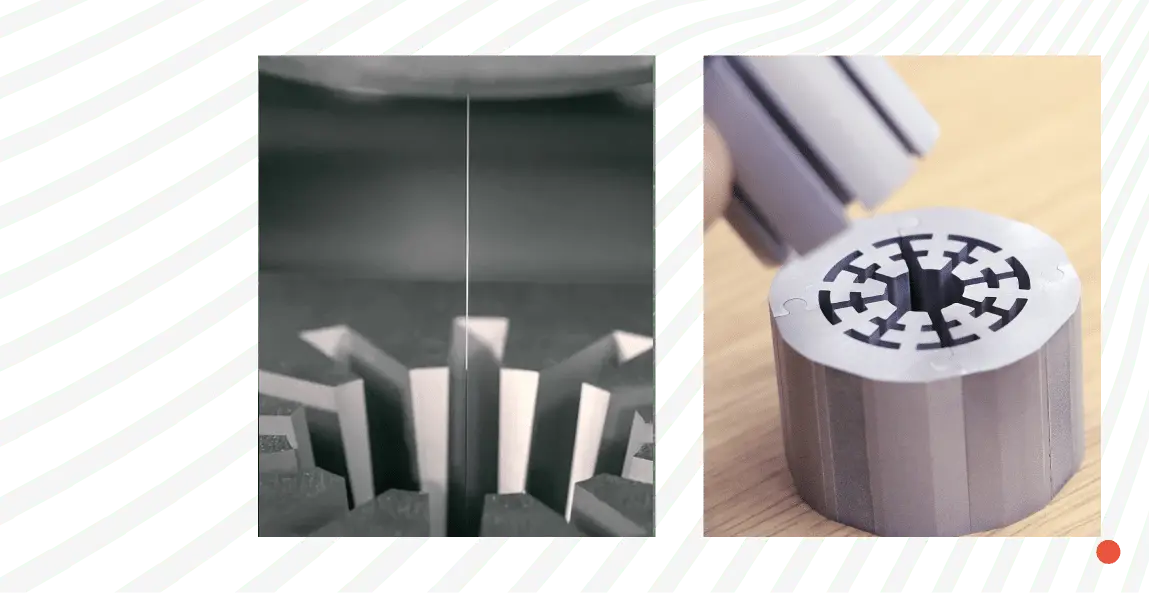
As-cast dimensions will rarely be your final dimensions for functional parts. Budget for post-casting machining—facing, boring, drilling, or thread tapping—to land CTQ features within spec. Confirm with your supplier which dimensions are held as-cast and which require secondary machining after the part cools.
Ask the supplier to document their inspection method: CMM, optical comparators, or laser scanning. For safety-critical or aerospace applications, request a first-article inspection report aligned with AS9102. For industrial applications, a calibrated coordinate report on CTQ dimensions is typically sufficient.
## Common Questions Before Ordering Precision Casting Parts
Do I need a wax pattern, or can I skip it?
For investment casting, a wax or replica pattern is standard. For prototype or small-batch runs, 3D-printed wax substitutes are now widely available. Confirm which method the foundry uses and whether the pattern geometry accounts for solidification shrinkage.
How does heat treatment shift my tolerances?
It can, and often noticeably. Stress-relief, normalizing, or quench-and-temper cycles may shift dimensions by 0.02–0.15 mm depending on alloy and part mass. Specify the final heat-treatment condition on the drawing so the foundry compensates in the pattern.
What lead time should I plan for?
Prototype or small-lot runs typically run 4–8 weeks including pattern, mold, casting, and machining. Production batches of 500+ units often compress to 3–6 weeks. Confirm whether the quote covers post-casting machining or only the as-cast piece.
How do I verify alloy composition on delivery?
Request mill test reports and, for high-value or safety-critical parts, a spot-spectroscopy or wet-chemistry analysis on the as-received lot. YPMFG supports buyers who need documentation packages aligned with supplier qualification requirements.
Making a Better Long-Term Decision
A well-specified casting saves money over its service life, not just at the point of purchase. Before finalizing your order,send your drawing, material spec, and CTQ list to YPMFG for an engineering review. The team can flag tolerance conflicts, suggest process changes that reduce scrap, and provide a detailed quote with inspection documentation included. Start with a sample batch to validate dimensional accuracy before committing to full production.