Spanish
 English
 German
 Russian
 Japanese
 Korean
 French
 Italian
 Portuguese

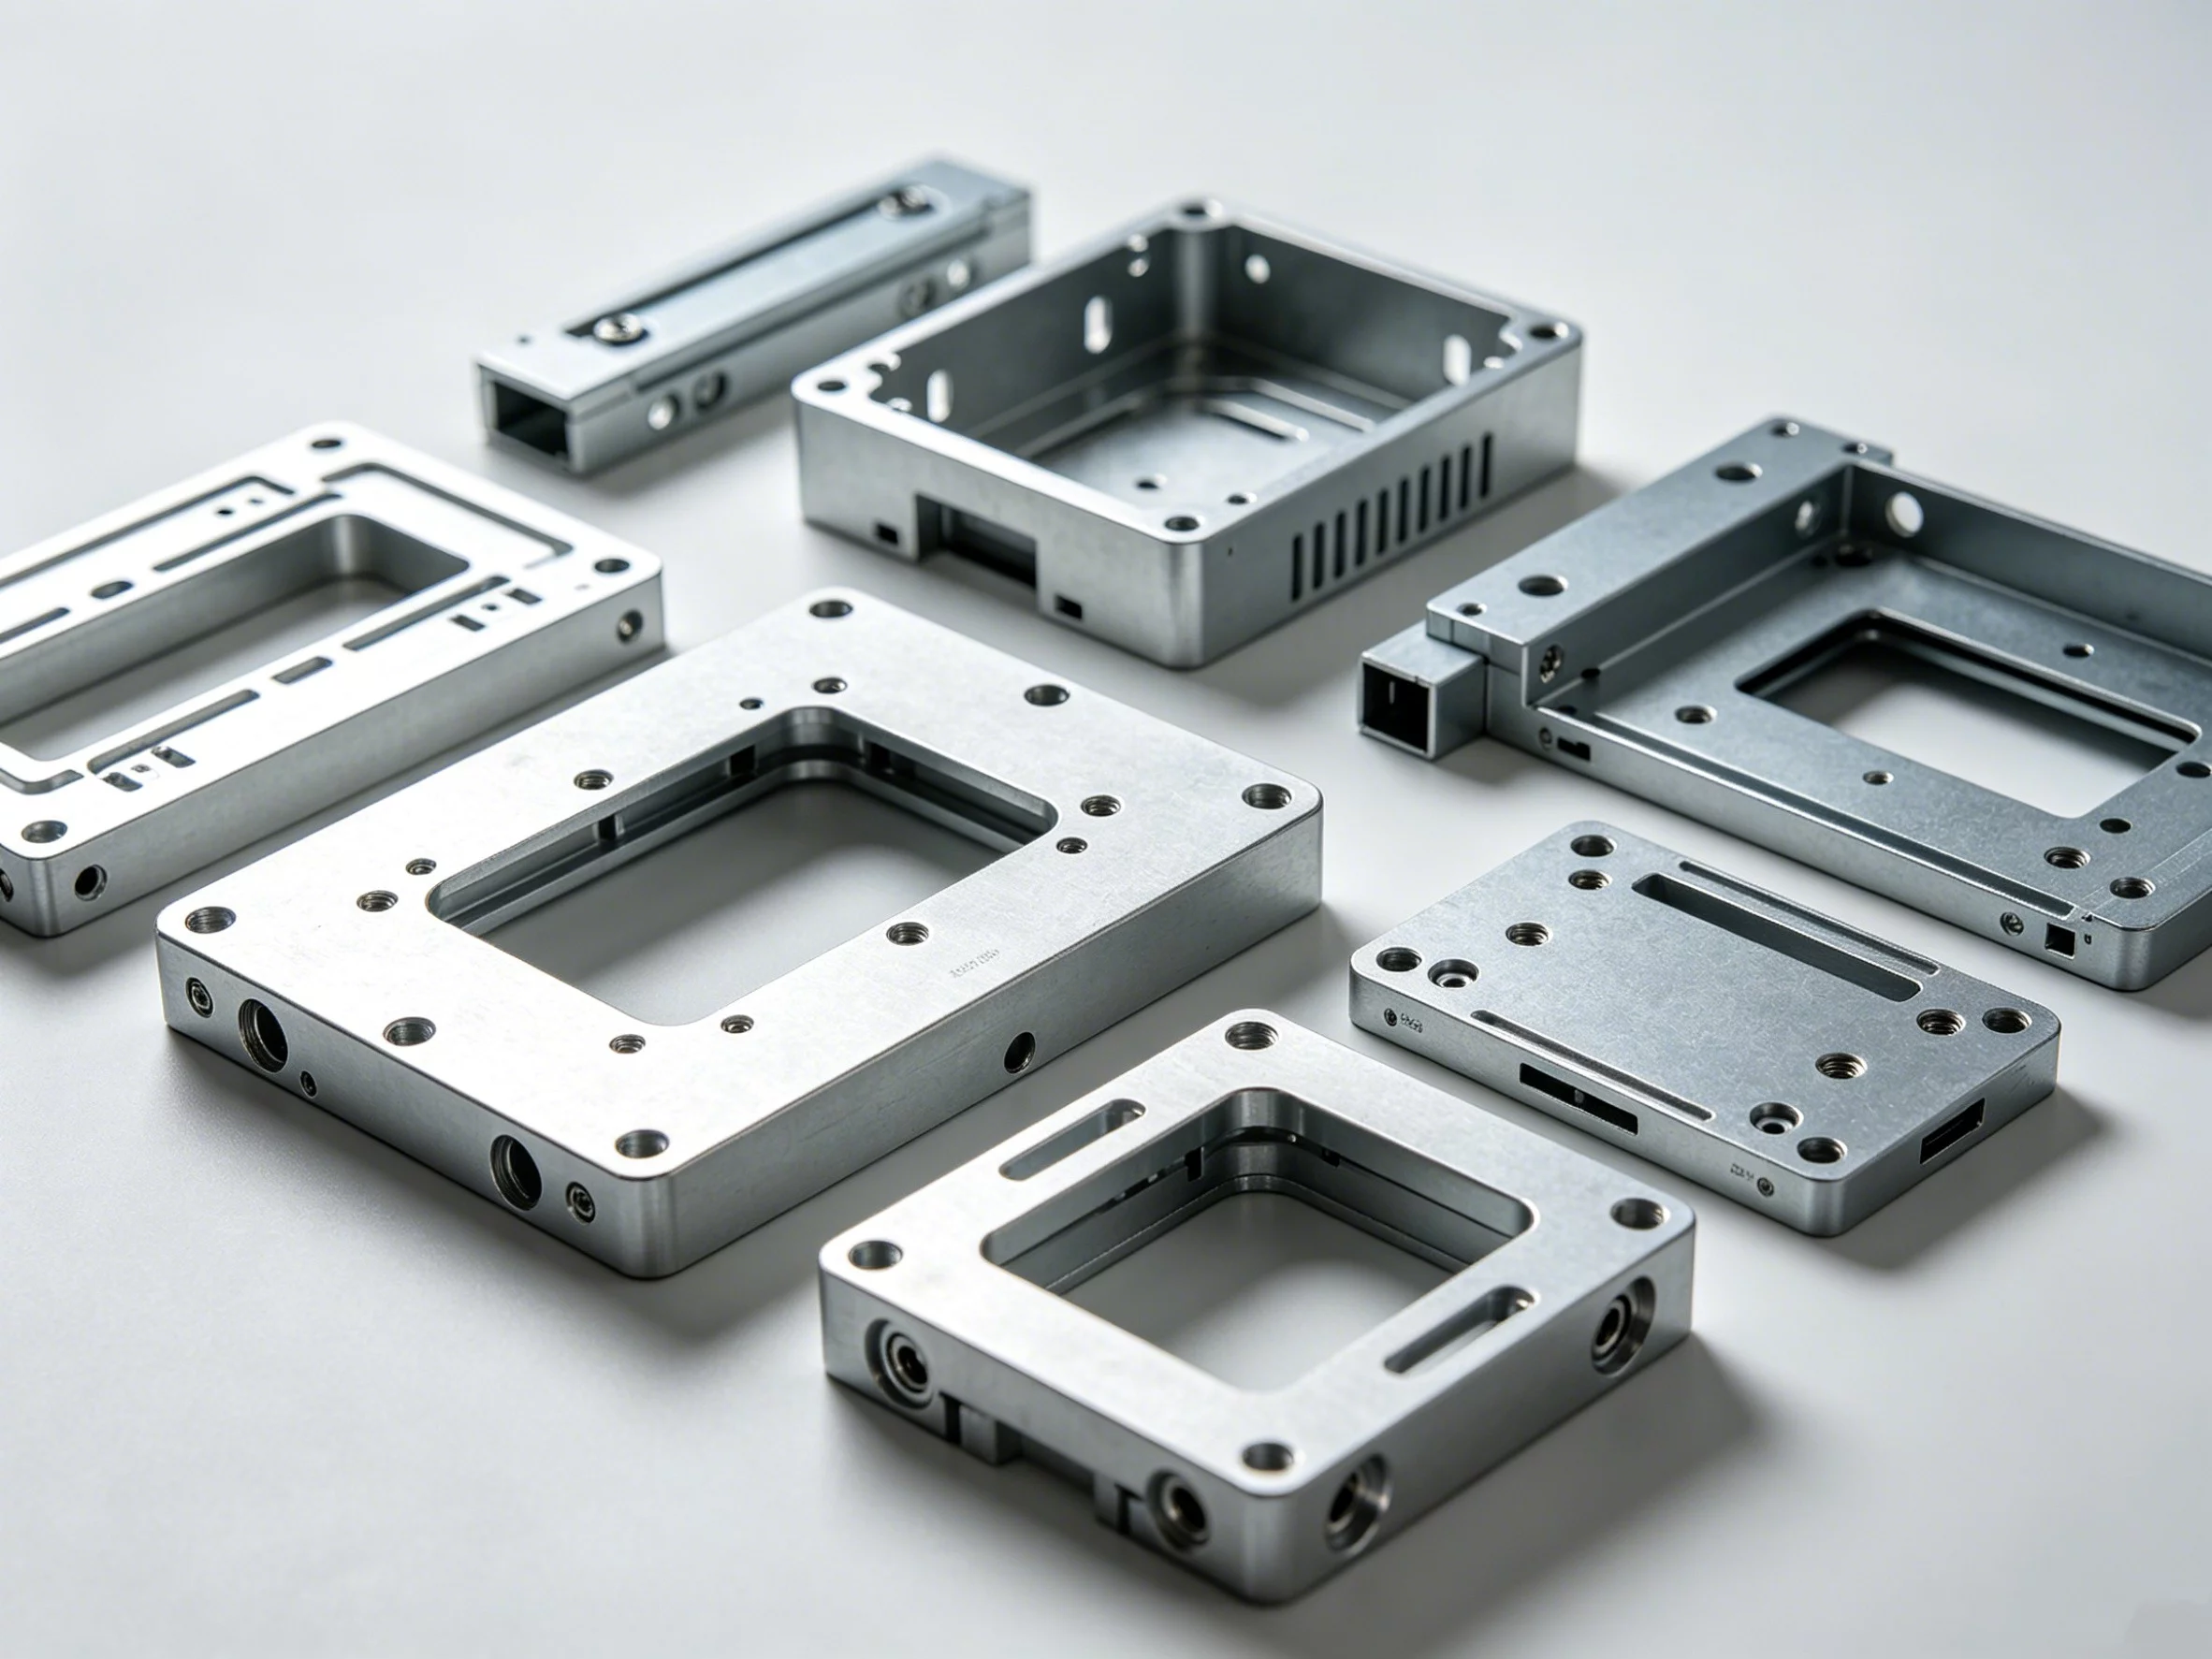
Personalizado stamping parts con red powder coating pair sheet-metal forming with a thermoset paint finish. The stamping press shapes raw metal into precise brackets, enclosures, or structural sub-assemblies. The powder coat then adds resistencia a la corrosión, uniform color, and a durable surface layer that outlasts most liquid finishes. Buyers should specify the base metal, part geometry, RAL shade, and target film thickness before the first press run. Getting those parameters aligned in advance prevents rework, color mismatch, and costly assembly delays downstream.
Most procurement teams define the part shape and material but leave the powder coat finish details vague. That gap is where color drift, peeling, and failed salt-spray tests start. Here is what to lock down before you release an order.
What Red Powder Coating Does for Stamped Parts
Red powder coating is a dry, electrostatic finishing process. A thermoset polymer powder is sprayed onto the stamped part, then cured in an oven at 180–210 °C. The result is a continuous, solvent-free film that resists chipping better than most liquid paints. For stamped components exposed to outdoor conditions, chemical washdowns, or frequent cosmetic inspection, this finish extends service life and cuts surface-maintenance cycles. The powder-coating process also handles complex geometries well because the powder wraps edges and recesses evenly, something liquid paint struggles to achieve on deep-draw features.
Datos técnicos clave que hay que confirmar antes de realizar el pedido
Before releasing a purchase order, confirm these parameters with your fabricator:
Base material and thickness (cold-rolled steel 1.5 mm, aluminum 5052-H32, stainless 304, or application-specific alloy)
Stamping tolerance on fit-critical features (typically ±0.1 mm; tighter for mating joints or press-fit interfaces)
Powder shade referenced by RAL or Pantone number, with a physical coupon attached for non-standard colors

Espesor de la película (60–120 µm for general use; 150 µm or more for high-abrasion or outdoor-exposed zones)
Surface texture (matte, gloss, or textured) and the cure temperature profile
Salt-spray, cross-hatch, or adhesion test requirement tied to your service environment
YPMFG reviews fabricación metálica drawings against this checklist and flags conflicts between stamping tolerance and coating build-up before the first press run, so you avoid a geometric clash after the part is finished.
## Quick Comparison: Finishing Options for Stamped Parts
For high-volume stamped brackets or enclosures, red powder coat typically offers the best balance of durability, color stability, and per-unit cost compared with liquid paint or anodizing.
Common Mistakes That Trigger Rejections
Three issues account for most supplier rework on red powder-coated stamped parts:
Unspecified shade. “Red” is not a spec. Without a numbered RAL or Pantone reference, batch-to-batch variation is unavoidable, and the final part may not match the sample.
Coating over sharp 90° edges. Powder builds up at corners, creating uneven film thickness and weak adhesion spots. Design with a minimum 3 mm fillet where the geometry allows.
Skipping surface prep. Stamping leaves cutting oils and burrs on the part. A proper degrease plus light abrasive blast (Sa 2.5 minimum) is mandatory before the powder goes on.
If your drawing does not call out prep method, coating thickness, and a pass/fail acceptance criterion, the supplier will default to house standards that may not match your quality bar.
Writing a Clear Drawing Note for Your Coating Shop
A short, structured note on the drawing eliminates most back-and-forth. Include the material grade, the exact RAL or Pantone number with a coupon reference,the minimum and maximum allowed film thickness, the surface texture, and the specific salt-spray or adhesion test you will run on receipt. State whether the coating covers all surfaces or only external faces. Add a note on prohibited zones, such as threaded bores or sensor windows. YPMFG engineers can pre-review this note against your stamping drawing so the fabrication and finishing teams work from one aligned document.
Preguntas prácticas antes de elegir un proveedor
Can I get a coated sample before full production?
Most metal-stamping shops will produce 3–5 coated samples from your approved geometry. Request a physical sample in the exact shade and verify adhesion with a cross-hatch pull test before committing to a full run.
¿Qué plazo de entrega debo esperar?
Stamping setup plus a 200–500-part run typically takes 2–3 weeks. Powder coating adds 3–5 business days. Custom color matching or a non-standard shade can add another week to the timeline.
How do I verify film thickness on incoming parts?
Use a magnetic or eddy-current gauge and spot-check at least five points per part. Readings should fall within the specified ±10 µm window. Log the results and attach them to the receiving report.
Will the coating affect dimensional tolerances?
A 100 µm film adds roughly 0.1 mm to each exposed face. If the part fits into a tight housing or mating assembly, call out the finished (coated) dimensions on the drawing rather than bare-metal dimensions.
What documentation should the supplier provide with each lot?
At minimum: material certification, stamping inspection report, coating thickness map, cure-temperature log, and a color reference coupon stored alongside the batch for future touch-up matching.
Tomar una mejor decisión a largo plazo
The lowest quoted price rarely reflects the true cost of color mismatch, early surface failure, or repeated rework cycles. Specifying the full chain—material, geometry, prep method, shade, film thickness, cure profile, and acceptance test—turns a risky guess into a repeatable manufacturing process. YPMFG can review your part drawings, suggest optimal fabricación metálica parameters, and coordinate the powder-coating step so you receive a finished component that fits and looks right the first time. Send your specifications or a sample drawing to start a quote and get an engineering review before you commit to volume.