
 Spanish
 English
 German
 Russian
 Japanese
 Korean
 French
 Italian
 Portuguese
Respuesta rápida:
When selecting stainless steel parts for a production run, three factors determine whether your components will perform on time and on budget: material grade, tolerance call-outs, and surface finish requirement. Grade 304 covers general corrosion service. Grade 316L is the standard for marine, chemical, and food-grade applications. Getting the grade wrong is the most expensive mistake a buyer can make. Confirm grade, certificate level, and dimensional tolerances before you request a quote.
Choosing the wrong alloy or skipping a tolerance specification on a critical bore can mean scrapping an entire batch. YPMFG works with buyers who need machined stainless components and helps them lock in the right parameters before metal is cut.
Stainless Steel Grades for Machined Parts
The grade you choose sets the ceiling for corrosion resistance, strength, and weldability. Most shops can machine any grade, but material cost and tooling life shift dramatically between them.
316L stainless steel is the default for chemical processing, pharmaceutical, and marine environments. It handles chloride exposure that would pit 304 within weeks.
For most Mecanizado CNC projects, 304 or 316L covers the need. Step up to duplex or 904L only when the service environment demands it.
Tolerances, Surface Finish, and DFM
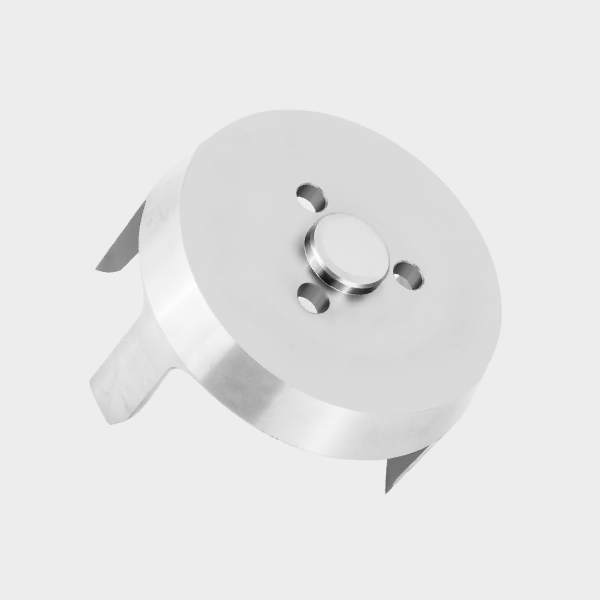
A acabado superficial call of Ra 0.8 µm on a 316L housing costs roughly twice what Ra 3.2 µm does, even with identical part geometry. The extra material removal and tool wear add up fast on stainless because the material is softer and gummier than carbon steel.
Before sending a drawing for quoting, check these items:
Are critical dimensions called out with individual tolerances, or is there a blanket ±0.1 mm?
Does the part need post-machining corrosion testing such as salt spray or immersion?
Is there a minimum wall thickness that keeps the CNC path rigid?
Are there threads that should be rolled instead of cut for better fatigue life?
Applying design for manufacturability early can shave 15–25 % off cycle time without changing part function.
Cost Factors That Actually Move the Price
Machining cost on stainless is driven less by part size and more by three variables:
Material grade selection – 316L bar or sheet costs 30–60 % more than 304; duplex is 100 % or more higher.

Tolerance and finish – A ±0.01 mm bore with Ra 0.4 µm finish nearly triples machining time versus ±0.1 mm and Ra 3.2 µm.
Geometry complexity – Internal undercuts, thin webs, or multi-axis features add setup time and dedicated tooling.
If you are comparing quotes from multiple shops,make sure each quote reflects the same grade, certificate level, and inspection method. Apples-to-apples pricing is the only fair basis for a decision.
YPMFG’s engineering team can review your drawing against these cost drivers before you commit to a production quantity.
## Practical Questions Before Ordering Stainless Steel Parts
Which grade should I use for a food-contact component?
Grade 304 or 316L, depending on whether the part sits in a high-chloride or acidic environment. 316L is the safer default for pharma lines and marine-adjacent food processing. Always request an EN 10204 3.1 material test certificate with each shipment.
Does stainless really need no secondary treatment?
It does not need plating for corrosion resistance in most environments, but machined surfaces often benefit from a light passivation or deburr step. For cosmetic parts, a final polish or bead blast changes the appearance entirely. Confirm the finish specification on the drawing.
What lead-time difference should I expect between 304 and 316L?
Machining time is nearly identical. The gap is in raw-material procurement: 316L bar and sheet typically carry one to two extra weeks compared with 304, especially in smaller diameters or thicker plate.
Can I get prototypes before committing to a full run?
Yes. YPMFG supports prototype or short-run batches of 5–50 pieces so you can validate fit, function, and surface quality before scaling to production volumes.
How do I verify corrosion performance after delivery?
Request a salt-spray test per ASTM B117 on a sample from the batch, or specify the required immersion test directly on the drawing. Agree the test duration and failure criteria in writing before production starts.
Tomar una mejor decisión a largo plazo
The right call on custom CNC parts in stainless is made before the first tool touches the material. Lock in grade, tolerance, finish, and inspection method. Once those are set, pricing, lead time, and performance become predictable instead of a gamble.
You can send your drawing or 3D file to YPMFG for an engineering review. The team will flag DFM issues, confirm the material specification, and return a line-item quote. That single review step is usually enough to avoid the most expensive mistakes downstream.




