Russian
 English
 German
 Japanese
 Korean
 Spanish
 French
 Italian
 Portuguese
Краткий ответ:
Laser cutting in metal fabrication uses a focused beam to melt, burn, or blow away material along a programmed path. It handles sheet and plate metal from roughly 0.5 mm up to 25 mm or more, depending on the machine and alloy. The process delivers laser cutting for metal fabrication that holds tight tolerances, minimizes secondary machining, and reduces scrap versus mechanical shearing.
Most buyers care about three things: part geometry, material thickness, and edge finish. Getting all three right determines whether laser cutting is the economical route or whether CNC metal fabrication via milling or turning makes more sense for your batch.
You need parts cut to a specific profile in steel, aluminum, or another alloy, and you are not sure whether laser cutting will actually save time and money or just add a new variable to manage. The cost, tolerance window, and material limits vary more than most buyers expect. What follows is a practical breakdown of what to check before you send a file to a shop.
How Laser Cutting Works in Metal Fabrication
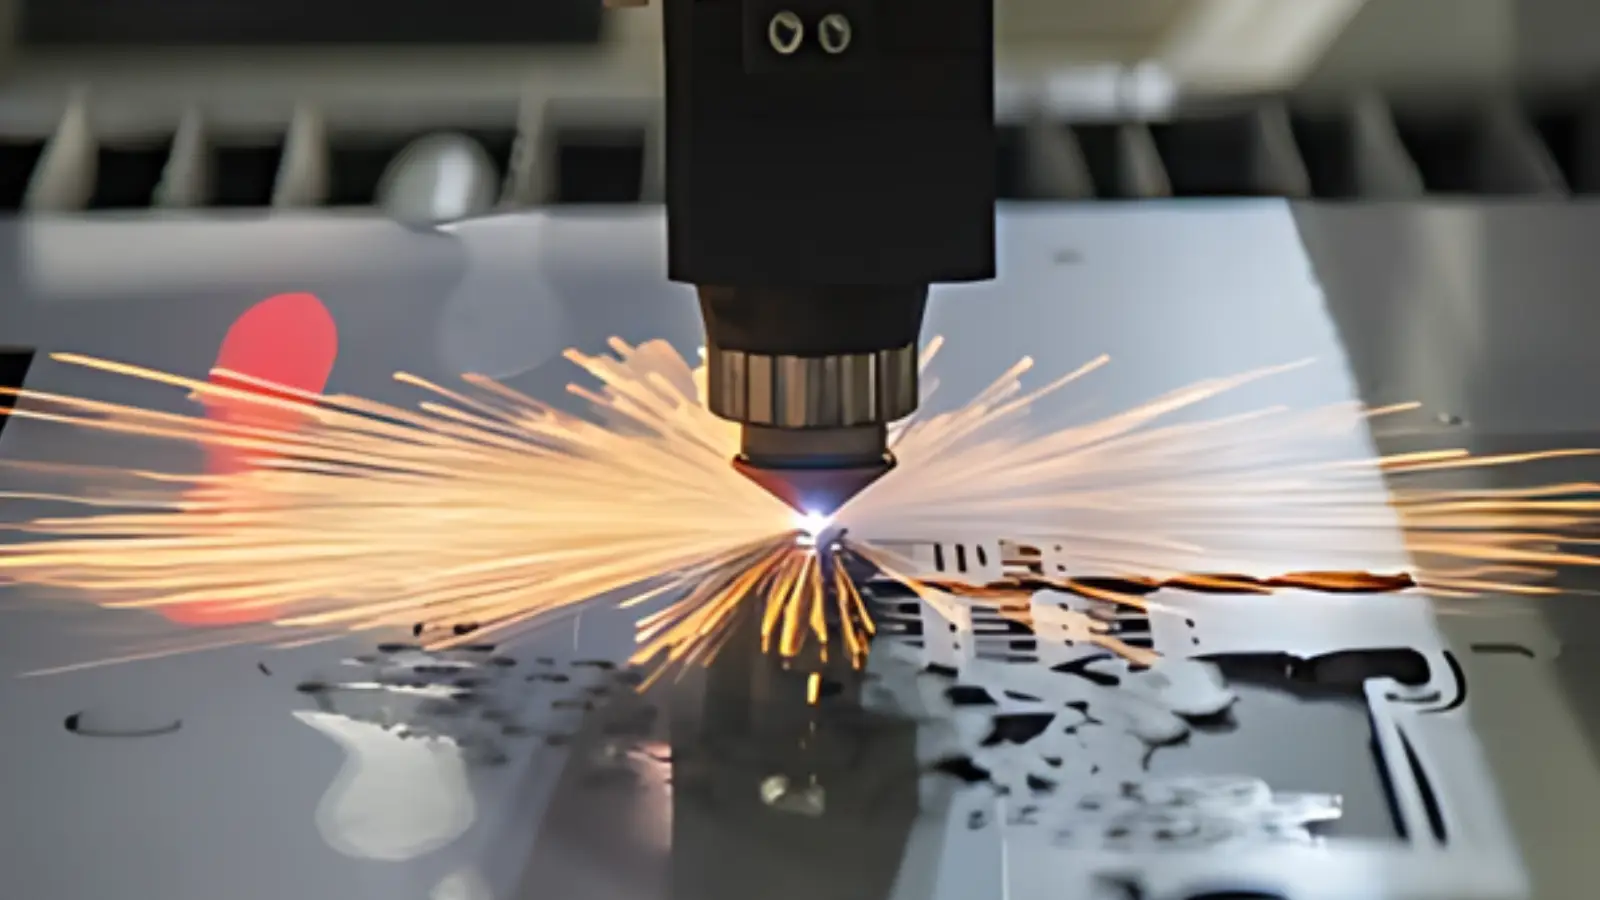
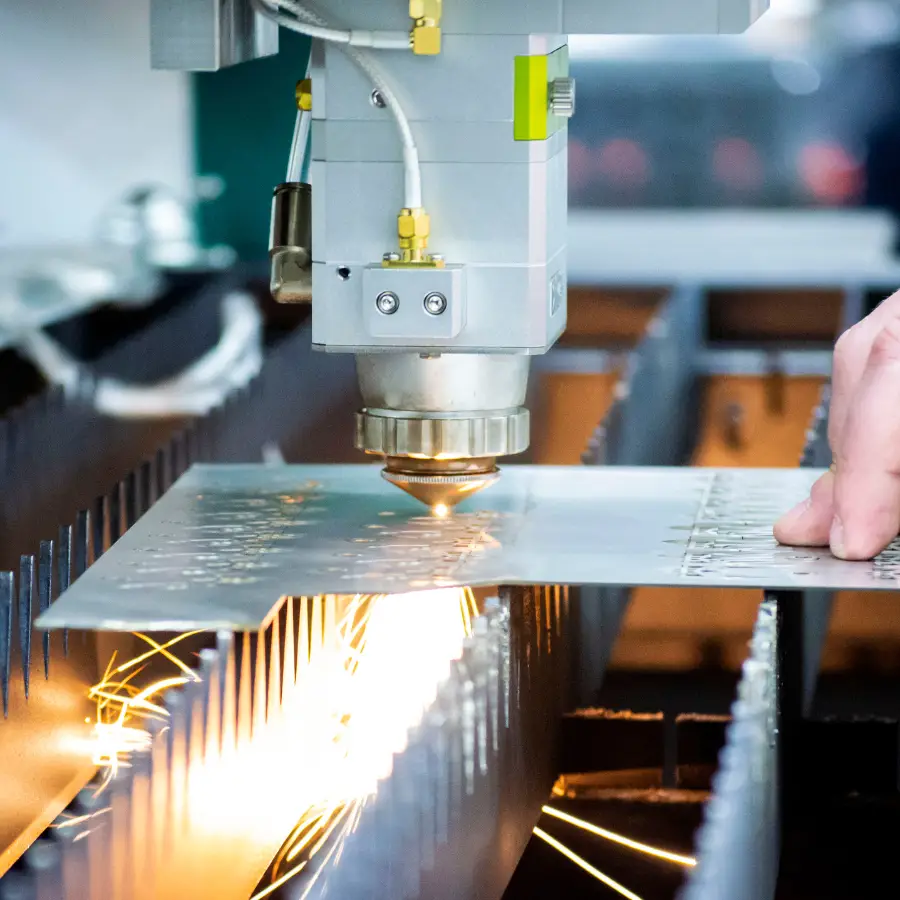
A fiber or CO₂ laser fires a concentrated beam through the workpiece. The beam either vaporizes the metal or, for oxygen-assisted cuts on mild steel, creates an oxidized melt that the assist gas blows away. The gantry moves the head along X, Y, and sometimes Z axes to follow the CAD path.
The key parameters are power (watts), material thickness, cut speed, and gas type. Nitrogen is standard for stainless and aluminum to prevent oxidation. Oxygen-assist is common and lower-cost for mild steel. The resulting kerf width usually falls between 0.1 and 0.5 mm, which directly affects the laser cutting tolerances you can hold on fine features.
Большинство sheet metal laser cutting runs on flat stock from 1 to 12 mm. Thicker plate work shifts toward high-wattage лазерная резка с использованием волоконного лазера. Understanding which regime your part falls into helps you pick the right machine and avoid paying for power you do not need.
Choosing the Right Laser Setup for Your Parts
Before sending a file, check four factors: material, thickness, part geometry, and post-finish requirements. The table below summarizes what to verify.
If your part has thin walls under 1 mm or very tight micro-features, ask whether the machine resolution and gas pressure can hold those specs. For larger structural members, confirm the beam spot size at your maximum thickness.
YPMFG can review your part drawings and material specs before you commit to a cut. Sending the CAD or PDF file along with the alloy and finish notes lets the engineering team flag nesting issues or tolerance conflicts early.
Факторы, влияющие на стоимость, и скрытые риски
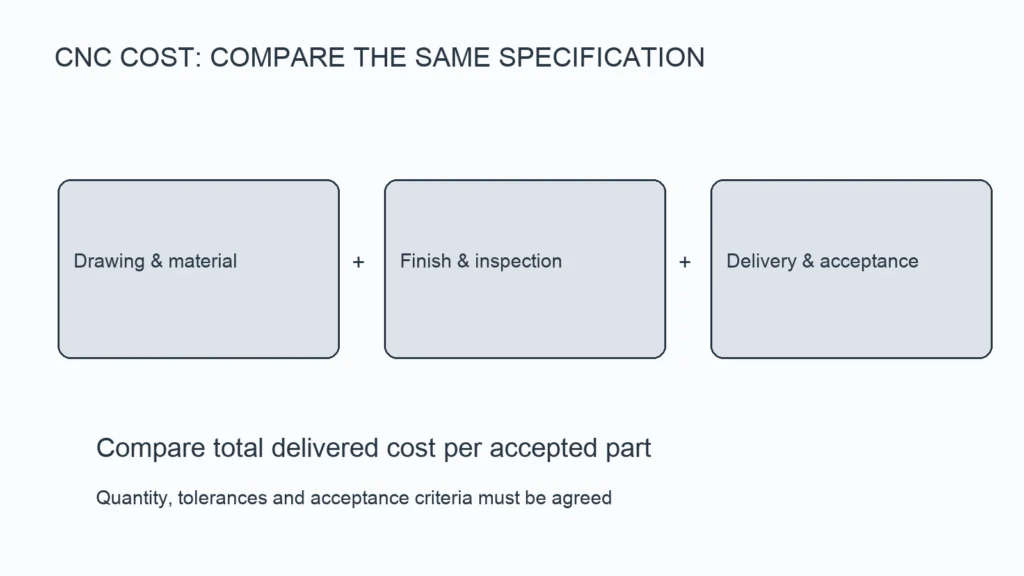
The quoted price for custom laser cut parts is not just watts multiplied by time. Five variables move the number: material grade, sheet thickness, part complexity, assist gas, and post-processing. A part with many small internal slots takes longer per sheet than a simple rectangle.
Hidden risks to watch before you approve a batch:
Thermal distortion on sheet under 1 mm can warp the part outside tolerance.
Stainless edges oxidize unless nitrogen covers the full cut height.
Mixed-material assemblies cut on the same sheet may require separate runs and higher cost.
Ask the supplier to confirm gas type, nesting efficiency, and whether laser cutting material compatibility for your specific alloy grade is proven on their machine. YPMFG supports buyers who need documented gas and speed settings for audit or qualification purposes.
Common Questions About Metal Laser Cutting
What is the thickest metal a laser can cut?
It depends on power and alloy. A 6 kW fiber unit handles mild steel up to roughly 25 mm. Aluminum and stainless need proportionally more power. Always confirm the exact thickness with the machine operator before committing to a quote.
Can laser cutting replace all mechanical shearing?
Not quite. For very thick plate or high-volume straight cuts, plasma or waterjet may cost less per part. Laser shines on complex 2-D profiles, mixed-material sheets, and услуги по изготовлению металлоконструкций that need tight tolerance without a secondary operation.
Do I need to deburr after laser cutting?
Mild steel edges usually carry a light burr; stainless and aluminum need more. Specify whether your part goes to weld, powder coat, or final assembly, and the shop should recommend the right post-process step.
How accurate is laser cutting for tight-tolerance parts?
Expect ±0.1 mm on well-maintained machines with proper nesting. For features under 0.5 mm, verify the minimum kerf at your material thickness before approving the drawing.
Принятие более взвешенного долгосрочного решения
Laser cutting becomes the right choice when part geometry is complex, material variety is high, and you need consistent tolerances without a secondary machining step. Before you sign off on a batch, send your specifications to YPMFG for an engineering review. The team can confirm material compatibility, suggest nesting layouts that lower per-part cost, and return a quote with clear tolerance and finish notes so there are no surprises on the shop floor.