Korean
 English
 German
 Russian
 Japanese
 Spanish
 French
 Italian
 Portuguese
간단한 답변:
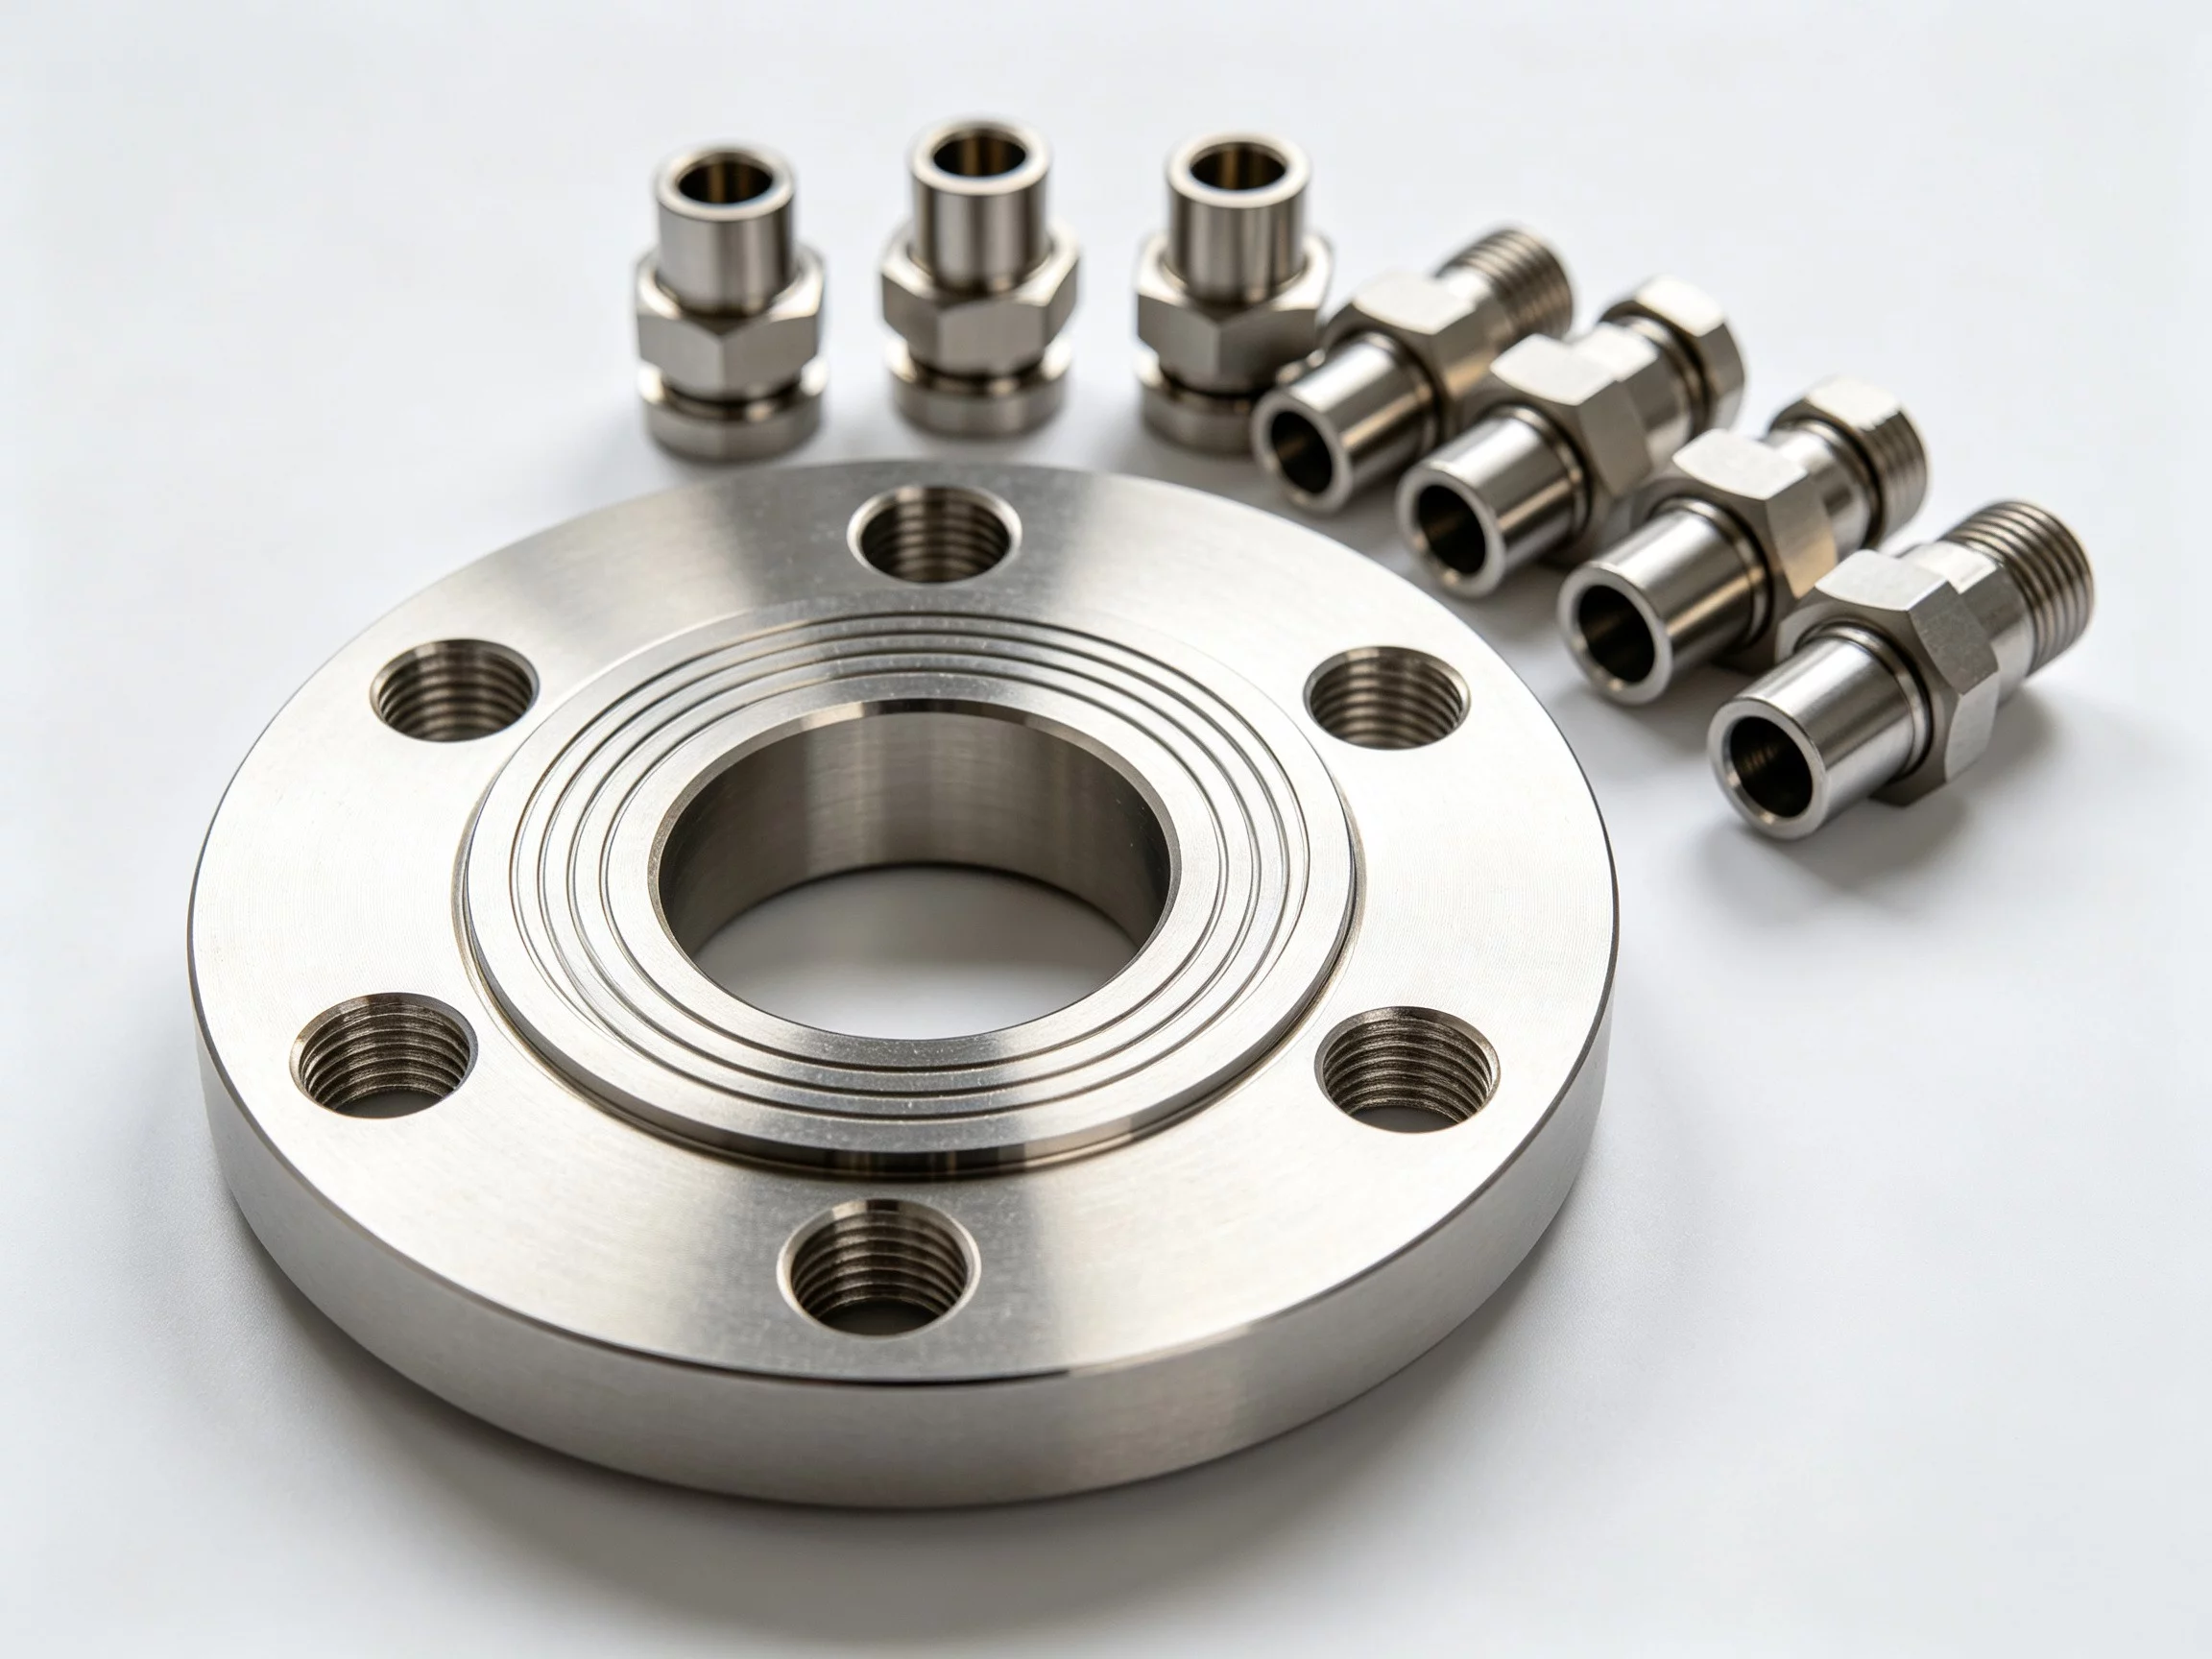
A cutter bar CNC turning lathe tool holder secures a straight or profiled cutting bar on a CNC lathe turret or tool post. It holds the bar at a fixed angle so the cutting edge stays in consistent contact with the workpiece on every pass. The right holder depends on bar cross-section size, turret bore diameter, clamping method, and whether the operation is rough turning operations or finishing. Mismatched specs lead to vibration, accelerated edge wear, and parts that miss dimensional tolerance on the first cut off the machine.
Most turning shops lose hours and scrap material when the holder does not actually match the bar geometry or the turret layout. The problem stays invisible until the surface finish shifts or the chip pattern changes mid-run. The points below cover the specs that decide whether a cutter bar tool holder will perform in your cell or quietly degrade part quality over a shift.
In this guide: What a holder does, the five specs to verify, three common fit failures, and questions to resolve before you place an order.
What the Holder Actually Does on the Lathe
A cutter bar holder locks the bar in a rigid, repeatable position so the cutting edge follows the programmed path exactly. Unlike an insert holder that clamps a small carbide chip, it grips the full length of the bar with a wedge, screw, or hydraulic clamp. That longer engaged length gives better stability at higher feeds and lets the operator run the bar deeper into the cut without micro-vibration.
Because each holder body is machined for one bar cross-section, a typical CNC turning lathe tool set needs a separate holder per bar size. Swapping between sizes means a different clamping jaw or a completely new holder body, which is the first thing to confirm when planning a tooling kit.
Five Specs to Verify Before Ordering
Turret bore diameter and the ISO standard it follows
Bar cross-section: square, round, or profiled
Clamping method: wedge, drawbar screw, or hydraulic
Overhang distance from the turret mounting face
Turret or tool-post interface: bolt-on, clamp-on, or integrated
If your turret uses a non-standard bore or a proprietary lock ring, a catalog ISO holder will not seat flush. YPMFG can review your turret drawing, confirm which holder series fits the existing bore, and flag any machining needed before the holder reaches the machine.
Three Fit Problems Behind Most Returns
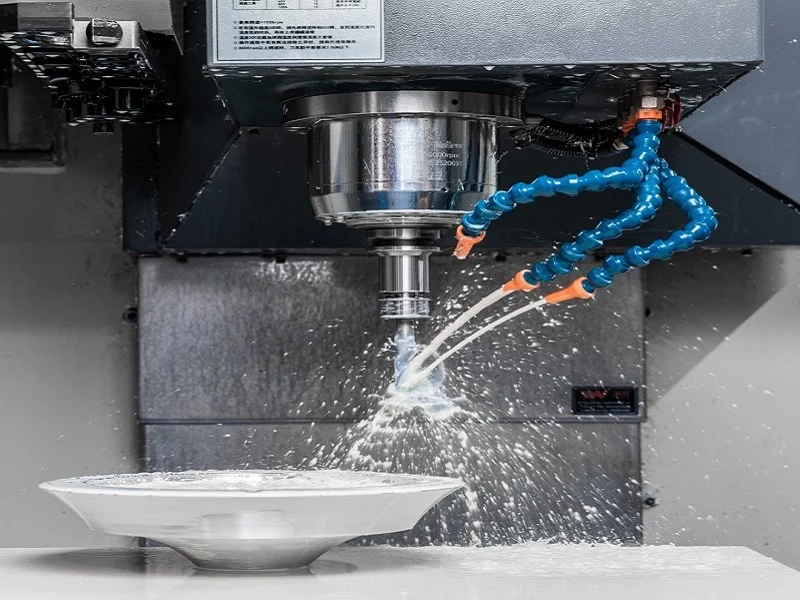
Bar tilt error. When the holder body is not parallel to the turret face,the cutting angle drifts by half a degree or more. The result is uneven cut width and a chip stream that shifts pass to pass. Check the mounting-surface flatness with a dial indicator before bolting the holder in.
Low clamping force. A bar that can micro-vibrate at spindle speeds above 2 000 rpm will blunt the edge within the first few parts. Verify the clamp bolt torque or hydraulic pressure against the holder’s rated maximum, and re-torque after the first ten minutes of cutting.
Excessive overhang. A holder that places the bar far from the turret face multiplies leverage on the turret bearings. Keep the tool overhang inside the range the machine manual states. If your operation requires a longer reach, consider a shorter bar with a holder designed for that cross-section instead of extending the overhang.
When these three issues stack, the shop blames the machine for missing tolerance. The root cause is almost always the holder-to-bar fit, not the spindle or controller.
Questions Buyers Ask Before Placing an Order
Can one holder take several bar sizes?
Usually no. Each holder body is machined for a single cross-section. Some modular systems swap clamp jaws, but the base and bore stay fixed. Confirm the jaw part number and the clamp interface before ordering extras.
How do I confirm my turret accepts ISO holders?
Measure the bore diameter and the distance from the bore face to the lock ring. Cross-reference those numbers against ISO 4417 or 4418. If your turret is proprietary, send the bore drawing to YPMFG for a fit check before ordering.
Which clamping method gives the best repeatability?
Hydraulic clamps lock fastest and hold the tightest position on repeated setups. Wedge and screw clamps cost less and work well for low-volume cells where you swap bars only a few times a shift. Match the method to your setup frequency.
Does the holder material affect chip evacuation?
In most cases, no. The holder body sits outside the chip path. What matters is the clearance between the bar and the holder seat. Too tight and chips pack behind the edge; too loose and the bar shifts under cutting force.
Making the Holding Decision Stick
A tooling layout that pairs each bar with a holder matched to its bore, clamping method, and overhang will hold edge life and part tolerance far better than a “close-enough” generic part. Send your current bar dimensions, turret spec, and a photo of the existing holder to YPMFG for a short engineering review. The team can confirm compatibility, flag overhang or tilt risks, and suggest a clamp style that fits your setup cycle. If you already run the bar and just need a replacement, that photo plus the bore measurement is usually enough to get an accurate quote back within a business day.