
 Portuguese
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Italian
Resposta rápida:
Keyboard machining typically involves CNC milling, turning, and drilling of housings, plates, keycaps, and structural components for mechanical and custom keyboards. Most production runs use 6061 or 7075 aluminum, though brass and titanium appear in premium builds. Tolerances usually fall between ±0.05 mm for general features and ±0.01 mm for mating surfaces. The process choice,material grade, and surface finish directly affect fit, feel, and unit cost. Buyers should verify drawings, material certifications, and post-machining treatment before committing to a supplier.
Se você estiver especificando machined keycap components or custom keyboard enclosures, the decision tree is shorter than it looks. A few variables drive nearly all cost and quality outcomes on the shop floor. YPMFG works with keyboard and peripheral brands on this kind of component work, and the patterns below reflect what separates a clean first-pass build from a rework loop.
What Goes Into Keyboard Machining
The three most common machined keyboard parts are aluminum keyboard plates, housings, and switch-plate cutouts. Each calls for a different balance of milling depth, tooling, and finishing.
A direita machining process selection depends on part geometry. Deep-hollowed housings benefit from 5-axis milling to avoid setup errors between opposing faces. Flat switch plates run faster and cheaper on 3-axis machines.
If your design includes tight internal threads, confirm whether the supplier taps the holes in-place or uses insert hardware. That decision affects both cycle time and the functional life of the thread. For high-volume runs, ask about fixture design. A well-designed vacuum or clamp fixture keeps repeat dimensions tight across lots.
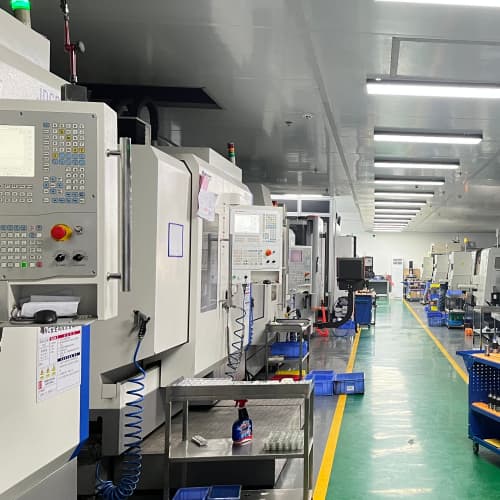
YPMFG can review your STEP or IGES files and flag process issues before any cutting begins.
Tolerances and Surface Finish That Matter
Fit and feel on a keyboard are tolerance-driven. A housing that is 0.05 mm off will show a visible gap at the seam. Especificações de tolerância for mating surfaces should be called out per feature, not as a blanket value across the drawing.
Surface finish follows function. Requisitos de acabamento superficial for touch-facing surfaces often land at Ra 0.8–1.6 µm. Internal switch-routing surfaces can relax to Ra 3.2 µm unless the design calls otherwise.
Anodizing adds another layer of complexity. Thickness and color consistency must be confirmed before the part reaches the finish line. Check whether the supplier treats anodizing in-house or outsources it, because dimensional growth of 10–25 µm per side must be subtracted from the raw machined size.
Common Ordering Mistakes
Três erros aparecem repetidamente em keyboard component sourcing:
Ordering without a finished STEP or IGES file. Relying on 2D PDFs invites interpretation errors on hole patterns and chamfer radii.
Skipping a material certification. A mill test certificate or PMI report protects you when alloy-specific strength or corrosion resistance is part of the spec.
Assuming anodizing color and tolerance are independent. A thick anodize layer adds dimensional growth that must be subtracted from the raw part size before machining.
If any of these gaps exist in your current order, pause and re-check the drawing package before releasing it to the floor.
Questões práticas antes de fazer seu pedido
Which alloy should I use for a keyboard housing?
For most consumer and prosumer builds, 6061-T6 offers the best cost-to-strength balance. 7075-T6 reduces weight further but raises machining difficulty and cost. Titanium suits low-volume premium runs. Confirm your finish vendor supports the alloy before locking the material.
How tight can tolerances realistically go on a machined switch plate?
±0.02 mm is achievable on a stable 3-axis setup with proper fixturing. Below ±0.01 mm, expect longer cycle times and a higher scrap rate. Define at each callout whether the tolerance is critical or general so the shop can quote accordingly.
Do I need a prototype run before full production?
Yes, if this is your first geometry. A single CNC milled keyboard housing prototype catches fit, finish, and assembly issues that drawings alone will not surface. Budget roughly one week for machining plus finishing, depending on part size and anodize type.
What documentation should I expect from my machinist?
At minimum: as-built dimensions on critical features, material traceability, and a surface finish report. For anodized parts, add a color match reference or Pantone code with a physical chip attached to the packing list.
Can I mix materials in one keyboard assembly?
Yes. Many designs pair an aluminum housing with brass or titanium accent plates. Confirm that thermal expansion differences will not cause binding over the operating temperature range. Your machinist can model the worst-case gap at maximum temperature.
Need Help Specifying Your Keyboard Parts?
The variables that drive a custom keyboard enclosure project are finite: material, process, tolerance, and finish. Get those four right on paper and the production run follows a predictable path.
YPMFG supports keyboard and peripheral teams from Torneamento e fresagem CNC through post-machining treatments. You can send your CAD files, BOM, or even a rough sketch for an engineering review. The team will flag feasibility issues, suggest tolerance adjustments where cost savings are available, and return a quoted lead time before you commit to a tooling schedule.
If you already have a working part and want to compare specs or explore a lighter alloy, send the part number and drawings. A short evaluation typically takes one to two business days.






