English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Italian
 Portuguese
Quick answer:
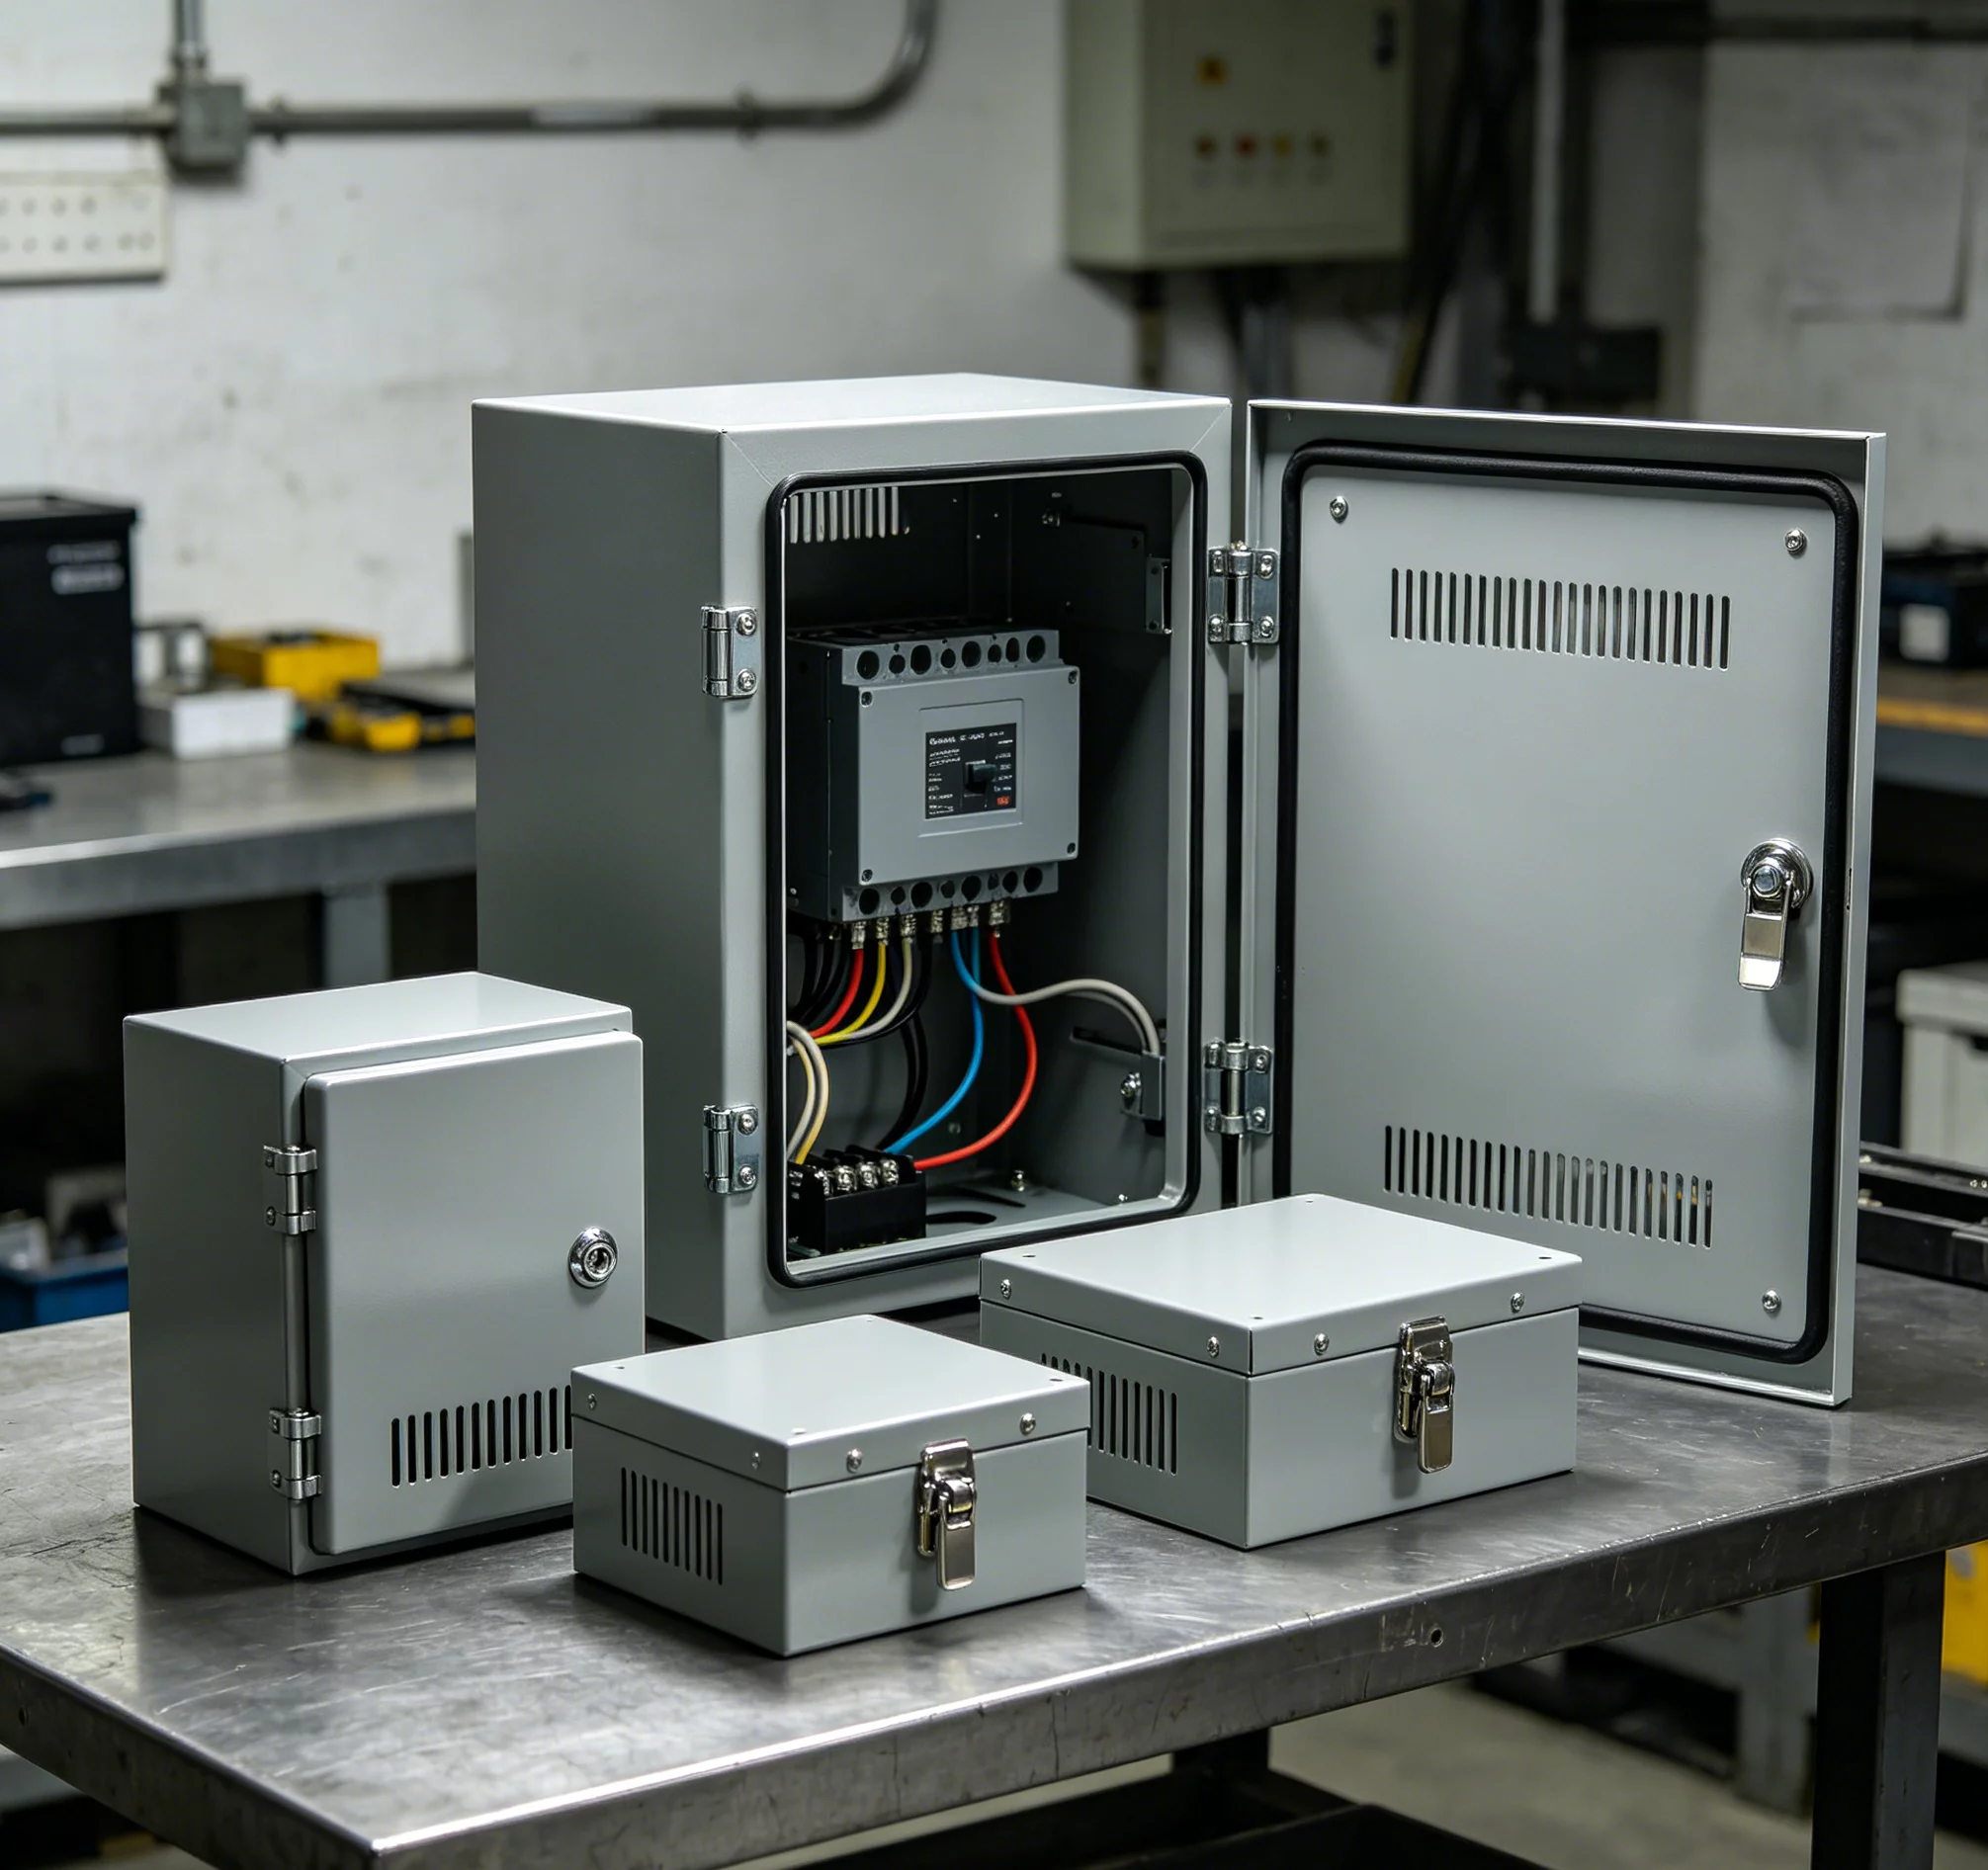
Sheet metal stamping presses a flat metal sheet between a die and a punch to produce cuts, bends, or shaped parts in seconds. It excels at high-volume production where consistent stamping die accuracy matters. The process suits parts with defined bends, holes, and flanges but struggles with complex 3D geometry or very low quantities. If your project needs one-off prototypes or intricate internal features, CNC machining or sheet metal fabrication may fit better. Confirm tooling lead time and minimum order quantity before finalizing any design.
Many buyers receive stamped-part quotes that vary by 40 percent between suppliers and cannot explain the gap. Material grade,die complexity, and run length all shift the final number. YPMFG’s engineering team reviews part drawings against these variables so you can compare offers on a clear basis.
How sheet metal stamping works
What drives unit cost
Stamping versus other processes
Mistakes that inflate rework
Buyer questions

How Sheet Metal Stamping Works
A flat blank feeds into a press tool. The punch and die work together to shear, bend, or form the metal in one stroke. Progressive die stations allow multiple operations to happen as the strip advances, cutting cycle time sharply.
The press force, blank size, and material hardness set the upper limit on part complexity. Thicker gauge or harder alloys require higher-tonnage presses, which increases tooling and setup costs.
What Drives Unit Cost
Three factors account for most of the price spread buyers see. The table below maps them to practical decisions.
After the tooling is amortized, per-part cost drops toward material and labor only. A short paragraph of context: YPMFG can model your projected volume against tooling amortization so you know the break-even point before committing to a die build.
Stamping versus Other Processes
Sheet metal fabrication (laser cut + welding) works for low-to-mid volumes and parts with mixed geometries. Stamping wins at 10,000+ units where cycle speed and repeatability matter.
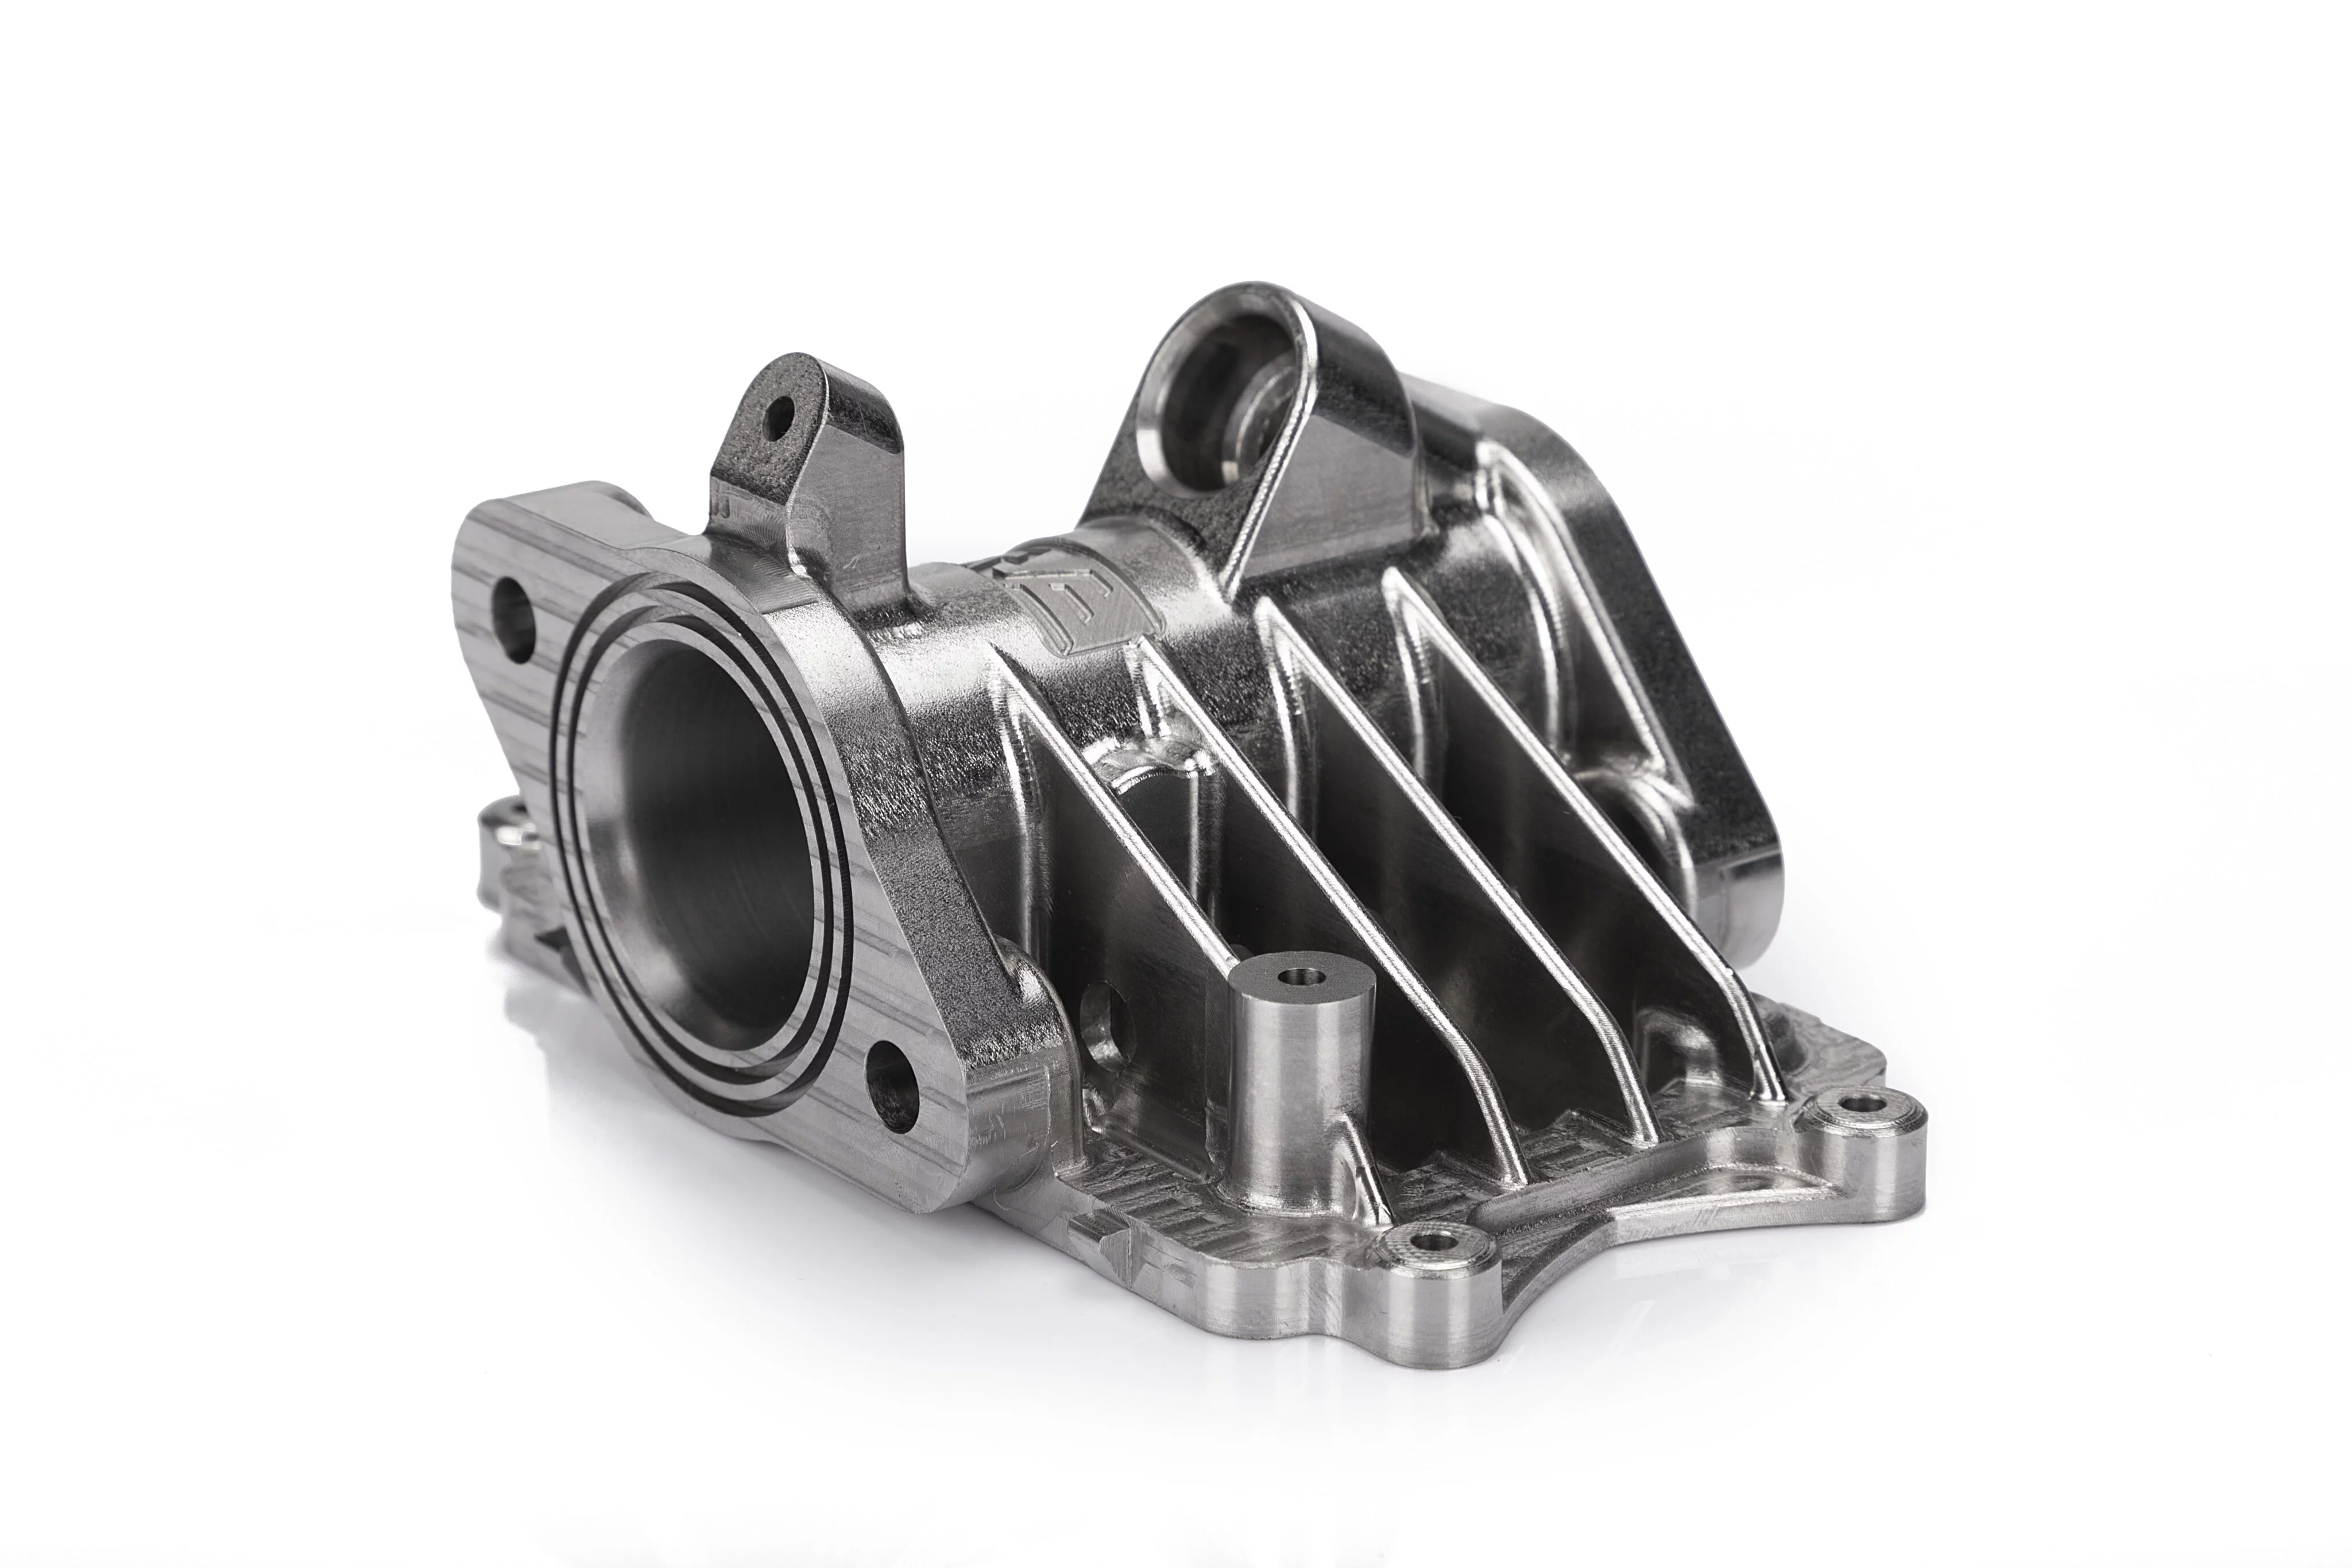
CNC machining handles complex 3D pockets, threaded features, and tight metal bending tolerance calls that a die cannot reach. In practice, many assemblies pair stamped brackets with machined housings. Choose the process that matches your part geometry, not the one your supplier pushes hardest.
Mistakes That Inflate Rework
Tolerances tighter than the die can hold consistently. Confirm with your tooling vendor what achievable sheet metal stamping tolerance is at your volume before specifying ±0.1 mm on every feature.
Skipping a die maintenance plan. A worn die shifts part dimensions after a few thousand hits, creating silent scrap.
Ordering below the volume that amortizes tooling. If you need 500 parts, stamped tooling may cost more per unit than a laser-cut batch.
Questions Buyers Often Ask
What material thickness range is practical for stamping?
Most presses handle 0.2 mm to 6 mm of steel, aluminum, or copper. Above 6 mm, dedicated blanking or forming dies become impractical, and sheet metal fabrication is the usual alternative.
How long does die tooling typically take?
Simple single-station dies: 4–6 weeks. Multi-station progressive dies: 8–14 weeks depending on cavity count and finishing. Confirm the schedule in writing before releasing the part.
Can I switch material grades after the die is built?
Often yes, if the new alloy has similar formability and thickness. Harder alloys may reduce part count per press stroke. Ask your supplier to verify press capacity before the switch.
How do I inspect incoming stamped parts quickly?
Check critical dimensions with calibrated calipers or CMM, verify bend angle with a protractor, and inspect edges for burrs or cracks. A 10-piece AQL sample per lot covers most sheet metal stamping quality agreements.
Making a Better Long-Term Decision
The right process choice saves rework cycles and keeps unit costs predictable once tooling is paid down. Send your part drawing, target annual volume, and material spec to YPMFG’s engineering team. They will return a feasibility note, a tooling cost range, and a recommended press schedule so you can compare offers without guessing.