
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Italian
 Portuguese
Quick answer:
Custom CNC aluminum 6061 parts are machined through turning, milling, or a combined setup, depending on your part geometry. 6061 is the most widely specified aluminum alloy for precision components because of its balance of strength, machinability, and anodizing response. Before ordering, verify your CNC turning or milling route, the temper (typically 6061-T651), and all critical tolerances. Rotational parts favor turning; complex multi-plane features favor milling. YPMFG supports both prototypes and batch production runs with full material traceability.
Most buyers overthink material selection and underthink process choice. A vague tolerance spec or a mismatch between part geometry and machine setup quietly adds cost and lead time. What follows is a practical walkthrough of what actually matters when ordering custom CNC parts in 6061.
What Makes 6061 the Default Choice
Aluminum 6061 is the go-to alloy for machined brackets, housings, fixtures, and structural components across aerospace, automotive, and industrial applications. Its tensile strength in the T6 temper sits near 45 ksi, which covers most load-bearing needs without the weight penalty of steel.
Machinability is the second reason it stays the standard. The alloy cuts cleanly at standard feed rates, produces predictable chip formation, and reduces tool wear compared to free-machining alternatives. It also takes Type II and Type III anodizing uniformly, which matters when your part needs corrosion resistance or a specific finish color.
If your part faces sustained temperatures above 100°F or high cyclic loads, confirm with your engineer whether 6061 or a 7075-series alloy is more appropriate. 6061 is the default, not the universal answer.

Turning vs. Milling: How to Pick the Right Process
CNC turning handles rotational geometry: shafts, bushings, flanges, connectors, and any part that would sit naturally in a chuck. The workpiece spins against a single-point tool, keeping cycle times short and consistent for higher volumes.
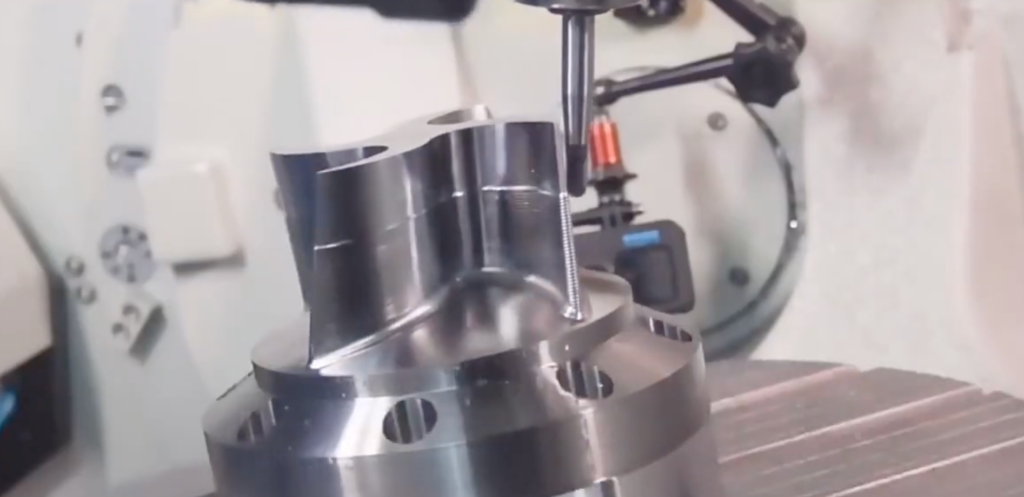
CNC milling covers everything else—brackets, enclosures, complex 3D contours, and parts with features on multiple axes. A 5-axis setup can hit undercuts and angled surfaces in one clamping operation.
Many production parts are a turning-milling hybrid. A short shaft with a milled slot and a threaded end section is the classic example. If your drawing shows features on more than one plane, ask whether a combined setup or a dedicated multi-tasking machine makes sense at your volume.
Specs to Verify Before Sending Your Drawing
Before you hand off a file, confirm the items below. Each one directly affects quote accuracy and whether the part arrives right the first time.
Once these are confirmed, request a DFM review from your machining partner. YPMFG’s engineering team will flag features that are hard to hold at your specified tolerance and suggest design tweaks that reduce cost without changing function.
Cost Drivers to Expect
Material is usually the smallest line on a 6061 quote. What moves the total is machining time, setup complexity, and post-processing. A part needing 5-axis milling, hand deburring, and Type III anodizing costs noticeably more than a simple turned bushing with a basic machine finish.
If your budget is fixed, the fastest lever is reducing operation count or relaxing a non-critical tolerance. Always ask for a line-item quote so you can see material, machining, finishing, and inspection broken out. That transparency makes it easier to adjust the design before tooling is committed.
Practical Questions Before Ordering
Do I need a first-article inspection report?
For any part going into a regulated or safety-critical application, yes. A FAIR documents measured dimensions against your drawing and confirms process stability before the full batch is released.
Can I get material mill certificates with each shipment?
You should. YPMFG provides heat-number-traceable material certification with every batch. This is standard practice in aerospace, medical, and automotive supply chains.
What file format works best for quoting?
Send a 3D STEP or IGES file alongside a 2D PDF drawing that includes all critical dimensions and callouts. A PDF alone works for simple turned parts, but a 3D model removes ambiguity on complex geometry.
How far ahead should I order for batch runs?
Lead time depends on quantity and finishing, but plan two to six weeks for moderate volumes. Set your design-freeze date early so the supplier can hold material stock and complete any needed tooling.
Making a Better Long-Term Decision
The real value of a well-specified 6061 part is consistency. The same drawing, the same tolerances, and the same finishing spec should produce the same result on every lot, whether that is fifty pieces or five thousand.
Send your drawings and specifications to YPMFG for an engineering review. The team will confirm process routing, flag tolerance conflicts, and return a transparent, itemized quote. You can also request sample builds before committing to a full production run.






