
 Italian
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Portuguese
Risposta breve:
Alluminio Lavorazione CNC produces parts with tolerances as tight as ±0.01 mm, typically machined from 6061, 7075, or 5052 alloy plate or bar stock. The three decisions that matter most before placing an order are alloy selection, finishing process, and tolerance class. Picking the wrong alloy or skipping the material spec sheet can result in parts that fail corrosion or load-bearing tests downstream. Also confirm whether the quoted price covers post-machining steps such as anodizing, deburring, or surface coating.
Why Aluminum Is the Default for CNC Machining
Aluminum is the go-to material for Parti lavorate con macchine CNC in aerospace, electronics, and medical device applications. Its low density cuts part weight, and high thermal conductivity keeps cutting speeds high, which reduces cycle time. For most non-structural applications, aluminum beats steel on a cost-per-part basis while still meeting strength and corrosion requirements.
Common applications include battery housings, heat sinks, sensor brackets, injection-molding tool plates, and drone frames. YPMFG supports buyers who need parti in alluminio su misura at prototype or production volumes without losing dimensional accuracy.
Alloy Selection: 6061 vs. 7075 vs. 5052
The right alloy depends on load, environment, and post-processing needs. Matching the grade to your actual service conditions avoids overpaying for strength you do not need.
7075 delivers the highest strength but machines slower and costs more per spindle hour. 6061 remains the most widely specified alloy because it balances strength, raw-material availability, and finishing options. If your part will see salt-water or chemical exposure, 5052 is the safer baseline. Always request a mill test certificate tied to the raw-material lot number so traceability is built in from the start.
Tolerance, Geometry, and Finishing
Tolerance class drives cost more than most buyers realize. A ±0.05 mm tolerance is standard for Pezzi torniti a controllo numerico and adds minimal machining time. Tightening critical dimensions to ±0.01 mm or less often increases cycle time by 30–50% and may require a dedicated fixture. Always state per-dimension tolerances on the drawing rather than applying a blanket value across all features.
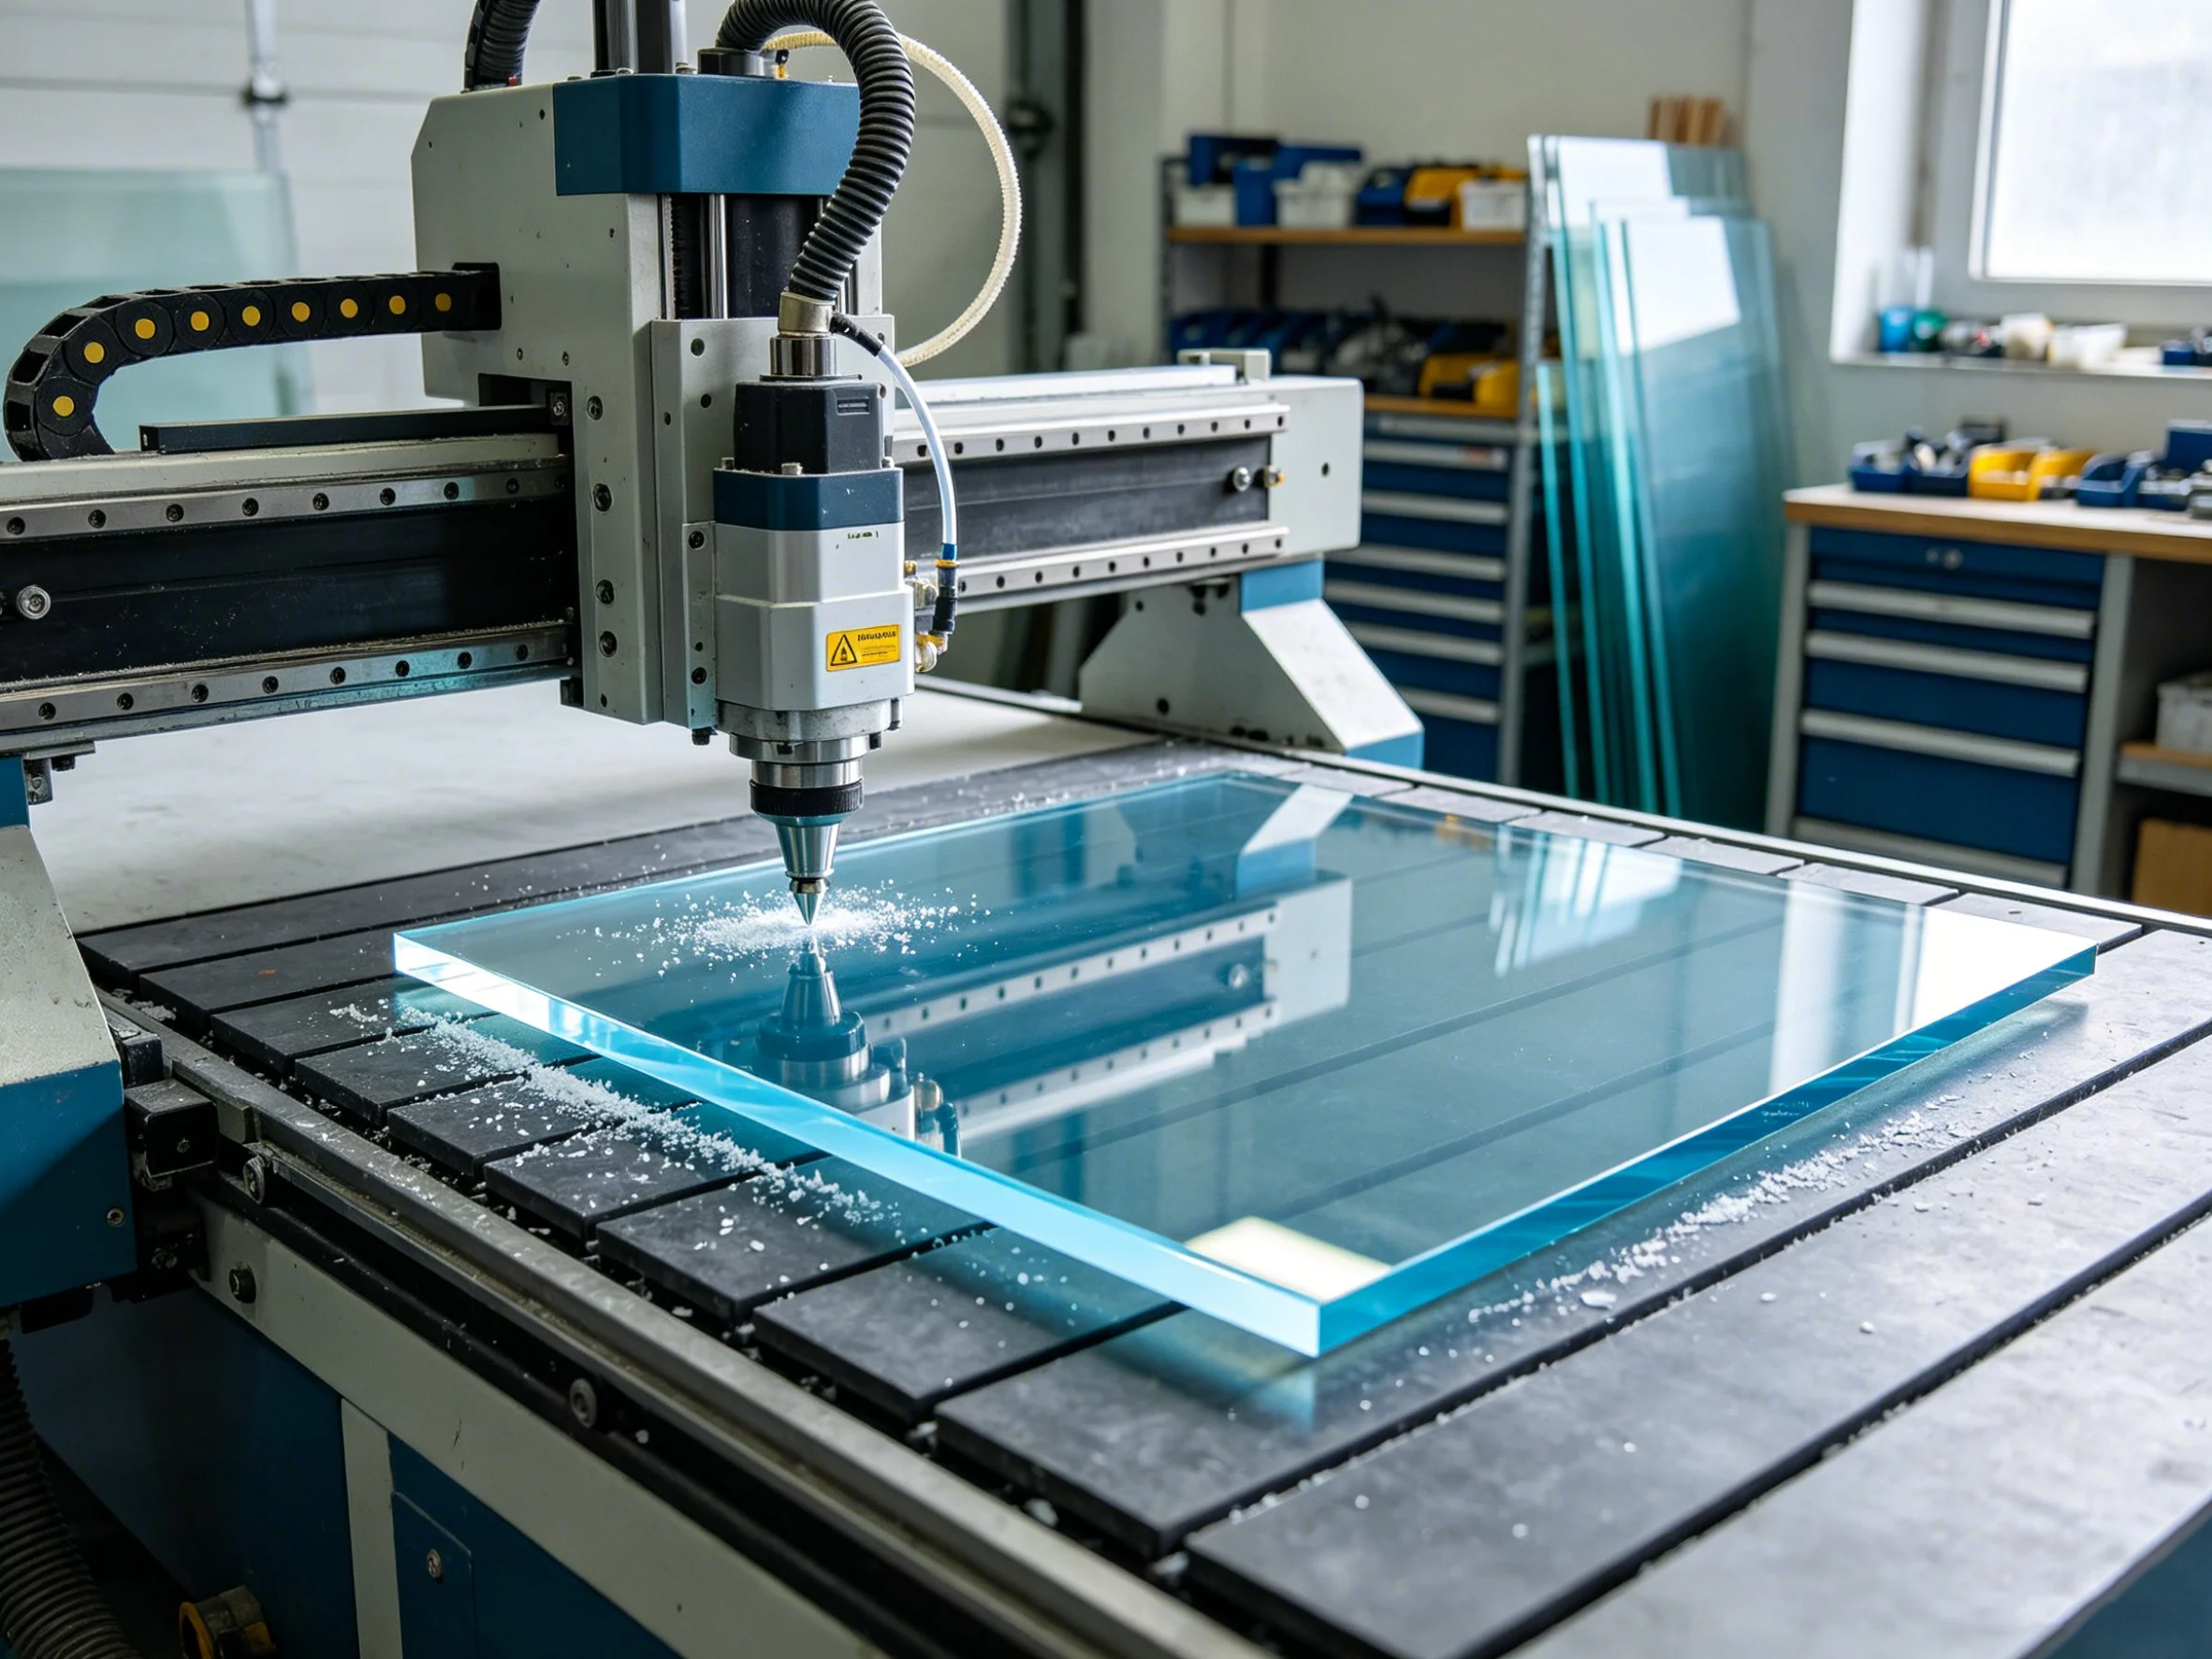
Finishing options range from mill finish to Type III anodizing, bead blasting, or powder coating. Each step adds lead time and cost, so specify only the finishes your functional requirements actually call for. Which finish matches your application is easier to settle during the engineering review stage, before tooling is committed.
Deep pockets, thin walls under 2 mm, and internal threading are the geometry features most likely to trigger design-for-manufacturability changes. Flag these early in the review process to avoid a second design iteration and the extra machining cost that comes with it.
Fattori chiave di costo
Five factors move the price of aluminum CNC parts the most:
Alloy grade and raw-material quantity
Tolerance class on critical dimensions
Part geometry (deep pockets, thin walls, internal features)
Finishing and coating requirements
Order volume and setup-cost amortization
For prototype runs under 10 units, setup fees dominate the quote. At 500+ units, per-part cost drops sharply because the CNC program and fixture are already in place. Negotiate tooling and material pricing as separate line items at higher volumes so you can see exactly where your money goes.
Pre-Order Checklist
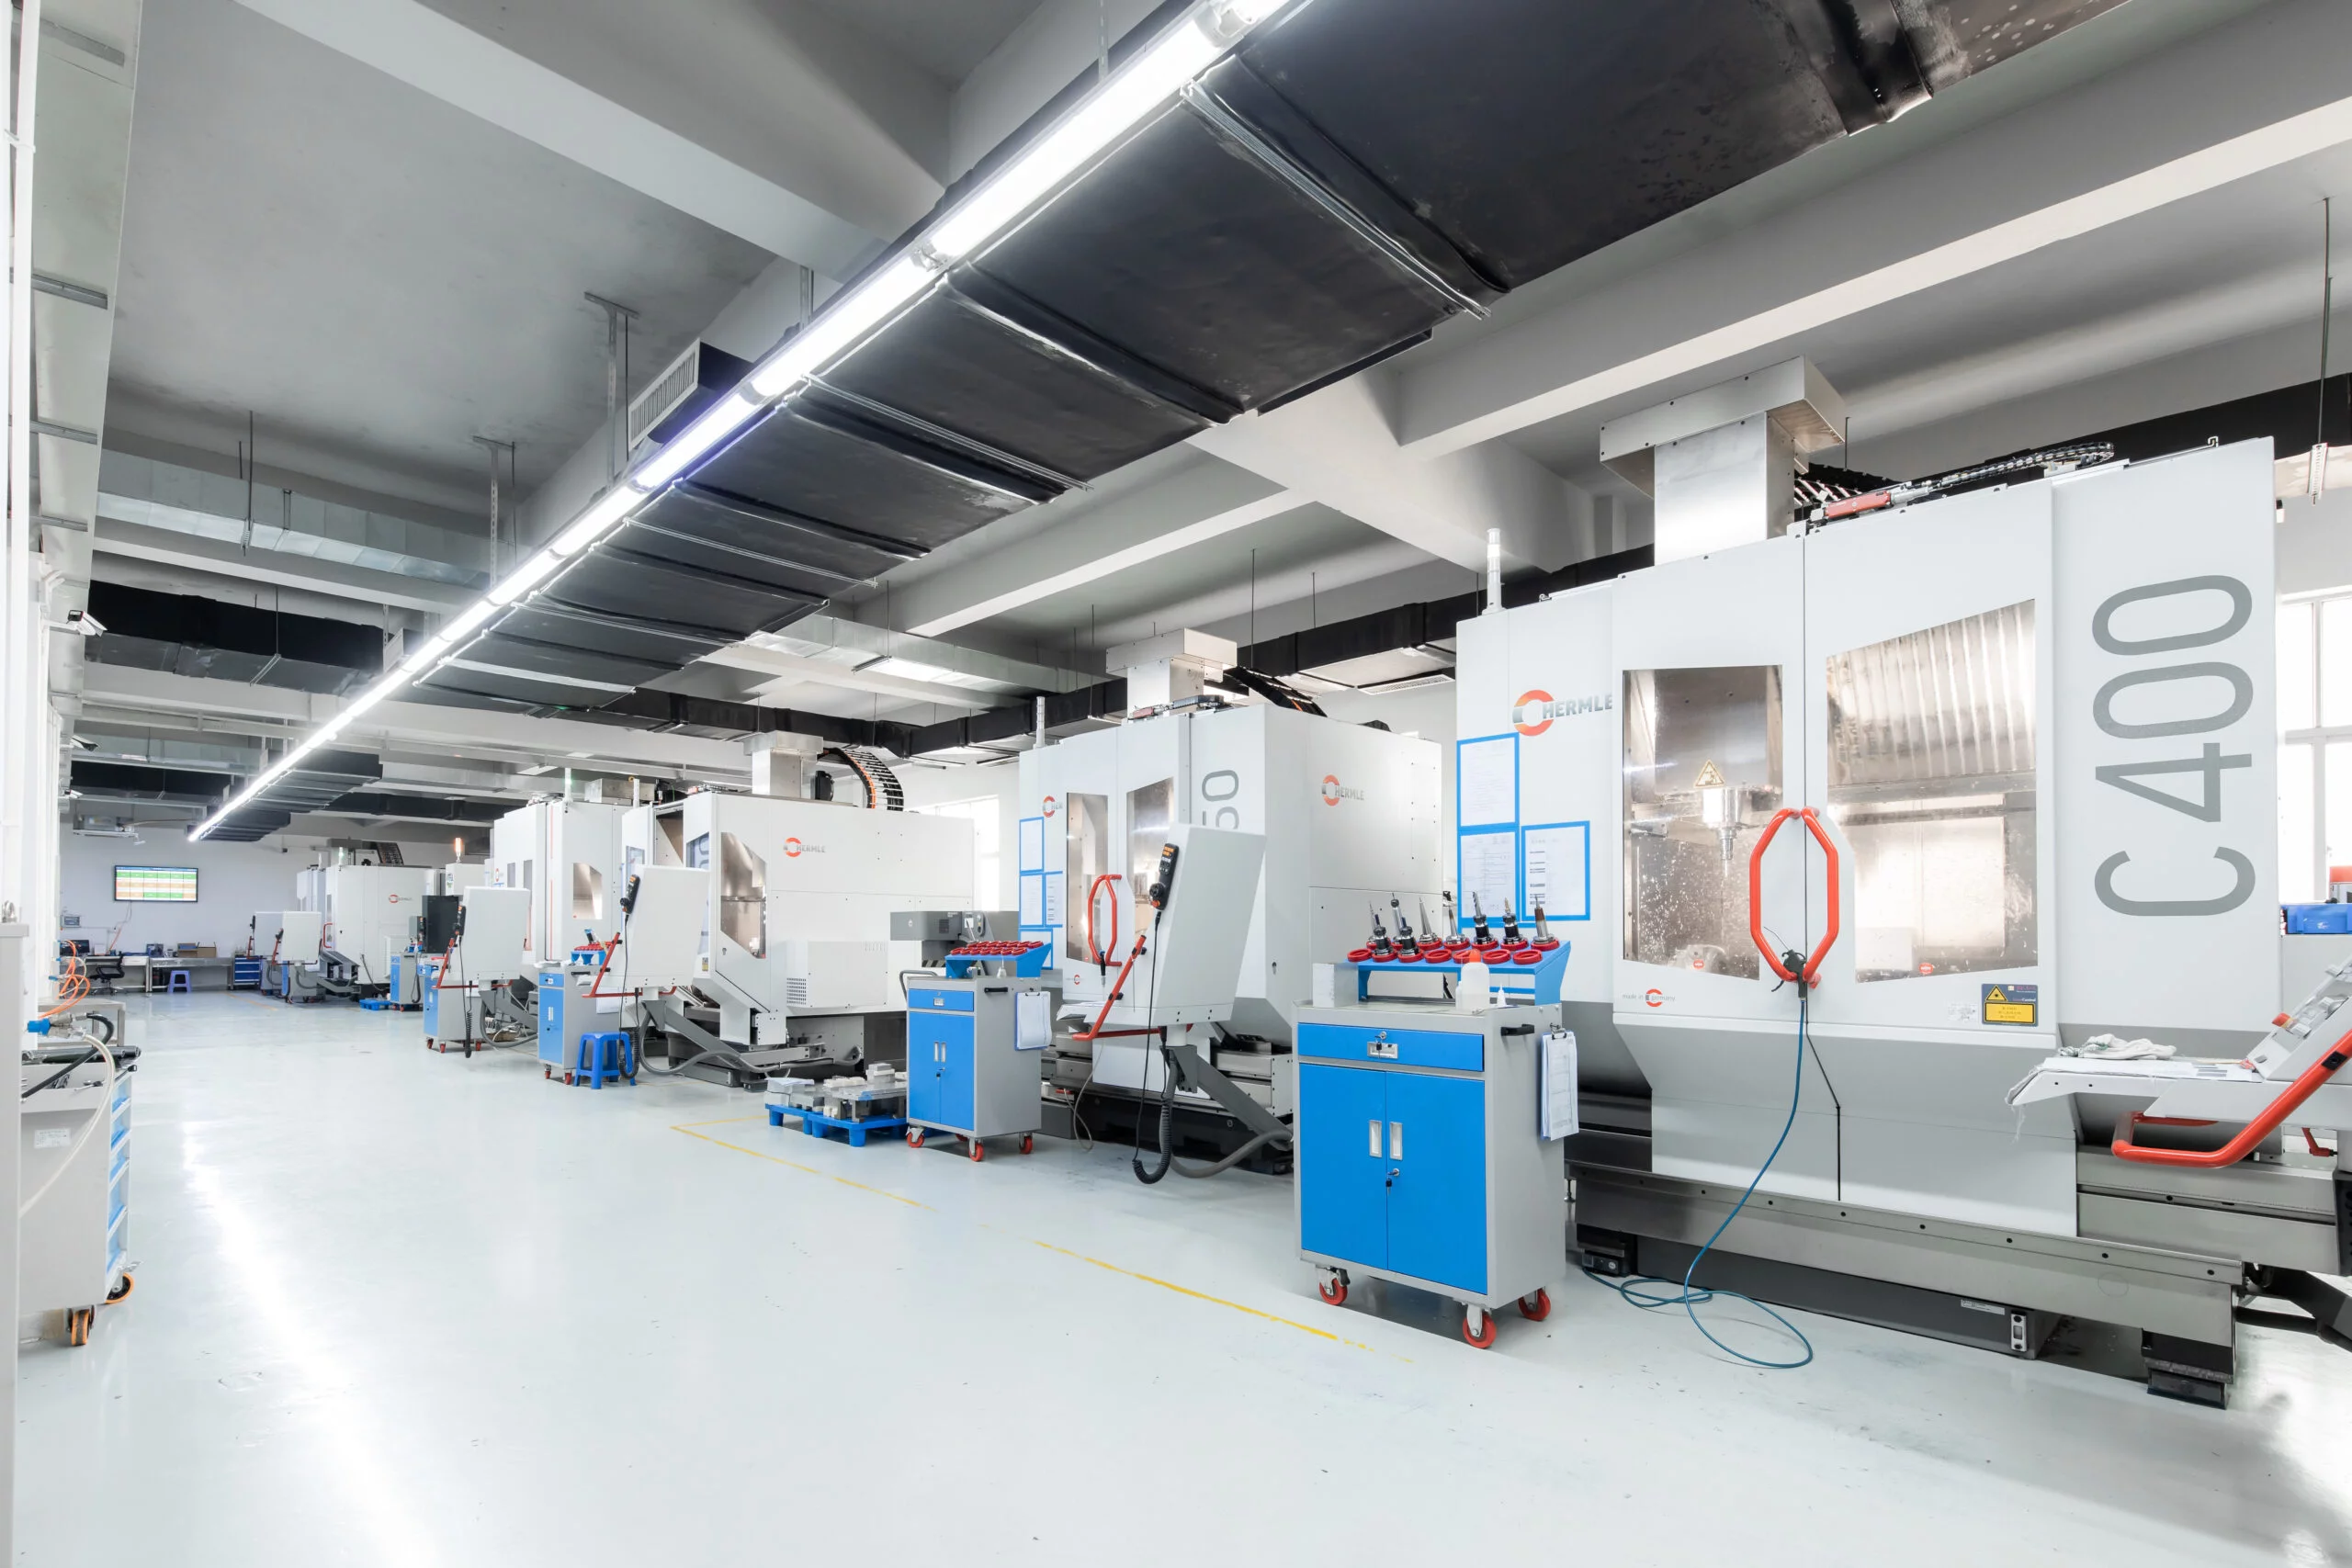
Before sending files to any CNC machining shop, confirm the following:
1. Alloy grade and temper (e.g., 6061-T651)
2. Critical tolerances stated per dimension, not as a blanket value
3. Surface finish specified as an Ra value, plus coating type
4. 3D model in STEP format with all threads and fillets called out
5. Inspection method and acceptance criteria (CMM, profile gauge, visual)
6. Whether the quote includes deburring, washing, and packaging
YPMFG reviews incoming engineering drawings and 3D models for manufacturability before quoting, flagging features that may need a design adjustment to avoid rework on the shop floor.
Common Questions About Aluminum CNC Parts
Can 6061 handle high-temperature environments?
6061 begins to soften above roughly 150 °C. For sustained heat exposure, 7075 or a purpose-built alloy is the better fit. Verify your maximum operating temperature before finalizing the alloy choice.
What is the minimum wall thickness for CNC-machined aluminum?
In practice, walls below 1 mm tend to flex during cutting. Most shops set 1.5 mm as a safe minimum, though success depends on workholding rigidity and tooling selection.
Does anodizing change part dimensions?
Yes. Type III anodizing adds approximately 10–25 µm per exposed surface. Design your part to account for this layer so mating components still fit within your assembly tolerance stack-up.
How many units should I order to reduce per-part cost?
The steepest cost drop happens between 10 and 200 units, where setup fees get amortized. Beyond 500 units, negotiate tooling and material pricing as separate line items.
What should I include in the material spec sheet?
State the alloy, temper,and any second-phase requirements such as mill-certified 6061-T651. Also call out the ASTM or AMS standard so the supplier can trace the raw material lot back to the mill.
Need Help Specifying Your Aluminum CNC Part?
Send your drawings or 3D files to YPMFG for a manufacturing feasibility review. You will receive a manufacturability assessment, recommended tolerances, and a line-item quote that separates machining, finishing, and inspection costs. This keeps your BOM and supplier comparison on the same page from the first quote.



