Japanese
 English
 German
 Russian
 Korean
 Spanish
 French
 Italian
 Portuguese
簡単な答え:
A desktop enclosure is a compact, self-contained housing for electronic or mechanical components, typically ranging from 200 mm to 600 mm in its largest dimension. Spec one well and you avoid assembly failures, heat issues, and rework. The three critical specs to lock down before ordering are enclosure dimensions (internal and external), material choice, and 許容範囲の仕様 for mating surfaces. Get these wrong and your 特注筐体 will not fit your PCB, connectors, or cooling layout, leading to costly re-machining cycles.
はじめに
Most product teams order a desktop enclosure, receive it, and discover the panel openings are 0.5 mm off, the heatsink sits proud of the surface, or the screw standoffs don’t align with the board. These problems trace back to unclear specs at the drawing stage. This guide walks through the exact parameters you need to define before sending files to a CNC加工 shop, so the first article arrives assembly-ready.
目次
Key Specs to Define
Material Selection
Sizing, Tolerances, and Fit
CNC加工 Considerations
Common Questions

Next Steps
Key Specs to Define
A desktop enclosure is not just a box. It houses a board, connectors, fans, and sometimes a small drive. Before you draft the drawing, list every component that must fit inside and note its footprint, height, and connector position. This becomes your internal volume requirement.
From there, define the external form factor: flat or rounded edges, mounting feet, cable glands, and ventilation openings. Each of these changes the wall thickness, the machining strategy, and the final part weight.
Material Selection
Material drives cost, weight, thermal behavior, and surface finish options. For most desktop applications, aluminum is the default because it machines cleanly, dissipates heat, and anodizes well.
材料の選定 also affects surface finish. If you need a matte black appearance, anodizing on aluminum or passivation on stainless changes the process and lead time. Confirm the finish with your machinist early.
Sizing, Tolerances, and Fit
The most common failure point is internal clearance. A PCB with surface-mount components needs 2–3 mm of top-side clearance for reflow; a board with tall connectors or a heatsink may need 8–12 mm. Spec your internal height as the tallest component plus a minimum 3 mm gap, then work outward to wall thickness.
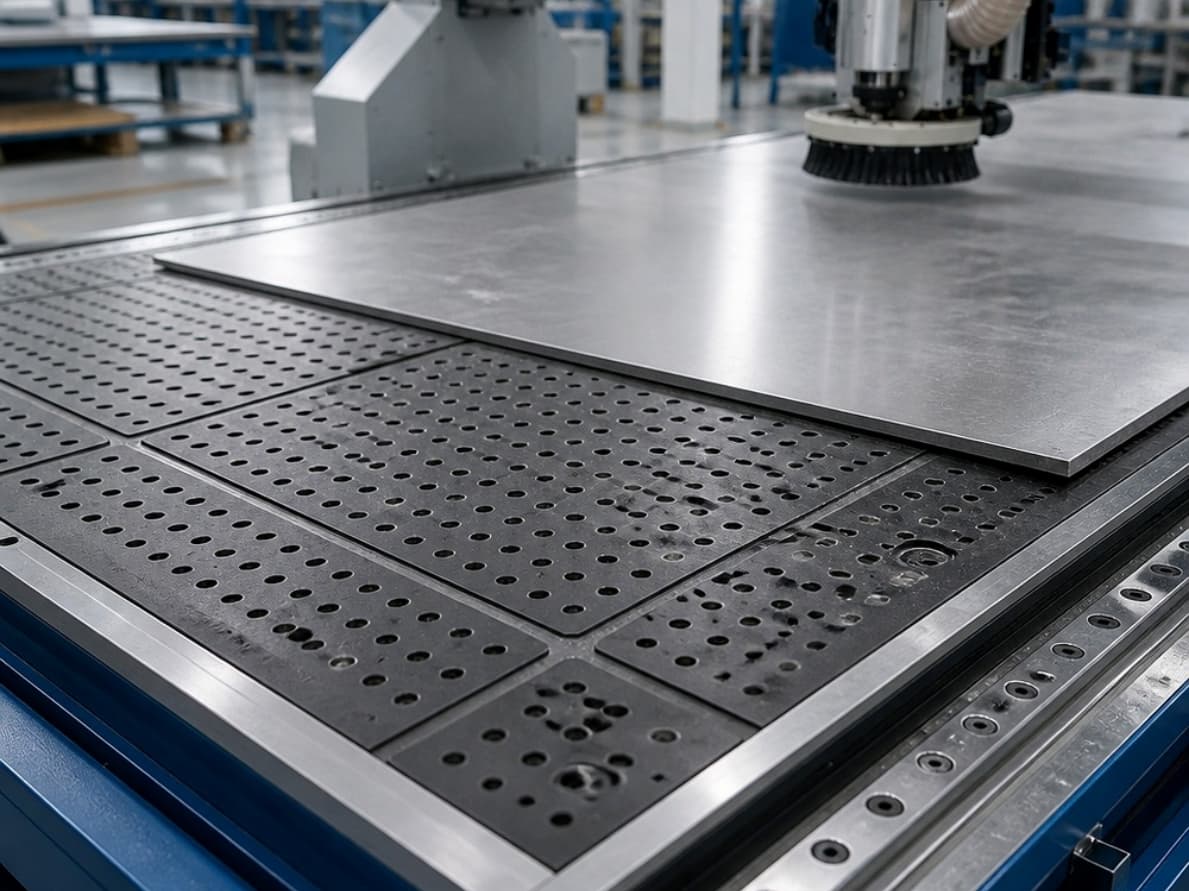
For panel openings (connector cutouts, switch recesses),call out 許容範囲の仕様 explicitly. A USB port opening machined at ±0.1 mm may leave too much play; ±0.05 mm is tighter but costs more in cycle time. State your acceptable fit class on the drawing.
許容差仕様 on mating surfaces (lid-to-base, door hinges, screw bosses) are where most first-article rework happens. YPMFG engineers review customer drawings and flag areas where standard 2D tolerances will cause assembly friction before cutting starts.
CNC Machining Considerations
Not every enclosure detail is equally easy to machine. Sharp internal corners below R2 mm require a second pass or a small end mill, adding cycle time. Wall thicknesses under 1.5 mm on larger panels may flex during machining and affect flatness.
If your aluminum enclosure includes a split lid with a hinge line, discuss the parting strategy with your machine shop. A machined seam is stronger than a cast one, but the seam line must be called out as a functional surface or painted zone.
Thermal management features such as fins, through-holes, or recessed pockets for a cold plate add machining depth. Confirm the maximum available Z-travel on the machine before committing to deep pockets. For most desktop sizes, 3-axis CNC is sufficient; 4- or 5-axis work is only needed for complex angled features.
CNC部品の製造 for enclosures typically runs 4–10 hours per unit at standard speeds, depending on material and detail density. YPMFG provides a cycle-time estimate with the quote so you can plan production batches accordingly.
Common Questions
What is the minimum wall thickness for a machined desktop enclosure?
Practically, 1.5 mm is the floor for 6061 aluminum on panels up to about 400 mm wide. Below that, the panel may flex under screw torque. Verify with your machinist for larger spans.
Can I add an IP rating to a standard desktop enclosure?
A sealed, gasketed enclosure can reach IP54 or IP65 depending on the gasket material and fastening method. IP67 and above usually require a different design approach, such as a potted or welded construction.
What file formats do I need to send for CNC machining?
DXF or DWG for 2D profiles, STEP for 3D bodies, and a PDF or drawing sheet with all dimensions, tolerances, and finish notes. YPMFG accepts STEP, IGES, DXF, and annotated PDFs.
How many prototypes before I commit to a production batch?
Most teams run one or two articles to verify fit, finish, and function. If the part has a complex hinge or multiple mating surfaces, budget a third article to confirm repeatability.
Do I need to specify the anodize color on the drawing?
Yes. Call out the finish (e.g., Type II anodize, 10–15 µm, black) and the referenced Munsell or Pantone swatch. Unspecified finishes default to natural or clear, which may not match your product palette.
より良い長期的な決断を下す
A well-specified desktop enclosure saves you rework, protects your components, and shortens your path from prototype to production. Lock down internal volume, material, tolerances, and finish before you release the drawing. If any parameter is uncertain, send your current CAD files and a brief note to YPMFG. The team reviews the geometry, flags risky features, and returns a revised drawing with recommended tolerances and a 特注筐体 quote within a few business days.