Portuguese
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Italian

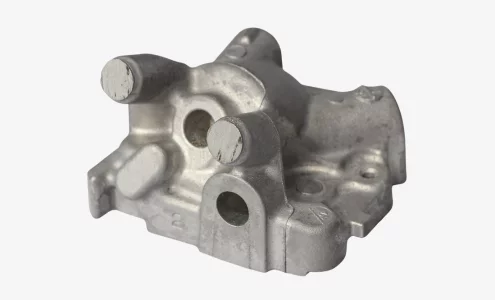
Die casting manufacture is a metal forming process in which molten aluminum, zinc, magnesium, or copper alloy is injected under high pressure into a hardened steel mold. The result is a near-net-shape part with tight tolerância dimensional and a smooth surface finish, ready for limited or no secondary machining. The process is widely used in automotive, aerospace, and industrial equipment sectors because it balances high production volume with consistent geometry. For any buyer, understanding the casting process, material grade, and quality checkpoints is essential before committing to a production order.
Most buyers approach die casting manufacture focused on unit price alone. This is a frequent source of downstream cost and quality problems. Material grade, tooling investment, porosity control, e post-casting machining requirements all influence total project cost and part reliability. What follows is a practical breakdown of what to verify before you place an order.
The Die Casting Process in Brief
Each cycle starts with a dry or lubricated mold cavity. Molten metal is then injected at pressures ranging from 200 to 1,500 bar, depending on alloy and part geometry. After a few seconds of solidification, the part is ejected and trimmed. The entire cycle for a small component can run under 30 seconds, which is why die casting suits high-volume production better than sand casting or investment casting.
Tool life is a critical variable. A well-maintained die casting tool can survive 50,000 to 200,000 shots, but thermal fatigue and erosion at the gate and runner areas will shorten that window. Buyers should confirm how many shots the tooling has already consumed and whether the vendor follows a documented inspection schedule.
Material and Design Choices That Drive Quality
The most common alloys are fundição de alumínio sob pressão grades A380 and ADC12, and fundição sob pressão de zinco grades ZA-3 and ZA-5. Aluminum offers a better strength-to-weight ratio and corrosion resistance, while zinc tolerates sharper features and thinner walls. Magnesium alloys are used where weight savings are critical, at a premium cost.
Design dictates everything. Wall thickness below 1.5 mm in aluminum increases porosity risk. Internal ribs should taper at least 3 degrees to allow clean ejection. If your part has deep pockets or asymmetric features, request a simulation report from the supplier before tooling is cut. YPMFG can review part drawings and flag casting-related design issues early, helping you avoid expensive retooling later.

Cost Factors to Budget For
The following table lists the major cost layers most buyers underestimate:
The single largest hidden cost is often secondary machining. If your print calls for machined bore tolerances of ±0.02 mm on a cast part, budget for post-casting machining capacity and verify that the caster controls that step in-house or through a bonded partner.
Common Procurement Mistakes to Avoid
Ordering without a material mill certificate. Always request a heat-number traceability document for each batch.
Ignoring porosity acceptance criteria. Specify whether you follow AWWA C412, ASTM B873, or an in-house X-ray or CT scan protocol.
Accepting a first-article inspection report with no dimensional data. The report should include actual measurements at every critical-to-quality dimension.
Pular um die casting procurement checklist that covers tooling ownership, lead-time penalties, and rework terms.
Choosing the cheapest quote without confirming whether the quoted price includes gating, sprue removal, deburring, and coating.
Each of these gaps surfaces in the field as returned parts, line stoppages, or warranty claims that far exceed the initial savings.
## Questions Buyers Often Ask About Die Casting Manufacture
What wall thickness should I design for in aluminum die casting?
For most structural aluminum parts, 2.5 mm to 3.0 mm wall thickness is the sweet spot. Thinner walls below 1.5 mm significantly raise the risk of hot tearing and internal porosity. Confirm your geometry with the caster before finalizing the print.
How is die casting different from sand casting for my application?
Die casting delivers tighter dimensional tolerance, smoother surfaces, and faster cycle times. Sand casting suits larger, lower-volume, or single-material parts. If your run exceeds a few thousand units and the part fits a die casting machine envelope, die casting is usually the cost-efficient path.
Do I need to own the die casting tooling or can I rent it?
Both models exist. Tooling ownership gives you long-term cost stability and portability across suppliers. Rental or shared-tooling arrangements reduce upfront capital but add per-shot licensing fees. Run a 36-month total-cost comparison before deciding.
What lead time should I expect from quoting to first articles?
A typical timeline is 4 to 8 weeks for tooling design and fabrication, followed by 1 to 2 weeks for tryout and first-article inspection. Complex multi-cavity tools or exotic alloy setups can push this to 12 weeks or more.
Can I switch alloys mid-production without retooling?
In many cases, a minor tooling modification handles the switch, but thermal behavior and shrinkage differ between aluminum and zinc. Run a short trial batch and re-inspect critical dimensions before releasing full production. YPMFG supports alloy-change evaluations and can model shrinkage differences for your specific geometry.
## Making a Better Long-Term Decision on Die Casting Manufacture
The right die casting partner is not the one with the lowest per-unit quote. It is the one who walks you through material traceability,porosity acceptance, tooling maintenance data, and secondary machining control before you commit. Send your part drawings and specifications to YPMFG for an engineering review. The team will flag design risks, recommend alloy and finishing options, and return a detailed quotation with clearly separated tooling, unit, and finishing line items—so you can make a comparison that reflects true cost, not just sticker price.