Portuguese
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Italian

TIG gives tighter control on thin sheet; MIG wins on speed for thicker gauges. Under 1.5 mm, TIG is typically the safer pick to avoid burn-through.
The real choice comes down to three variables: base-metal thickness, production volume, and surface-finish tolerance. A wrong match means burn-through, heat distortion, or a rework cycle that eats your margin. YPMFG’s fabrication team weighs all three before recommending a weld process on any sheet-metal order.
Key Takeaways
- TIG weld penetration: Below 1.5 mm sheet, TIG limits the heat-affected zone and cuts warpage risk.
- MIG production speed: MIG lays down filler roughly three times faster, making it the default for runs above 50 parts.
- Sheet thickness threshold: 1.5 mm is the common crossover where MIG’s speed advantage outweighs TIG’s precision.
TIG vs MIG on Sheet Metal at a Glance

Below the 1.5 mm line, TIG’s smaller thermal input keeps distortion in check. Above it, MIG’s wire-feed speed makes the cycle time work for most production shops.
What Thickness of Sheet Metal Should You TIG-Weld?
TIG works best on sheet from 0.5 mm up to about 2 mm. The narrow arc concentrates heat in a small zone, so the parent metal barely warps. Below 0.5 mm you enter the territory of resistance or laser welding.
On thinner material the operator controls amperage and travel speed to keep the molten pool small. Too much heat and the sheet curls or the joint cracks on cooling. MIG at the same gauge often punches through before the pool sets.
The hard limit is physical: a single TIG pass on 1 mm steel tops out around a 3 mm bead width. If the joint needs a wider fill, a second pass re-heats the first and raises distortion risk.
Next step: check your thinnest joint. If it is under 1.5 mm and the seam is visible,plan the TIG route first.
Where MIG Outperforms TIG on Sheet Metal
MIG’s continuous wire feed deposits filler three to four times faster than TIG’s manual rod. For a batch of 200 bracket seams, that speed gap is the whole argument.
The trade-off is spatter. Solid-wire and flux-cored MIG throw small droplets across adjacent faces. On a painted or anodized panel you will grind and sand. TIG leaves a clean, uniform bead with no cleanup pass.
MIG also handles thicker stock more comfortably. Past 3 mm, TIG needs multiple passes and the joint gets hot enough to warp the whole panel. MIG’s higher heat input fills the gap in a single run.
The hard limit: on gauges under 1 mm, MIG’s minimum arc energy still overshoots. You will see burn-through before the wire feeds enough to bridge the gap.
For runs under 20 parts on visible panels, TIG still wins. For everything else, MIG keeps the line moving.
How Do Tolerance and Finish Requirements Steer the Choice?
When the drawing calls for a visible seam on a housing or a food-grade panel, TIG is the default. The bead is uniform, spatter-free, and easier to pass a visual inspection.
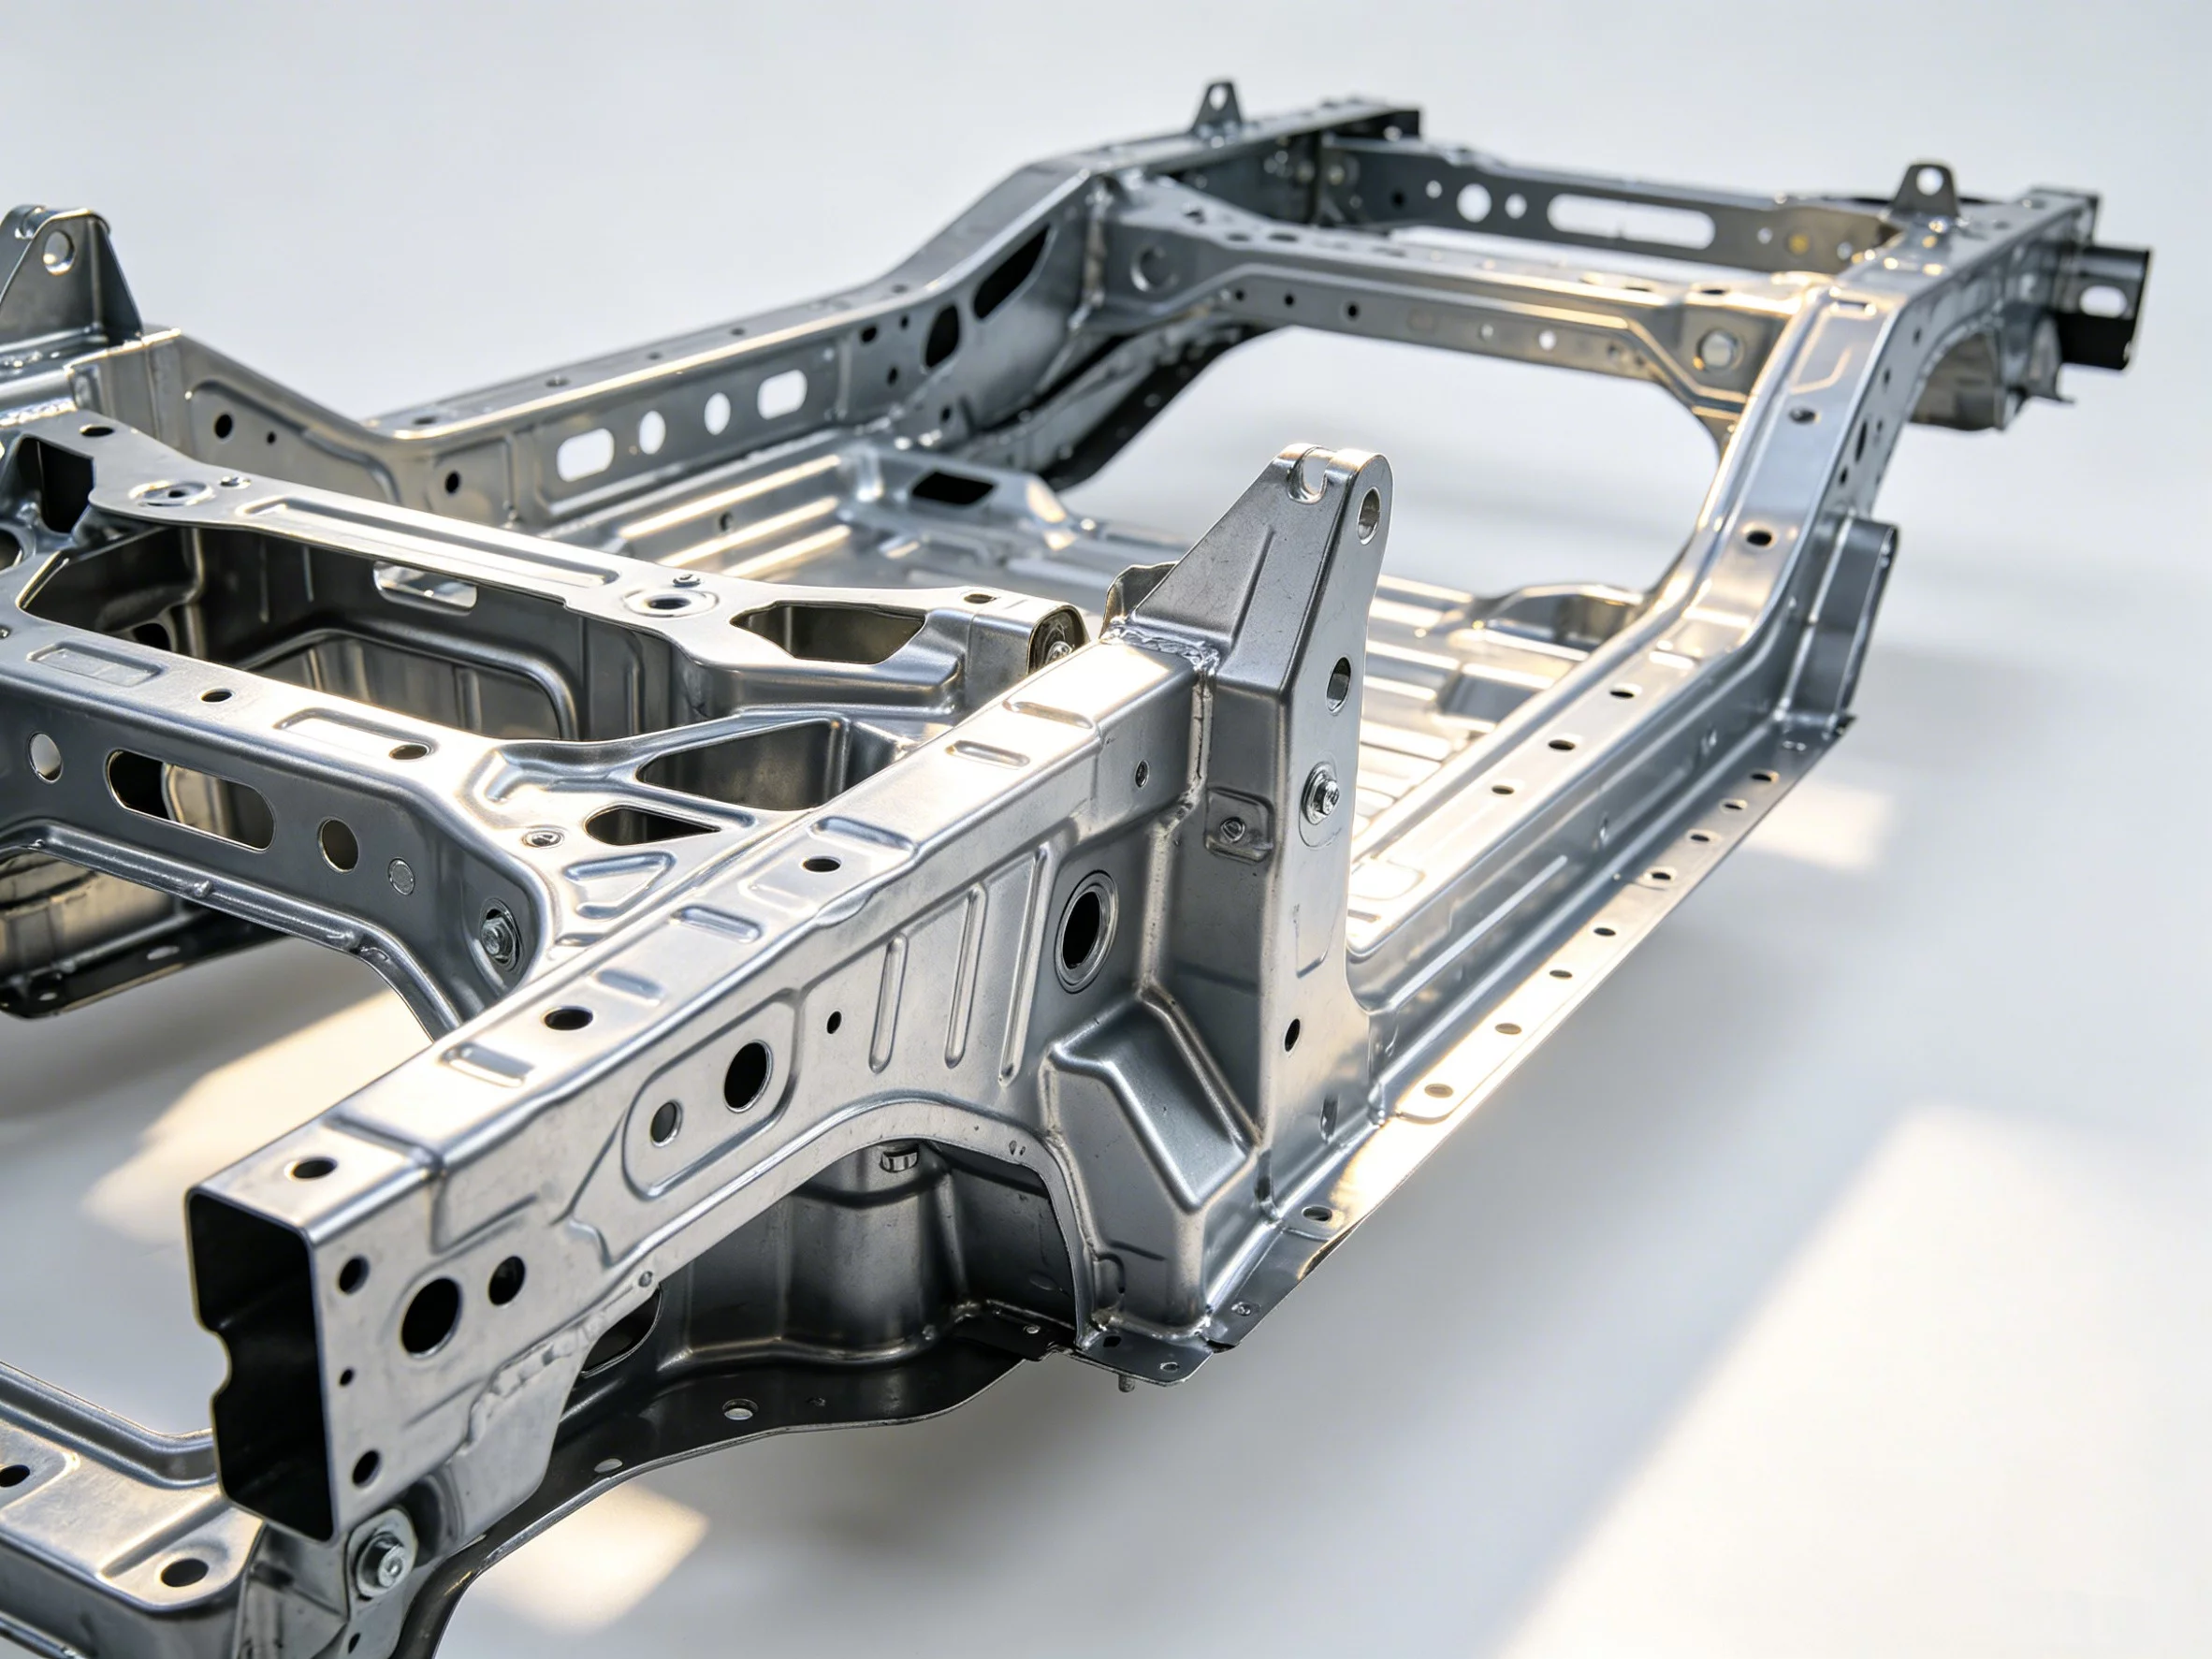
For internal structural brackets or chassis rails, MIG is acceptable. Spatter lands on non-visible faces, and the speed saves hours across the batch. A quick deburr and paint covers any residue.
Argon-helium gas-shielded MIG can tighten the bead on stainless, but it still cannot match TIG’s cosmetic consistency on a 1 mm panel. The physics of a continuous wire versus a filler rod sets the floor.
Check your inspection spec: if it reads “no spatter within 5 mm of joint,” MIG will fail on thin sheet regardless of gas mix.
How a Sheet-Metal Weld Route Looks in Practice
Take a typical 1.2 mm 304L stainless enclosure with four corner seams and two internal braces. The mixed route below is the one most shops run.
Step 1: Clamp and tack. Tack each seam with short TIG pulses spaced 6 mm apart to hold geometry before the root pass.
Step 2: Root pass in TIG. Run typically 90-110 A with 2 mm or 2.5 mm 304L rod, travel speed matched to a 4 mm pool width.
Step 3: Cap and internal braces in MIG. Switch to 1.0 mm ER308L, typical wire speed 1.2-1.5 m/min, argon-shielded. This handles the thicker joints fast.
Step 4: Post-weld check. Dye-penetrant on all seams. Log results against the FAI template.
Process Route Reference: YPMFG process library, reviewed against published wire and rod data. Client-specific amperage values withheld per NDA.
The mixed TIG-plus-MIG route keeps visible seams clean and internal work fast. No single process covers both needs on one panel.
Practical Questions Before You Pick a Process
Can MIG weld 0.8 mm sheet without burn-through? No. Minimum arc energy on most MIG units overshoots the melt depth at that gauge. You will punch through before the wire fills the gap.
Does TIG handle 3 mm carbon steel in one pass? It cannot. A single TIG pass on 3 mm mild steel leaves an unfused root. You need a prep bevel and at least two passes, which multiplies cycle time.
How do I decide in under five minutes? Check two numbers: thickness and part count. Under 1.5 mm and low volume points to TIG. 1.5 mm and above, or a batch over 50, points to MIG.
Choosing the Right Weld Process for Your Sheet Metal
The right pick protects your yield rate, keeps distortion inside tolerance, and avoids a rework loop that costs more than the parts themselves. Thickness, volume, and finish spec are the three numbers that drive the decision. Get them right and the process choice is nearly automatic.
YPMFG can review your drawings, flag the seams that will fail in MIG, and confirm the TIG parameters your shop needs. Send your specifications and a short note on finish requirements, and the engineering team will return a process recommendation within two business days.