Japanese
 English
 German
 Russian
 Korean
 Spanish
 French
 Italian
 Portuguese
簡単な答え:
A precision casting part is a metal component produced through controlled foundry processes that hold tight dimensional tolerances, typically within ±0.1 mm or better. Unlike standard sand casting, precision methods such as investment casting and die casting minimize downstream machining while delivering consistent geometry, 表面仕上げ, and material integrity. Before ordering, verify the alloy grade, critical dimensional tolerances, required Ra value, and applicable inspection standards. For safety-critical or high-reliability applications, material certification and process capability data are essential documentation to request before committing to a production run.
Many procurement teams treat casting parts as commodity items and place orders based on unit price alone. This approach creates quality risk, rework, and schedule delays that are expensive to recover from. The real decision hinges on whether the part’s tolerance, material, and finish match the functional requirement in your assembly. YPMFG supports buyers in matching casting specifications to actual application demands so the part performs correctly without excess downstream work.
Contents
What Makes a Precision Casting Part Different
ご注文前に確認すべき主な仕様
Precision Casting vs. Machining from Solid
Common Mistakes When Specifying a Casting Part

購入者からよく寄せられる質問
用途に適した部品の選び方
What Makes a Precision Casting Part Different
Precision casting differs from standard casting in three core areas: dimensional accuracy,surface finish, and process repeatability. Standard sand casting often leaves 1.5–3 mm of excess material that must be removed by secondary machining. Investment casting and die casting can hold tolerances as tight as ±0.05 mm with finishes in the Ra 3.2–6.3 µm range, reducing or eliminating that downstream work. The trade-off is higher process complexity and a larger minimum order quantity.
If your part features thin walls, complex internal channels, or a production run above a few hundred units, casting typically offers a lower total cost than machining from solid stock. The key is matching the casting process to the geometry and volume your application actually requires.
ご注文前に確認すべき主な仕様
Before sending a quotation request, confirm the following with your engineering team. Each missing field adds risk of non-conformance and rework:
Missing any of these fields in your drawing will slow down quoting and increase the chance of a non-conformance at inspection. If you are unsure which tolerance level is functionally required, send your assembly context to YPMFG for an engineering review before finalizing the drawing.
Precision Casting vs. Machining from Solid
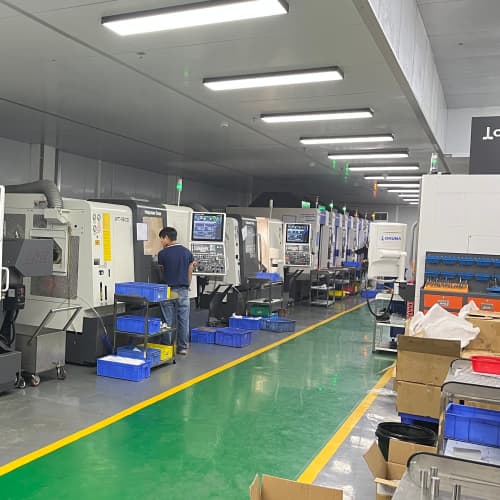
The choice between casting and CNC加工 depends on part geometry, material, and production volume. Machining from solid bar or plate offers the tightest tolerances and suits low-volume, high-complexity parts where near-net-shape casting is not feasible. Casting wins when the part has internal channels, thin uniform walls, or a run above a few hundred units.
For hybrid approaches, a near-net-shape cast blank followed by limited CNC work on critical surfaces often gives the best balance of cost and accuracy. In many cases, removing just 0.5 mm of material on the bearing seat or sealing surface is enough to meet the functional requirement without a full machining operation.
Common Mistakes When Specifying a Casting Part
Buyers frequently overlook two issues that cause problems at the production stage. The first is specifying a tolerance tighter than the casting process can reliably hold. Calling out ±0.01 mm on a sand-cast wall will force a machining step that defeats the purpose of casting. The second is omitting the heat-treatment specification. An alloy’s mechanical properties can vary significantly depending on the temper condition, and without a defined spec the foundry may deliver a part that passes dimensional inspection but fails in service. Always cross-reference your drawing’s tolerance callouts with the selected casting process capability before releasing the order.
購入者からよく寄せられる質問
What materials does the supplier support?
Confirm the alloy family—aluminum, magnesium, stainless steel, tool steel, or superalloys—and whether 材料のトレーサビリティ documentation is available per heat lot. This matters for aerospace and medical applications where full traceability is a regulatory requirement.
Can the supplier hold the tolerance you need?
Ask for process capability data on the critical dimension. A Cpk above 1.33 indicates stable, repeatable production across multiple batches rather than a one-off test result.
What surface treatment is included or separate?
Anodizing, passivation, heat treatment, and coating each add lead time and cost. Clarify whether the quoted price covers the finish or only the as-cast part.
What is the minimum order quantity and tooling investment?
Die casting and investment casting each have different MOQ thresholds and tooling amortization models. This directly affects your unit price at low volumes.
用途に適した部品の選び方
Match the casting process, alloy, and tolerance band to your part’s functional role rather than a generic “high-precision” label. Send your drawing, material specification, and target application context to YPMFG. The engineering team can review process fit, recommend the appropriate casting method, flag potential porosity or shrinkage risks, and return a quotation with a documentation plan. For buyers evaluating whether to switch from a machined part to a cast blank, a simple comparison of total cost per unit—material, labor, inspection, and tooling amortization—often makes the decision clear.