Japanese
 English
 German
 Russian
 Korean
 Spanish
 French
 Italian
 Portuguese
簡単な答え:
CNC turning and CNC machining are fundamentally different processes. Turning rotates the workpiece against a fixed tool, producing cylindrical parts efficiently. Machining moves the tool against a stationary workpiece, enabling complex multi-axis geometries. The right choice depends on part shape, 許容誤差要件, material, and 生産量. For symmetrical, round components, turning is typically faster and more cost-effective. For parts with features on multiple axes, multi-axis machining is the appropriate method.
Selecting between these two approaches is one of the first decisions buyers face when specifying CNC部品の製造. A wrong match between process and part geometry can add cost, extend lead time, or compromise dimensional accuracy on the finished component.
## What Is the Difference Between CNC Turning and CNC加工?
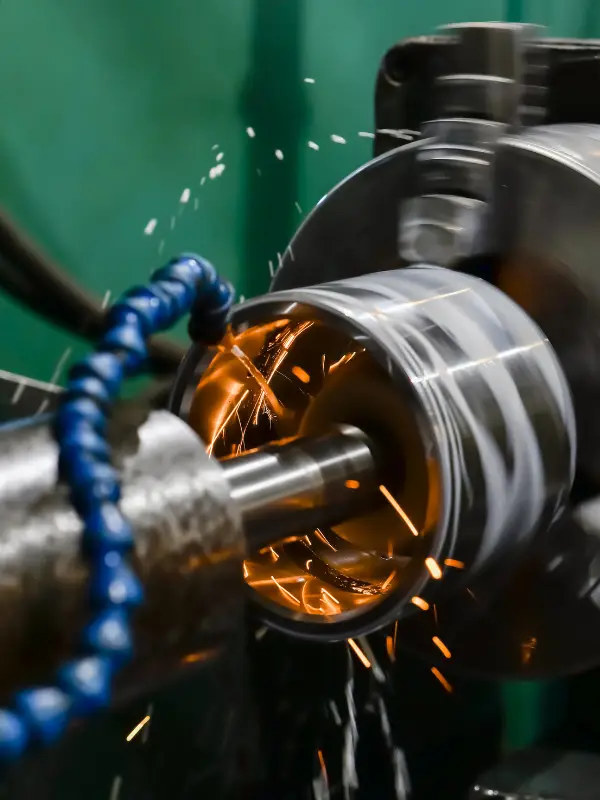
CNC旋盤加工, also called CNC lathe work, removes material by rotating the blank around its longitudinal axis while a cutting tool advances along defined paths. The tool stays largely stationary in angular position, and the rotation does the shaping. This makes the process ideal for shafts, bushings, connectors, and any part of revolution.
CNC加工 holds the workpiece fixed while the tool moves in two to five axes. It removes material from multiple directions, producing bores, pockets, threads,and irregular contours that a single lathe setup cannot reach in one operation.
The core distinction is geometry: turning handles radial symmetry, while machining handles arbitrary three-dimensional shape.
Process Comparison at a Glance
After reviewing the table, one takeaway stands out: part geometry drives the process choice more than material or lot size alone.
When to Choose Turning Over Machining
If your part is primarily cylindrical with features like diameters, chamfers, grooves, and axial threads, turning operations are usually the economical path. The lathe removes material in a single continuous rotational pass, which keeps cycle times short and tool wear predictable across a run.
Turning also excels at high-volume production of identical round components. Because the setup is simpler, changeover between parts is faster, and per-unit cost drops as volume increases.
Even at prototype quantities, a single-setup turning job can beat machining the same shape on a mill in terms of both cost and lead time.
When Multi-Axis Machining Is the Right Call
Parts with cross-drilled holes, non-cylindrical pockets, or features on faces that are not concentric to the main axis require a 3-, 4-, or 5-axis machining center. A two-axis lathe simply cannot reach those geometries without multiple setups, which introduces cumulative positional error.
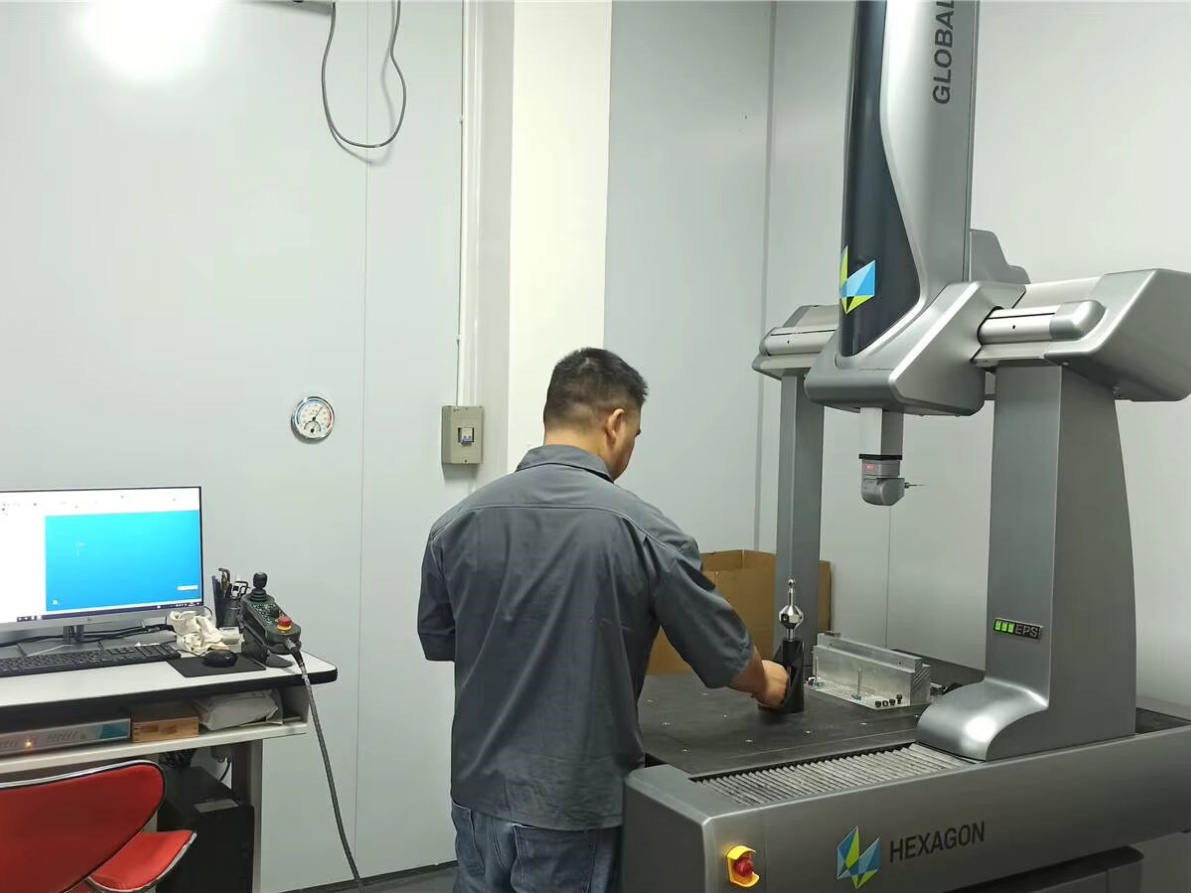
YPMFG supports projects that need hybrid processes, where a rough turned blank is finished on a multi-axis machining center in a single fixture. This reduces secondary handling and holds tighter tolerances across mating surfaces.
For assemblies where a turned shaft mates with a machined housing, running both operations under one roof avoids the dimensional drift that occurs between two separate shops.
Cost, Tolerance, and Material Considerations
Per-part cost is driven less by the label “turning” or “machining” and more by three variables: material grade, feature density, and lot size. A simple turned brass fitting in 5,000 units costs far less than a machined titanium bracket in 20 units.
Material removal rate also affects pricing. Softer materials like aluminum and engineering polymers cut faster than hardened steels or Inconel. If your drawing calls for a material with unusual hardness or a post-heat-treatment requirement, request an engineering review before finalizing the quote.
YPMFG can help buyers compare process options and estimate total ownership cost, including tooling amortization and inspection overhead, before committing to a production run.
Practical Questions Before You Specify
Is my part of revolution? If every cross-section along the axis is circular, turning is almost always the default starting point.
Does the part need features on non-concentric axes? Cross-bores, offset pockets, or angled faces push you into machining territory or a combined turning-machining sequence.
What is the minimum lot size and target tolerance? Tight tolerances under ±0.01 mm over long features may require a combined process rather than one method alone.
Which material and finish are specified? Surface finish, heat treatment, and plating requirements add operations beyond the primary cutting step.
Can the part be held in one fixture through all operations? Single-fixture setups reduce setup error and improve repeatability, especially at smaller batch sizes.
Getting the Right Process Recommendation
The safest path is to send your drawing or 3D model to a manufacturing partner early, before finalizing tolerances and material callouts. A process review at the design stage catches costly mismatches that would otherwise surface late in production.
YPMFG offers engineering evaluation, custom CNC components quoting, and documentation support for buyers who want to confirm that their part is assigned to the correct process before release. Send your specifications for a review and receive a process recommendation with estimated cost and lead time.