 French
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 Italian
 Portuguese

Design for CNC machining means shaping a part so a Machine à commande numérique can cut it quickly and accurately. The goal is to minimize tooling changes, cycle time, and post-machining rework. In practice, this covers wall thickness, hole depth-to-diameter ratios, fillet geometry, and tolerance allocation. A well-designed part can reduce cycle time by 15 to 30 percent in many cases. Getting these fundamentals right saves money and reduces schedule pressure on the shop floor. Start by asking one question: can this feature be cut in a single setup?
Most part failures on the shop floor trace back to a design that ignored basic CNC tool access limits. Engineers focus on function and fit. Then, during quote review, they find that a thin wall or deep blind hole forces expensive secondary operations. The result is a longer lead time, a higher quote, and sometimes a full redesign. The good news is that most of these problems are caught early, when the cost of a fix is measured in minutes of CAD editing rather than hours of rework.
Seven Core DFM Rules for CNC Parts
The following seven rules cover the features that most often trigger rework, extra setups, or rejected quotes.
1. Keep minimum wall thickness above 1.0 mm. Walls thinner than this flex during clamping and cause tool chatter. Depending on material, the practical minimum may be 1.2 mm for aluminum or 1.5 mm for steel.
2. Limit blind hole depth to four or six times the diameter. Deeper holes require longer end mills, which reduce rigidity and add cycle time. If the design demands more, specify a stepped hole or a through-hole instead.
3. Use internal fillets instead of sharp corners. A zero-radius internal corner creates a stress concentration and forces the tool into a tight-radius path. A minimum 0.5 mm fillet is easier to machine and stronger in service.
4. Avoid undercuts and internal corners that face the tool approach direction. These features require special fixtures or a secondary EDM operation. If the function allows, redesign the corner so the tool can reach it directly.

5. Allocate tight tolerances only where function requires them. A ±0.05 mm tolerance on a non-critical face adds machine time with no benefit. Reserve the tightest calls for mating surfaces and critical dimensions.
6. Standardize hole patterns and bolt-circle layouts. Irregular spacing forces the CNC program to write extra move commands and increases setup time. Symmetric patterns reduce fixture complexity and programming effort.
7. Specify material grade and condition directly on the drawing. Vague calls such as “stainless steel” leave the shop to guess between 303, 316, or 17-4. Naming the exact grade and temper avoids wrong-quote risk and rework.
Apply these rules during the CAD stage, not after the first quote comes back. Early DFM review is where the savings actually happen.
Design Mistakes That Add Cost
The table below pairs common geometry mistakes with their cost impact and a practical alternative.
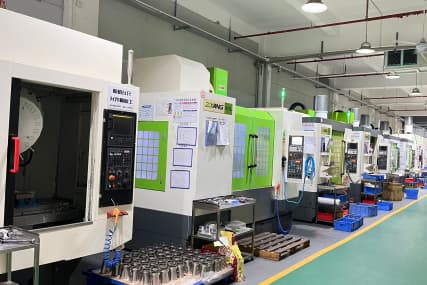
Most of these issues surface during a pre-production révision technique. Sending your drawing to a machining partner before releasing it to the shop can flag conflicts early, when fixes are still cheap. YPMFG includes this kind of review as part of its usinage CNC sur mesure service, catching geometry, tolerance, and material conflicts before tooling is committed.
Tolerance and Material Considerations
A standard Tolérance CNC for most machined parts is ±0.1 mm. Each step tighter adds machine time and inspection cost. Before specifying ±0.01 mm, verify with the assembly team that the functional requirement actually needs it.
Material choice affects machinability more than most designers expect. Aluminum 6061 machines at roughly 100 percent of a reference cutting speed, while 17-4 PH stainless can drop that to 25–35 percent. This directly changes cycle time and unit cost. CNC material selection should balance machinability, corrosion resistance, and the service environment. In many cases, the machinability gap between a mild steel and a precipitation-hardened alloy is the single largest cost driver in a part.
Hardened steels and titanium alloys often need a secondary process such as EDM for small internal features. If your design includes these materials, confirm with the shop that every feature is tool-reachable before releasing the drawing.
Practical Questions Before You Send a Design
How many machine setups does this part require?
Aim for one or two. Each additional setup adds fixturing, alignment, and programming time. If your part needs three or more, review whether a feature can be combined or the fixture redesigned.
Can any feature be eliminated or simplified without losing function?
Audit every pocket, chamfer,and surface-finish call. In many cases, a chamfer on a non-critical edge adds cost with no benefit. Stripping non-essential features is the fastest way to cut cycle time.
Are the specified tolerances actually required for assembly?
Check with your assembly team. A ±0.05 mm call on a non-mating face often exists by habit. Loosening it to ±0.1 mm can reduce machine time noticeably without affecting fit.
What exact material grade and condition is specified?
State the full grade, such as 6061-T6 or 316L solution-annealed. Vague descriptions like “stainless” or “aluminum” lead to quote ambiguity. Always include the condition or temper.
Making the Right DFM Decision
Getting design for CNC machining right is not about simplifying the part at the expense of function. It is about removing manufacturing friction so the part builds cleanly, fits in assembly, and holds up in service. The seven rules above, paired with a focused tolerance and material review, address most of the issues that drive up cost and lead time.
If you are working through a new part or reviewing an existing design, you can send your drawings to YPMFG for a pre-production review. The team checks tool access, tolerance feasibility, and material suitability, then returns a short report with flagged items and suggested changes before any tooling is committed.






