French
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 Italian
 Portuguese

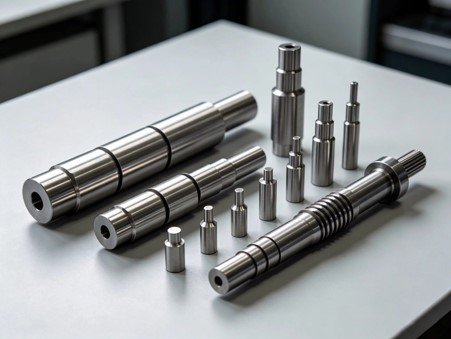
Last month a buyer sent me a drawing for a plain steel pin. Eleven tolerances on it. Eleven! Nine of them meant nothing, he’d just copied the title block from some other part. Guess what that did to his quote. I run into this all the time with Tournage CNC, so here’s the stuff I wish every buyer knew before hitting send.
What the Lathe Actually Does
Short version: the part spins, the tool doesn’t. A bar goes in the chuck, a tool on a turret nudges up against it and peels metal off, and a few seconds later you’ve got a diameter. The same machine swaps tools by itself, so it faces the end, turns the outside, drills, cuts a thread and snips the finished piece off the bar. Then a bar feeder pushes out more stock and it all starts again. Honestly, a good lathe will run half the night with the lights off in the shop.
Plenty of lathes have live tools now too. Those can drill a cross hole or mill a flat in the same grip. One less setup, one less chance to bump something.
What Belongs on One
Basically, anything round. If you can spin it like a top and it still looks the same, it’s a lathe part. Shafts, bushings, spacers, nozzles, valve bodies. I’ve seen pins smaller than a grain of rice and wheels as wide as a dinner plate. Length is where it gets awkward. Make a part too long and thin and it springs away from the tool, so the middle comes out fatter than the ends. Annoying, and no amount of programming fixes it.
Tolerances, and Why Fewer Is Better
Without a note, most shops fall back on ISO 2768 medium. ±0.01 mm on a key diameter is routine. ±0.005 mm? Possible on a few features, but the shop will want to talk it over, and they’ll check every piece. Fair enough.
As for roughness, a normal cut leaves about Ra 3.2 µm. A slower finishing pass gets you to 1.6, and with a light, sharp cut you can sometimes see 0.8. One thing I really like about turning is how well the diameters line up with each other. They’re all cut in one grip, so there isn’t much to go wrong.
Back to the pin with eleven tolerances. Every tight number means slower cuts, more measuring and more risk of scrap, and you pay for all of it. Put the tight one where a bearing or seal sits. Leave the rest loose.
Picking a Material
Aluminum 6061 is easy. 7075 is nearly as nice, and brass C360 practically cuts itself. In steel, 1018 and 1045 are cheap and tough. If the part gets heat treated later, I’d go with 4140.
Stainless is where people trip. 303 is the free-machining one, thanks to a bit of sulfur that snaps the chips. 304 is gummy. 316 work-hardens, so if the tool rubs instead of cutting, the metal just gets harder. Titanium is strong and light, but it dumps heat right on the cutting edge and chews through inserts.
Plastics are fun on a lathe. Delrin is my favourite, with nylon, PEEK and PTFE close behind. They do get warm and they do move, though. PTFE is so soft that a tight chuck squashes it, so shops switch to soft jaws.
Design Habits That Save Money
Inside corners come out round, since the tool tip is round. Draw a small fillet. Need a sharp shoulder for a mating part? Add a relief groove instead.
Keep metal walls over 0.8 mm and plastic over 1.5 mm. Thinner than that, they flex while being cut. Watch the length too. Past four or five times the diameter, you need a steady rest or a different machine, so mention it early.
Deep bores are hard on tools, and about four diameters deep is where I’d stop. Use standard threads. Name the pitch. Chamfer the edges, because a burr will find somebody’s thumb eventually.
Surface Finishing: Where Fits Go Wrong
What finish you need depends on the job the part does. As-machined is cheapest, with faint tool lines you can see. Bead blasting gives a flat matte look and hides them. Tumbling deburrs small parts by the bucket. Aluminum is usually anodized, steel gets black oxide or zinc, and stainless is passivated.
The mistake I see most with Finition des surfaces? Somebody anodizes a turned plug and it won’t fit its bore. Coatings have thickness. Roughly ten microns a side, which sounds like nothing until your fit is ±0.01 mm. Tell the shop which sizes must hold after coating, and they’ll cut a little over or under to make up for it. And mask any face that needs bare metal for grounding.
One Piece or Ten Thousand
One prototype means setup eats most of the price. Order a batch and cycle time starts to matter instead, which is where the bar feeder earns its keep. Repeat orders run the same program, so lot two matches lot one. Ask for a model review first. A decent shop will point out the stuff that’s driving your price up.
What to Send for a Quote
STEP file, PDF drawing. Material, quantity, finish. Say which tolerances matter and what the threads are. Need a material certificate or an inspection report? Ask now, not after the parts are cut.
Wrapping Up
CNC Turning is the right call for round parts, whether it’s one or ten thousand. Pick the material for the job. Tighten tolerances only where they count. Settle the finish before the drawing is final. Do that and the parts show up right, at a fair price.