Italian
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Portuguese

OEM custom metal stamping fabrication refers to the production of metal components through progressive die stamping, formed to your exact specifiche for integration into end products. Unlike standard off-the-shelf fasteners or sheet metal parts,stamped components are tooling-specific. Each part requires a dedicated die set, which drives upfront cost but enables high-volume consistency. If your application calls for thousands to millions of identical parts with tight tolerances, custom metal stamping is typically the most economical production method.
Most procurement teams face the same bottleneck: they know they need stamped parts but are unsure which spec sheets to prepare, which material grade to specify, or how to validate a supplier’s capability before committing to a tooling investment. Getting these decisions wrong means rework, delayed production lines, or parts that fail in assembly.
Key Specifications to Define Before Sourcing
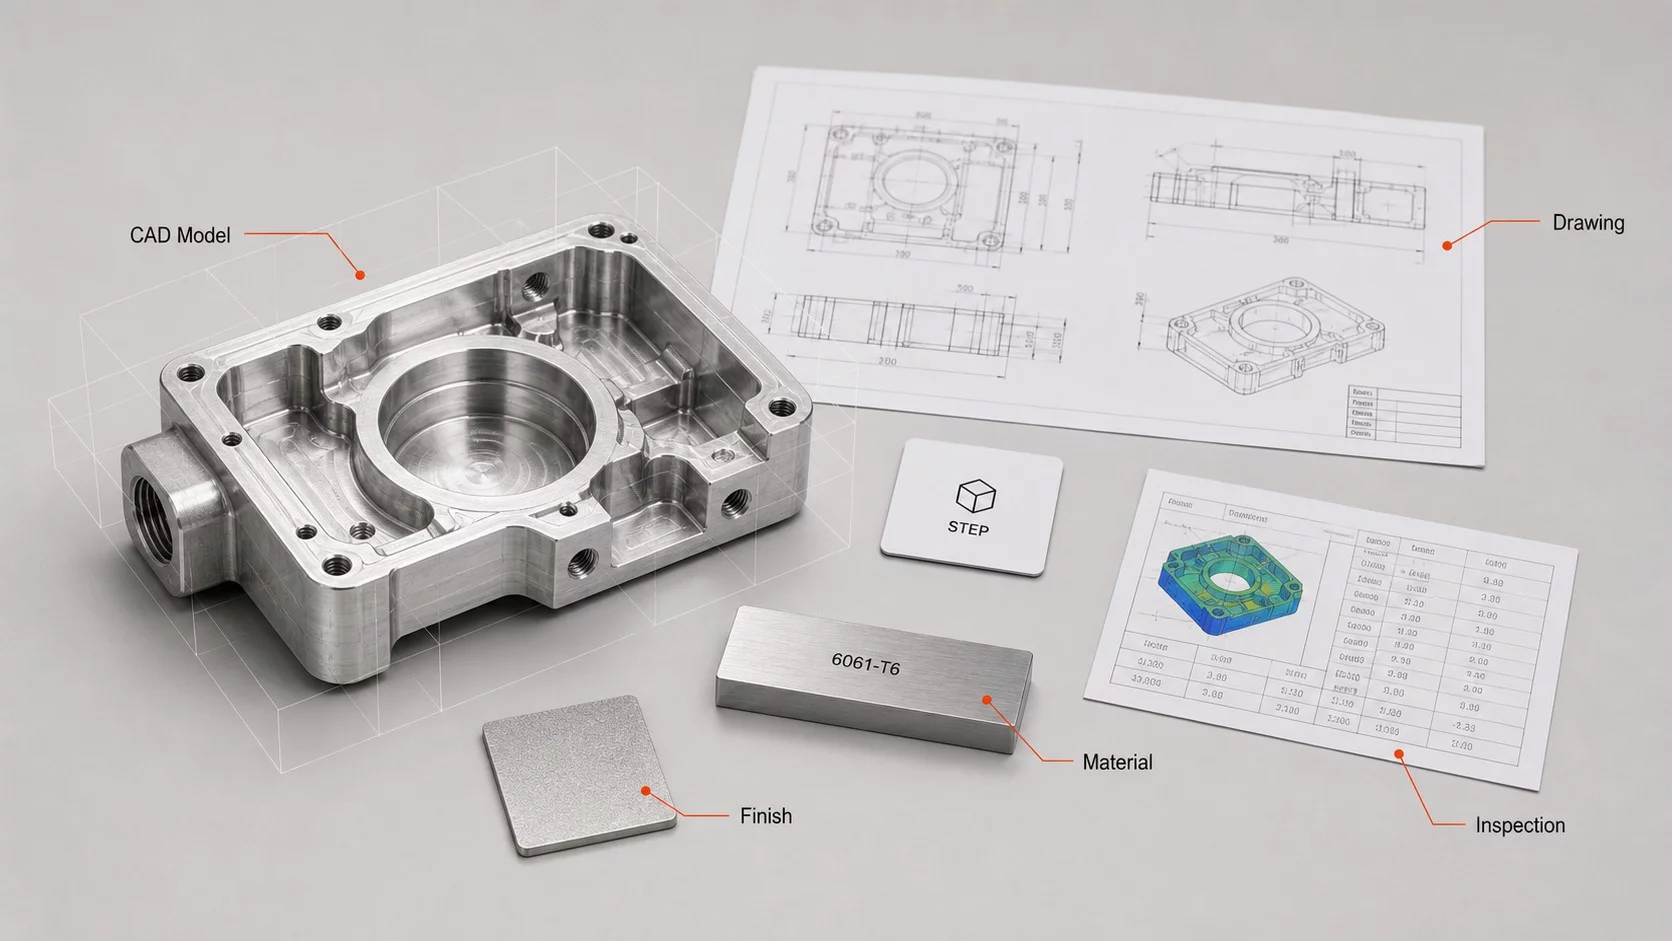
Before requesting a metal stamping fabrication quote, lock down five core parameters: material grade, thickness, part geometry, finishing requirements, and annual volume.
These five inputs determine die complexity, tonnage, and cycle time. A 0.8 mm cold-rolled steel part and a 2.4 mm stainless steel part will use entirely different tooling.
Tolerance is the next decision point. Stamping tolerances typically range from ±0.05 mm for general-use parts to ±0.02 mm for precision-fitted components. Tighter tolerances increase die cost and may reduce production speed. Specify tolerance only where functionally necessary to keep tooling affordable.
If your part feeds into a regulated industry such as automotive component manufacturing or medical device assembly, document the relevant material certifications and traceability requirements upfront. This avoids late-stage re-stamping or lot rejection at the customer’s incoming inspection.
## Materials, Tolerances & Tonnage: What Drives Your Cost
Costo unitario in OEM metal stamping is not a single number. It shifts with material, part complexity, run length, and finishing.
A part running 500,000 units per year shows a dramatically lower per-unit die allocation than the same part running 10,000 units. Metal stamping cost breakdown should always separate tooling from per-unit production so you can compare quotes on the same basis.
Quality Control & Compliance Checkpoints
Every stamped-part batch should carry traceability from strip certificate to final inspection.
Verify that your supplier provides material mill certificates, in-process dimensional checks at defined intervals, and a final inspection report per lot. For regulated applications, ask whether the die shop runs first-article inspection and maintains Cpk data on critical dimensions.
YPMFG offre supporto agli acquirenti che necessitano di valutazione tecnica of stamped-part drawings before tooling is committed. Sending your 2D or 3D geometry for a DFM review can surface formability issues, die-clearance risks, and fixture design gaps early in the project.

## Common Questions Before Ordering Metal Stamped Parts
What is the minimum order quantity for custom stamping?
There is no fixed industry minimum. Die cost can exceed material cost for small runs, so many shops quote a minimum of 5,000 to 10,000 units to keep per-unit pricing reasonable. Short runs are possible but carry higher amortized tooling cost.
How long does progressive die design and build take?
Depending on part complexity, die design typically runs 4 to 8 weeks and fabrication plus trial another 6 to 10 weeks. Simpler single-station dies compress this timeline. Complex progressive dies with multiple stations extend it.
Can I reuse the same die across part revisions?
Minor geometry changes—burr removal, small bend-angle adjustments—can often be accommodated with die rework. Major redesigns usually require a new die. Confirm revision flexibility during the quoting stage.
What finishing options pair well with stamped steel parts?
Common finishes include electroplating, powder coating for corrosion resistance, and passivation for stainless. The finish is selected based on application environment and target service life.
How do I verify a supplier’s stamping capability before awarding?
Request their metal stamping equipment list (press tonnage, stroke length, automation type), sample parts from comparable geometries, and production references from similar-volume jobs. A capable shop will share these documents without hesitation.
Choosing the Right Stamping Partner for Your Run
La destra OEM metal stamping fabrication partner is not the cheapest die shop. It is the one that validates your part for formability, holds tolerances across a multi-year production run, and responds when design revisions land mid-cycle.
Send your drawings, material specs, and target volume to YPMFG for a technical review. You will receive a DFM assessment, a tooling recommendation, and a structured quote broken into die, per-unit, and finishing line items—so you can compare options before committing.