Italian
 English
 German
 Russian
 Japanese
 Korean
 Spanish
 French
 Portuguese

Aluminum parts fabrication covers the full process of converting raw stock into functional components. It includes CNC machining, casting, extrusion, and sheet metal forming. The method you choose determines strength, tolerance, surface finish, and final cost. For most precision work, Parti in alluminio lavorate CNC are the default because they deliver tight tolerances without expensive tooling. The key decision is matching process to geometry, volume, and industry requirements.
Most buyers underestimate how much the fabrication method affects part cost and performance. The wrong choice adds weeks to lead time, pushes tolerances out of spec, or inflates the unit price. Here’s what to evaluate before you commit.
Why Aluminum Is the Default for Machined Parts
Aluminum’s low density and high strength-to-weight ratio make it the go-to material for aluminum parts fabrication in aerospace, automotive, and electronics. It machines at roughly one-third the power requirement of steel, cutting cycle time and energy cost.
The metal also dissipates heat well, which matters in housings and thermal management components. Corrosion resistance means many parts skip secondary coating steps entirely.
That said, aluminum’s yield strength is lower than steel or titanium. If your part sees sustained loads above ~300 MPa, you need a higher-grade alloy or a design rethink. Aluminum alloy selection directly governs stiffness and long-term behavior under load.
Choosing the Right Fabrication Process
The process you pick shapes cost, tolerance, and feasible production volume. The table below summarizes the main options:
For prototypes and low-volume production, CNC machining is the fastest path to a functional part. At higher volumes, die casting or extrusion can bring unit cost down sharply. The break-even point depends on part complexity and expected design revisions.
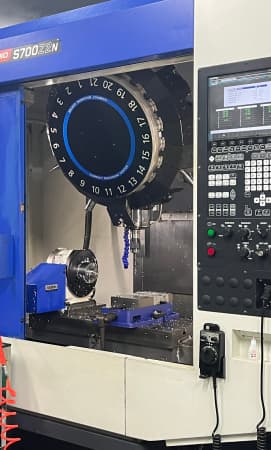
YPMFG supports projects across flexible volume ranges, from single prototypes to repeat production runs, using both in-house CNC machining and casting partnerships.
Fattori di costo e rischi nascosti
Unit price for aluminum parts fabrication isn’t just about material. The main cost drivers include:
Tolleranza e finitura: Tighter tolerances and finer surface finishes add machining or post-processing hours.
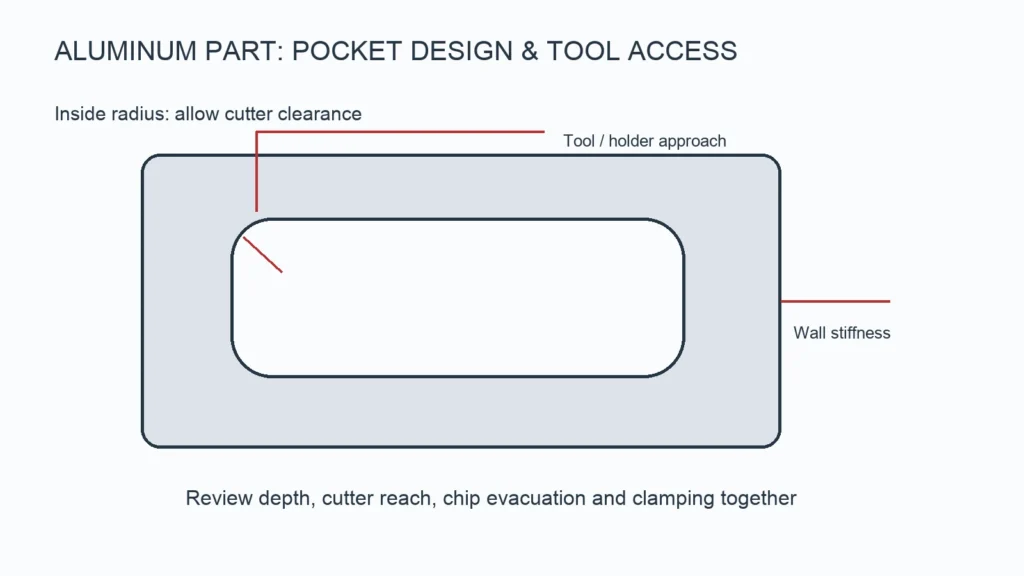
Geometria delle parti: Deep pockets, thin walls, and internal threads increase fixture complexity and cycle time.
Alloy grade and temper: 7075-T6 costs more per kilogram than 6061-T6 and changes post-machining behavior.
Volume and setup amortization: Low runs spread tooling and setup costs over fewer units.
Hidden risks include specifying a grade that’s hard to source, requesting multi-coat finishes, or calling tight tolerances on non-critical features. Aluminum part cost estimation should always reference the exact alloy, temper, and finish callout, not just the drawing.
Cosa verificare prima di effettuare un ordine
A short pre-order checklist keeps the project on track:

Confirm alloy grade and temper (e.g., 6061-T6 vs. 5052-H32).
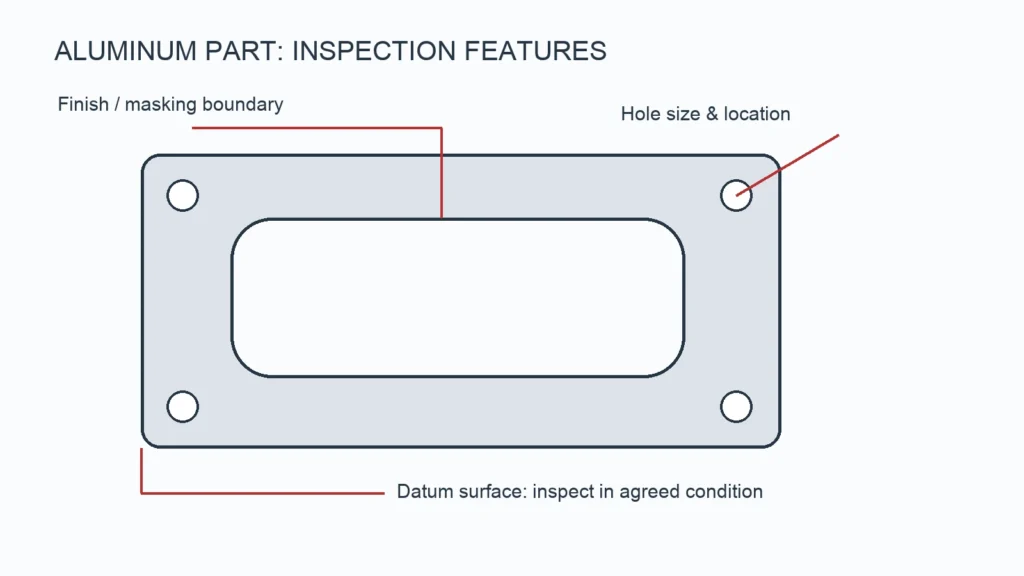
Verify which features carry critical tolerances.
Specify surface finish method: anodize, powder coat, or bare.
Richiesta certificati sui materiali and the full process flow.
Review the first-article inspection report before releasing the full run.
Confirm inspection methods: CMM, profile projector, or coordinate report.
YPMFG runs an engineering review on drawings before quoting, flagging DFM issues that could affect fabrication timelines or costs. Sending your specs early avoids rework cycles down the line.
Common Questions Before Ordering Aluminum Parts
What alloy should I use for a general-purpose machined part?
For most structural and mechanical applications, 6061-T6 is the default. It balances machinability, strength, and weldability. If the design needs higher yield strength, 7075-T6 is the common upgrade. Verify the load case before locking in the grade.
How tight can CNC-machined tolerances go on aluminum?
Standard CNC tolerances on aluminum are ±0.02 mm. Precision work can reach ±0.005 mm on select features. Tolerances tighter than that may require secondary operations like lapping or grinding. Factor that into your Tolleranza di lavorazione CNC budget early.
L'anodizzazione modifica le dimensioni del componente?
Yes. Type II anodize adds roughly 5–25 µm per surface; Type III adds 25–100 µm. If you have tight fit tolerances, the drawing must call out post-anodize dimensions. Specify whether tolerances apply pre- or post-finish.
What documents should I request from a fabrication supplier?
At minimum, ask for the process route, material traceability certs, and a first-article inspection report. Automotive or medical projects typically need a PPAP-style package. Aluminum parts documentation varies by industry, so confirm exact deliverables upfront.
Prendere una decisione migliore nel lungo periodo
Scegliere il giusto aluminum parts fabrication process comes down to matching material, geometry, volume, and tolerance to your actual application. A short engineering review surfaces issues that would otherwise cost weeks of rework.
If you have drawings or a BOM, send them to YPMFG for a no-obligation DFM check. You’ll get feedback on manufacturability, material fit, and a rough cost range before committing to a formal quote.