Japanese
 English
 German
 Russian
 Korean
 Spanish
 French
 Italian
 Portuguese

Plastic sheet fabrication converts flat polymer panels into functional components through cutting, bending, welding, forming, or post-processing. The right process depends on material type, part geometry, tolerance requirements, and production volume. Choose wrong and you face warped edges, inconsistent fits, or costly rework. This guide breaks down the core decisions a buyer should verify before placing an order.
Most fabrication projects fail not at the machine stage but at the specification stage—wrong material grade, missing tolerances, or unclear finish expectations. YPMFG supports projects where precise sheet work feeds into larger CNC-machined assemblies, so the spec stage is where most risk lives.
Core Processes in Plastic Sheet Fabrication
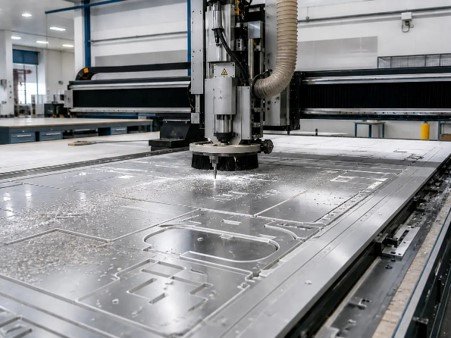
The main methods include レーザー切断, CNC routing, thermoforming, cold bending, welding (solvent or ultrasonic), and secondary sanding or polishing. Each suits different thicknesses and geometries. For example, laser cutting handles intricate 2D profiles in acrylic sheets または PVC panels, while thermoforming creates 3D shapes from the same sheet. Cold bending works well up to a material-specific deflection limit. If your part combines multiple features—cuts, bends, and surface finish—a hybrid approach is standard.
Material Selection and Compatibility
一般的なオプションには以下が含まれます ABS, polycarbonate, acrylic (PMMA), HDPE, and polyethylene. Each has distinct stiffness, heat resistance, and chemical tolerance. A buyer specifying only “plastic sheet” without naming the grade leaves the door open to substitutions that may not meet your load or environmental needs. Always confirm the material certification and test data sheet before approval. YPMFG can review your material spec against application requirements and flag compatibility risks early.
Tolerance, Finish, and Quality Verification
Typical laser-cut edge tolerances range from ±0.1 mm to ±0.5 mm depending on thickness and material. Thermoformed parts often carry ±0.5–1.0 mm dimensional variation. Before sign-off, request edge-roughness specs, weld-strength test results if applicable, and a first-article inspection report. A clear quality checklist in the purchase order prevents post-delivery disputes. For CNC-machined sub-assemblies that mate with formed plastic parts, CNC加工の公差 must be cross-referenced to avoid assembly gaps.
Cost Drivers in Sheet Fabrication
Unit cost shifts with material grade, sheet thickness, part complexity, tooling or fixture design, and batch size.
Thin,simple parts in commodity material run cheapest; thick, multi-feature parts in engineering-grade polymer push cost up sharply. Getting a fabrication cost estimate early helps budget realistically.
Common Specification Mistakes
Omitting bend radius or minimum wall thickness for thermoformed parts
Specifying “any plastic” instead of a named grade and thickness

Ignoring warpage allowance for sheets over 3 mm
Not defining acceptable surface finish (gloss, matte, texture)
Skipping UV-stabilized grade for outdoor exposure
Each of these leads to rework or rejected batches. A short 技術レビュー before production catches most of them.
購入者からよく寄せられる質問
What sheet thickness should I specify for laser cutting?
Thickness depends on material and cut-quality needs. For acrylic sheets, 2–6 mm is common for clean edges. Above 10 mm, kerf width and heat-affected zone grow, so confirm the cutter’s maximum capacity and edge-roughness spec with your fabricator before finalizing drawings.
Can plastic sheets be combined with CNC-machined metal parts?
Yes. Many assemblies pair thermoformed or cut plastic covers with CNC加工 brackets or housings. The key is matching tolerances at the interface so clips, screws, or welds align without forcing. Coordinate both the sheet work and the machined components under one project to avoid fit issues.
How do I check weld strength on plastic joints?
Request a peel or tensile test on a sample joint before full production. Ultrasonic welding そして solvent welding each have different strength profiles. Confirm the test standard and pass criteria in the quality agreement so both sides share the same acceptance bar.
What lead time should I expect for a small batch?
For 50–200 pieces of a single design, typical lead time runs 2–4 weeks including material sourcing and QC. Complex multi-step parts or custom fixtures can add 1–2 weeks. Lock the timeline in the order acknowledgment to protect your schedule.
より良い長期的な決断を下す
Getting plastic sheet fabrication right comes down to locking down material grade, process, tolerances, and finish before the first cut happens. Send your drawings, material spec, and quantity to YPMFG for an engineering review and a no-obligation quote. That single step often prevents the most expensive mistakes downstream.