Services de moulage sous pression sur mesure

From rapid prototypes to high-volume production runs, YP-MFG’s die casting services have you covered. We work with aluminum, zinc, and magnesium, and handle everything from tooling to finishing—plus, our experts make sure your die cast parts turn out just the way you need.

YPMFG - Services de moulage sous pression - Fabrication
20,000+ customers in over 120 countries & regions trust YP-MFG to manufacture their custom parts

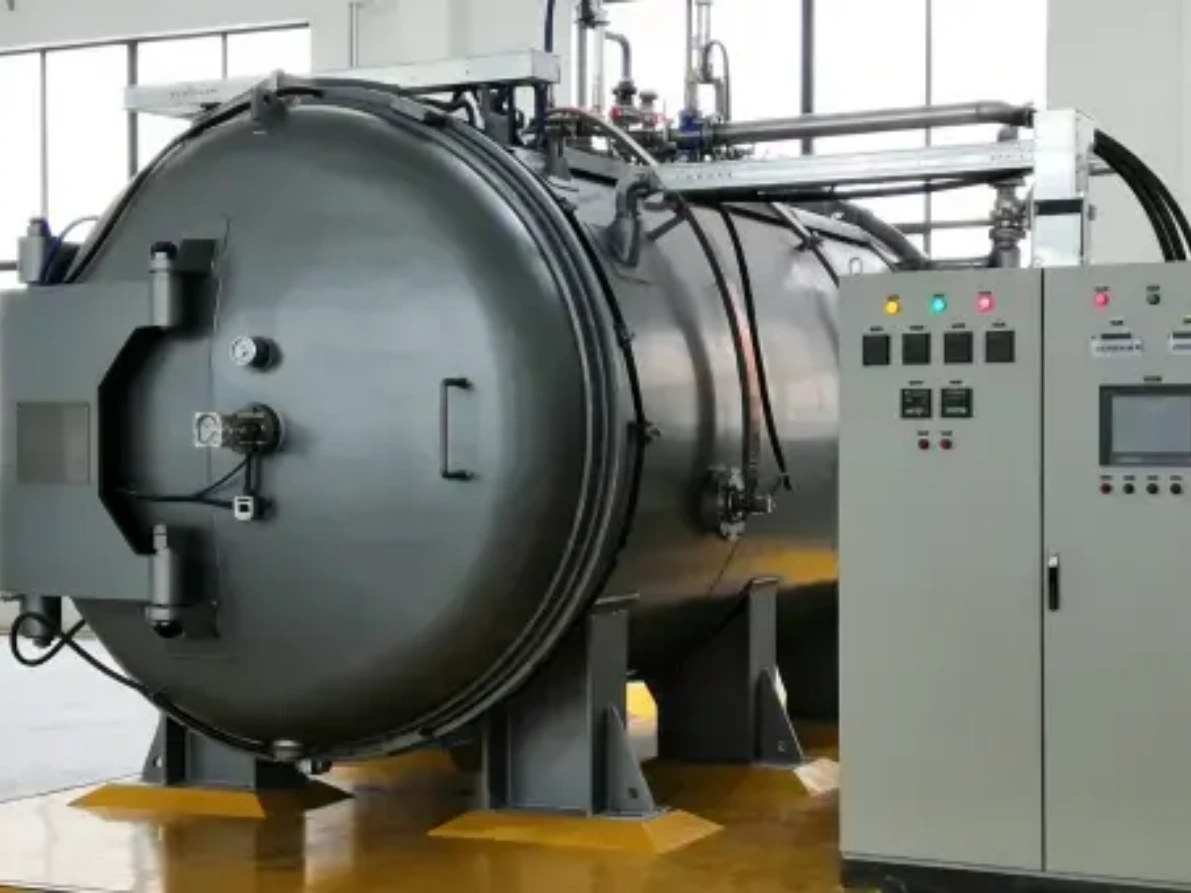
Usine et équipements de moulage sous pression YP-MFG

Our network of certified die casters runs 60+ machines, supporting intricate geometries and tight timelines.
Les services proposés comprennent la fabrication d'outils de moulage sous pression, l'usinage et toute une gamme de finitions.

Die Casting Manufacturer with Advanced Production Facilities

YP-MFG is a certified die casting manufacturer equipped with 60+ advanced die casting machines, serving global customers across automotive, industrial, robotics, and electronics industries.

Our factory in Shenzhen, China, integrates die casting tooling, high pressure die casting production, CNC machining, and finishing under one coordinated system—ensuring consistent quality and fast turnaround.

60+
Machines de moulage sous pression
ISO
9001, 16949, 13485
0,001 mm
Tolérance serrée
10 jours
Délais de livraison rapides

Capacités de moulage sous pression de YP-MFG

Détails
Tolérance Détails High-precision die casted parts need secondary machining to meet tolerance requirements, achieving accuracy up to ±0.01mm
Minimum Wall Thickness Détails Aluminum alloy recommended 1.5mm, zinc alloy can go down to 0.8mm
Rapport d'épaisseur de paroi Détails Keep within 1:3 ratio to avoid uneven filling
Diamètre du trou Détails Due to high temperatures during aluminum die casting mold processing, round holes smaller than 3mm diameter require secondary drilling. Product threaded holes and external threads are formed through secondary machining.
Angle de projection Détails Minimum 0.5° to avoid demolding difficulties
Maximum Die Life (Number of Cycles) Détails Zinc: 1,000,000 Magnesium, Aluminum: 100,000
Quantités minimales de commande (MOQ) Détails 500 à 1 000 pièces
Délai Détails 20-25 days. Specific timing varies based on mold type and product structure complexity

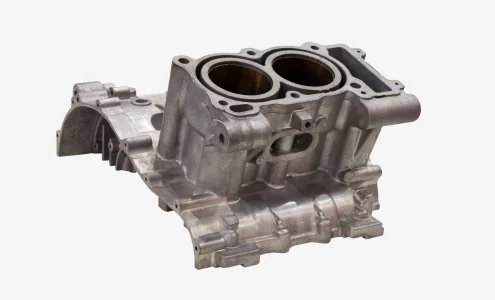
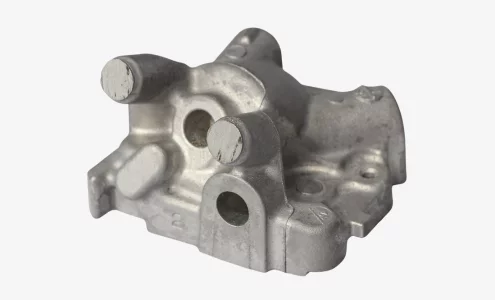
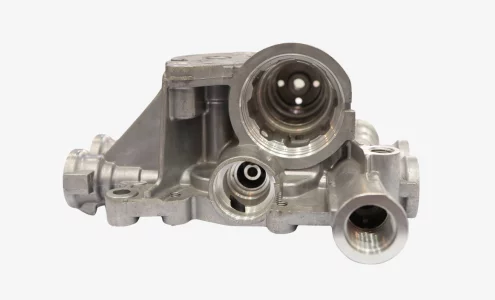
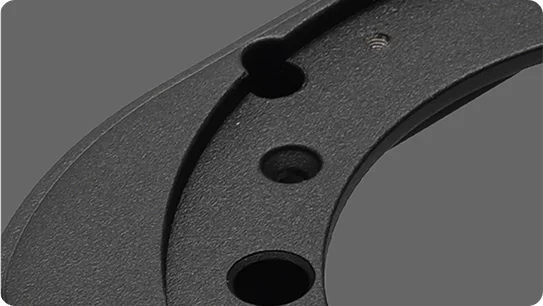
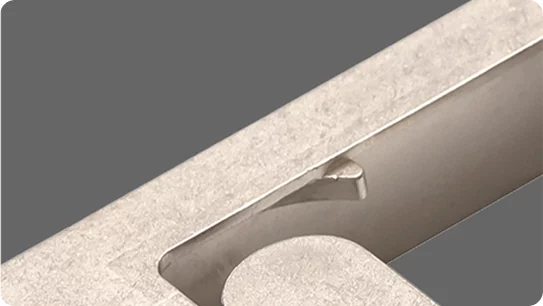
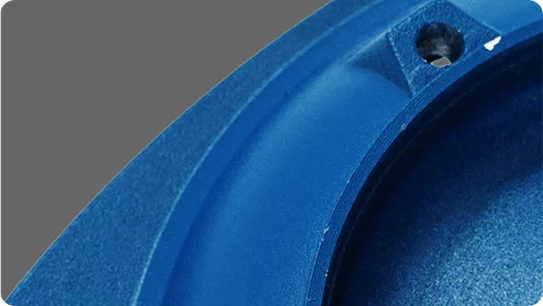
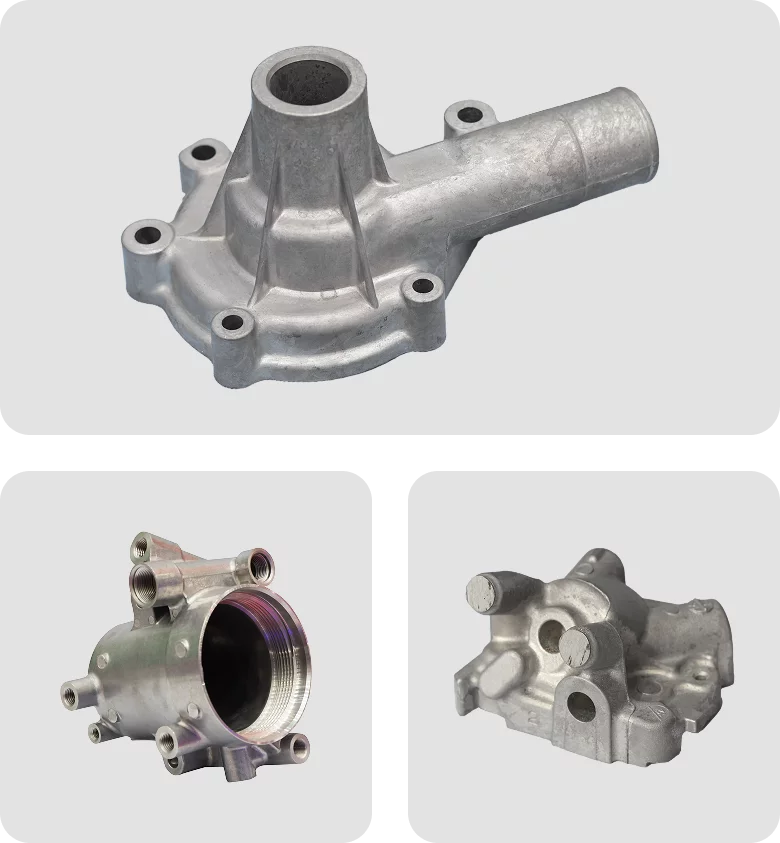
Pièces moulées sous pression que nous avons fabriquées

Types of Die Casting Processes at YP-MFG

To support a wide range of project needs, YP-MFG provides three types of die casting services, suited for different materials and deisgn complexities. We primarily apply hot and cold chamber casting. For components with tight tolerances and strong structural requirements, we offer advanced processes like semi-solid casting.

Moulage sous pression en chambre froide

Cold chamber die casting melts metal in a separate furnace before casting. The molten metal is poured into a cold chamber, where a piston pushes it into the die under high pressure. The process handles high melting point metals like aluminum. The separation prevents contamination and extends die life. This type of die casting produces car engine parts, aircraft components, and electronic housings where strength and precision matter

Moulage sous pression à chambre chaude

Hot chamber, or gooseneck casting, connects the melting furnace directly to the casting machine. A piston pulls molten metal from the furnace and injects it straight into the die. This creates faster cycle times and reduces waste since the metal stays hot throughout the process. The process suits low melting point metals like zinc, magnesium alloys. The direct connection allows efficient high-volume production of toys, hardware, decorative items, and small mechanical parts.

Moulage sous pression de matériaux semi-solides

Semi-solid die casting uses metal in a paste-like state between liquid and solid. The metal is heated to this semi-solid condition, then slowly pushed into the mold with less turbulence than liquid metal. This process reduces porosity and creates stronger parts with better surface finish. Semi-solid casting applies to aluminum and magnesium alloys effectively. The controlled flow produces automotive parts, aerospace components, and applications that need high strength and quality.

Matériaux et finitions pour le moulage sous pression

Die cast tooling uses hardened steel for withstand high temperatures and pressure. For die castings, non-ferrous metals are preferred for their fluidity and low melting points. Ferrous metals are used in some cases but less commonly. Below are standard materials used by YP-MFG in die casting manufacturing and we can support custom requests.

Acier à outils trempé

moule en acier moulé sous pression

Steel H13

Strong at high heat. Tough and crack-resistant. Stays hard when hot. Good for aluminum and magnesium casting.

moule en acier moulé sous pression

Steel 8407

Handles heat changes well. Tougher than H13 steel. Conducts heat better and lasts longer. Good for heavy-duty casting work.

moule en acier moulé sous pression

Steel 2344

Strong at high heat. Resists cracking from heat cycles. Easy to machine and polish. European steel grade for detailed parts.

Alliages pour moulage sous pression

moulage sous pression d'aluminium

Service de moulage sous pression d'aluminium

As a leading aluminum die casting company, we use ADC12, A380, and more for high-performance aluminum casting parts.

  • ADC10
  • A380
  • ADC12
  • Aluminium pur
  • DM6
  • HA6
  • HA4
  • 6063
moulage sous pression de magnésium

Moulage sous pression de magnésium

High strength, good machinability, and EMI shielding. Often used in electronics, automotive components, and handheld device housings.

  • AZ91D
  • AM60B
  • AM50A
moulage sous pression de zinc

Zinc Die Casting Services

Flows well in molds and holds tight tolerances. A good choice for small, detailed parts. Often used in electronics, connectors, locks, and everyday hardware for its strength and low cost.

  • ZAMAK2
  • ZAMAK3
  • ZAMAK5

Note: Choosing the right die casting material depends on your part’s application, geometry, operating environment, and budget. Talk to our experts for material recommendations.

Die-cast components, especially zinc and aluminum parts, naturally have smooth surface. To improve aesthetics, durability, or corrosion resistance, explore the surface finishes YP-MFG offers. For special request, feel free to contact us.

distribution originale

Distribution

Provides a basic, functional finish for die casting products with relatively smooth surfaces and minor tool marks, suitable for non-cosmetic applications.

anodisation

Anodisation

Improves corrosion and wear resistance of aluminum cast parts, while allowing for color options that enhance both durability and appearance.

chromate

Chromate Passivation

Commonly used for aluminum and zinc die casted parts, chromate passivation improves corrosion resistance and prepares the surface for painting or other coatings.

peinture

Peinture

Adds color and improves appearance while offering additional protection against corrosion and wear. Often used for branding or to meet specific design requirements.

moulage au sable

Sablage

Abrasive blasting that removes surface impurities and gives a uniform, matte texture. It also improves paint or coating adhesion.

Pièces moulées sous pression courantes
et applications industrielles

die casting are widely used to manufacture structural and functional metal components that require dimensional stability, strength, and repeatability.

Precision housings and device enclosures requiring dimensional stability and clean surface finish.

Engine housings, transmission cases, motor brackets, and structural supports requiring high strength and thermal resistance.

Precision brackets, gearbox housings, actuator components, and load-bearing structural parts.

Aluminum enclosures, LED heat sinks, internal frames, and protective housings for compact electronic devices.

Assurance qualité

At YP-MFG, quality drives every step—from the tools we use to the standards we uphold. Our ISO 9001, ISO 14001, and IATF 16949 certifications guarantee consistent excellence.
Contrôle et essais
certificats ISO

Équipements d'inspection de pointe

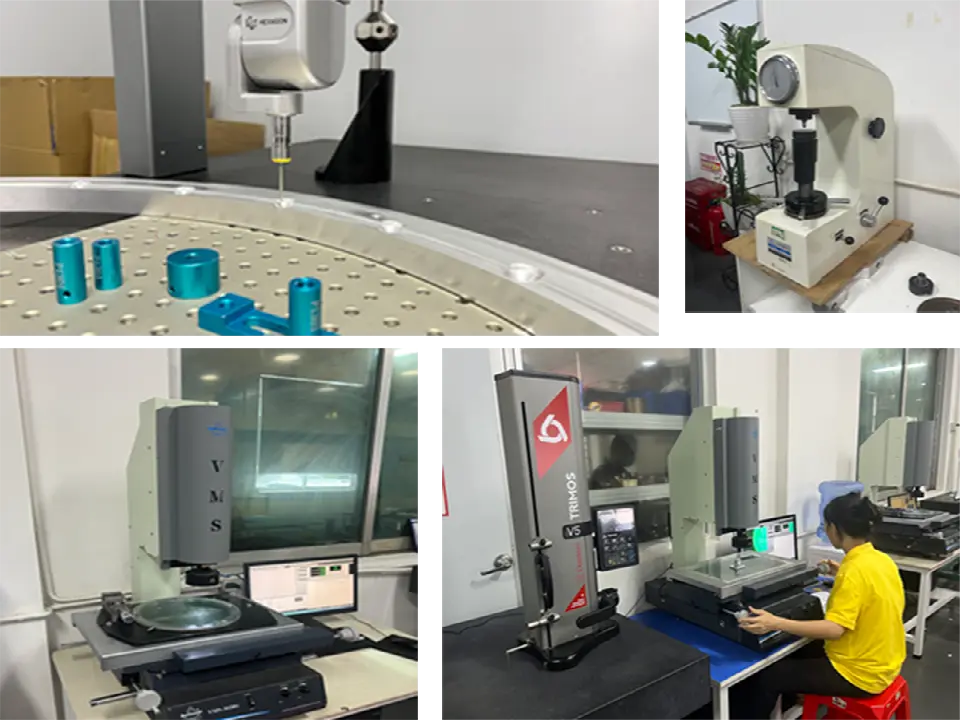
We use professional testing equipment for precise measurement and verification. Spectrometers analyze metal composition, coordinate measuring machines inspect complex 3D shapes, 2.5D instruments verify detailed features, and height gauges handle basic dimensions.

Comprehensive Testing Procedures

Parts go through four main tests: material analysis, durability testing, corrosion testing, and functional testing. These check your parts meet composition specs, handle tough conditions, resist environmental damage, and seal properly when needed.

Des normes de qualité éprouvées

Over 90% of parts pass first article inspection. And if there’s ever a quality issue, we’ll remake it for free. Every part gets checked before it leaves our facility.

Ready to see our quality standards in action? Get your quote today and experience the difference.

Why Choose YP-MFG Die Casting Services

rentable

Solutions rentables

We reduce your die casting costs through expert mold design and free DFM analysis, ensuring the most efficient material usage.

délais de livraison courts

Délais de livraison rapides

 Leveraging our in-house facilities and certified factory network, we deliver die casting samples in as little as 1 day with real-time project tracking.

qualité

Assurance qualité

ISO 9001:2015 certified. Strict quality checks at every step. We inspect parts pre-production, in-production, first article inspection, and pre-delivery.. Tight tolerances down to ±0.01mm.

Ready to Start Your Die Casting Project?

Upload your CAD files for free quotes and DFM analysis. We create prototype samples for approval, then begin full production. Your precision finished die cast parts ship on schedule.

Qu'est-ce que le moulage sous pression ?

Die casting is a high-precision metal casting process where molten metal is injected into a mold cavity under high pressure. It’s widely used to create complex metal parts with tight dimensinal accuracy and smooth surfaces, especially in high-volume production.

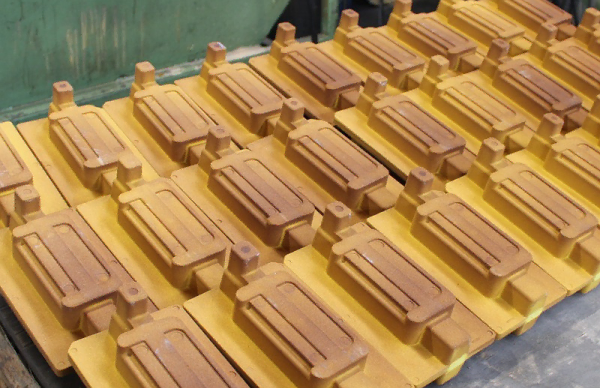
The die casting process uses a hardened steel dies cut by CNC machines. Molds can be single or multi-cavity, depending on production needs. Non-ferrous metals then get melted in furnaces, and machines push them into a ladle.

Based on what metal you’re using, die casting manufacturers choose hot chamfer or cold chamfer machines. Semi-solid casting works better for complex stuff like transmission cases, engine mounts, and electronic housings.

Once cooled, die cast parts are ejected and may need light post-machining, though smooth surfaces often reduce the need for additional finishing.

Applications du moulage sous pression

Die casting shows up in more industries than you might expect—and for good reason. It’s precise, repeatable, and ideal for making strong, detailed parts at scale. At YP-MFG, we help brands across industries turn complex designs into production-ready components—fast. Here are some key applications:

| Automobile

Durable, dimensionally stable parts like housings and bracket. For safety-critical, high-heat environments.

| Consumer Electronics

Internal frames, enclosures, and connectors, balancing structural integrity with compact, sleek design in high-use devices.

| Éclairage

Complex, lightweight housings with precision, ideal for both functional components and visible design elements.

| Dispositifs médicaux

Supports production of precise, clean-finished parts for tools and housings where consistency and hygiene are non-negotiable.

| Industrial Machinery

Withstands mechanical stress and wear, for structural and operational components in demanding, high-load applications.

pièces moulées sous pression

Avantages et inconvénients du moulage sous pression

Avantages

Production à grande vitesse. Cycle rapide pour de grandes quantités

Excellente finition de surface. Des pièces lisses dès leur sortie du moule

Tolérances serrées. Dimensions de précision allant jusqu'à ±0,01 mm

Formes complexes. Permet de créer des géométries complexes en une seule étape

Rentable à grande échelle. Coût unitaire réduit pour les volumes élevés

Inconvénients

Coût initial élevé. Coûts d'outillage et de mise en place élevés

Matériaux compatibles limités. Ne fonctionne qu'avec certains alliages.

Restrictions de taille. Limites de poids et de taille des pièces

Problèmes de porosité. Les bulles d'air peuvent affaiblir les pièces

Contraintes de conception. Exigences relatives à l'épaisseur des parois et à l'angle de dépouille

Foire aux questions

There is no “one-size-fits-all” price in die casting because costs depend on four key drivers: tooling (the mold), material volume, part complexity, and production quantity.
Volume de production : The higher your volume, the lower the per-part cost, as tooling expenses are amortized over more units.
Complexité : Features like undercuts, tight tolerances, or thin walls add to design and tooling complexity.

Tip: To get a precise quote, upload your CAD files today. Our engineers will perform a free DFM (Design for Manufacturing) analysis to help you identify cost-saving design optimizations before you spend a dime on tooling.

  • Production à grande vitesse : Perfect for scaling from hundreds to thousands of parts.

  • Finition de surface exceptionnelle : Get smooth, retail-ready parts straight from the mold.

  • Tolérances serrées : Consistency guaranteed up to ±0,01 mm.

  • Géométries complexes : Achieve intricate designs in a single production step.

Comment YP-MFG réduit-elle au minimum porosité dans les pièces moulées sous pression ?

When designing parts for die casting, several key considerations must be addressed to ensure optimal performance and manufacturability:

  • Wall Thickness: Maintain uniform wall thickness to promote even cooling and solidification, reducing risks of defects like warping or internal stresses. Thin walls are preferred for faster cooling and material savings, but their feasibility depends on the metal used and part complexity.
  • Draft Angles: Include draft angles in the design to facilitate the easy removal of the casting from the die. Typically, a minimum draft angle of 1 to 2 degrees is necessary, depending on the depth of the part.
  • Fillet and Radii: Incorporate fillets and radii to eliminate sharp corners and edges, which can cause stress concentrations and crack initiation points. This adjustment also enhances the flow of molten metal within the die.
  • Gating System: Design an efficient gating system to ensure proper flow of the molten metal into the die, minimizing turbulence and air entrapment. The placement of gates influences material distribution and part quality.
  • Venting: Proper venting must be planned to allow air and gases to escape from the mold cavity during metal injection. This helps prevent porosity and incomplete filling.
  • Simplifying Geometry: Simplify the geometry as much as possible to avoid undercuts and complex features that require intricate die mechanisms, which can increase tooling costs and complicate the casting process.

Yes, post-machining of die cast parts is not only possible but often necessary to achieve the desired precision and surface finishes that die casting alone might not provide. Post-machining allows for the attainment of tighter tolerances and smoother surfaces, which are crucial for high-performance and aesthetic requirements. Common post-machining processes include drilling, milling, and CNC machining, which refine the features of the die cast part to exact specifications.

Additionally, post-machining can correct any minor defects that occur during the casting process, such as porosity or surface imperfections. It also enables the addition of complex features and fine details that cannot be achieved through casting alone. By integrating die casting with post-machining, manufacturers can leverage the speed and cost-efficiency of die casting for the rough shape, while achieving the precision of CNC machining for critical dimensions and finishes.

The die casting process is a high-pressure manufacturing method where molten non-ferrous metal is injected into a precision-engineered steel mold (die). At YP-MFG, we follow a rigorous 5-step process to ensure every part meets your exact specifications:
  1. Preparation & Clamping: We start by lubricating the die cavities to ensure easy part ejection and temperature control. The two halves of the mold are then securely clamped under high pressure.

  2. Injection: Molten metal (aluminum, zinc, or magnesium) is forced into the die at high speed and pressure (typically between 1,500 and 25,000 psi). This ensures the metal fills even the most intricate geometries.

  3. Cooling & Solidification: The metal quickly solidifies inside the mold. Our advanced cooling systems ensure uniform temperature distribution to minimize internal stresses and warping.

  4. Ejection: Once cooled, the die opens, and the “shot” (the part plus the excess material like gates and runners) is ejected via hydraulic pins.

  5. Trimming & Finishing: The excess material is trimmed away. Depending on your needs, we then perform secondary CNC machining or surface finishing (such as powder coating or anodizing) to complete the part.

Ready to Start Your Die Casting Project?